
Carbide Insert Retention: Brazing vs Mechanical Fixing
Carbide insert retention compared: brazed and mechanically fixed inserts on service life, serviceability, fitment and cost per metre of cutting edge.

Insert loss is rarely a material problem. When carbide leaves a blade before its wear life is finished, the question is how the insert was held: a brazed joint that was not controlled, or a mechanical fixing that came loose under vibration. The two retention methods fail differently, are serviced differently, and are specified differently, which is why the choice belongs in the blade specification rather than in the workshop.
What Brazing and Mechanical Fixing Are Each Designed For
Brazing is permanent; mechanical fixing is replaceable.
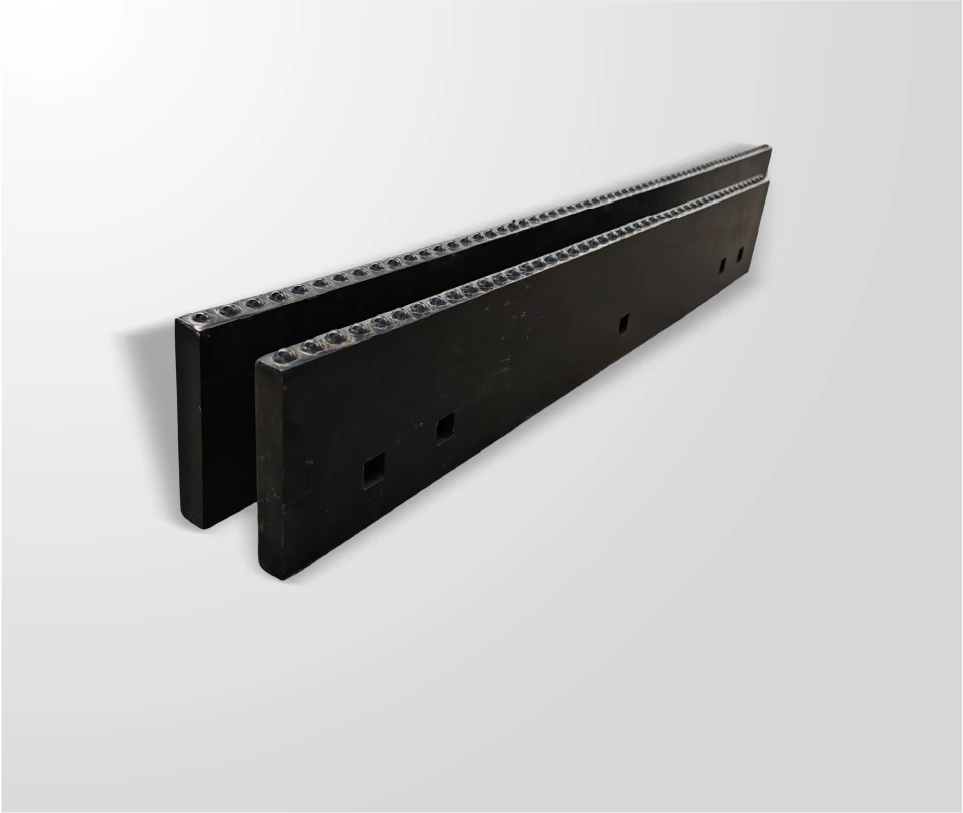
A brazed insert is joined to the steel body with a filler metal that melts below the parent metal; a mechanically fixed insert is held by bolts, pins, clamps or a keyed pocket.
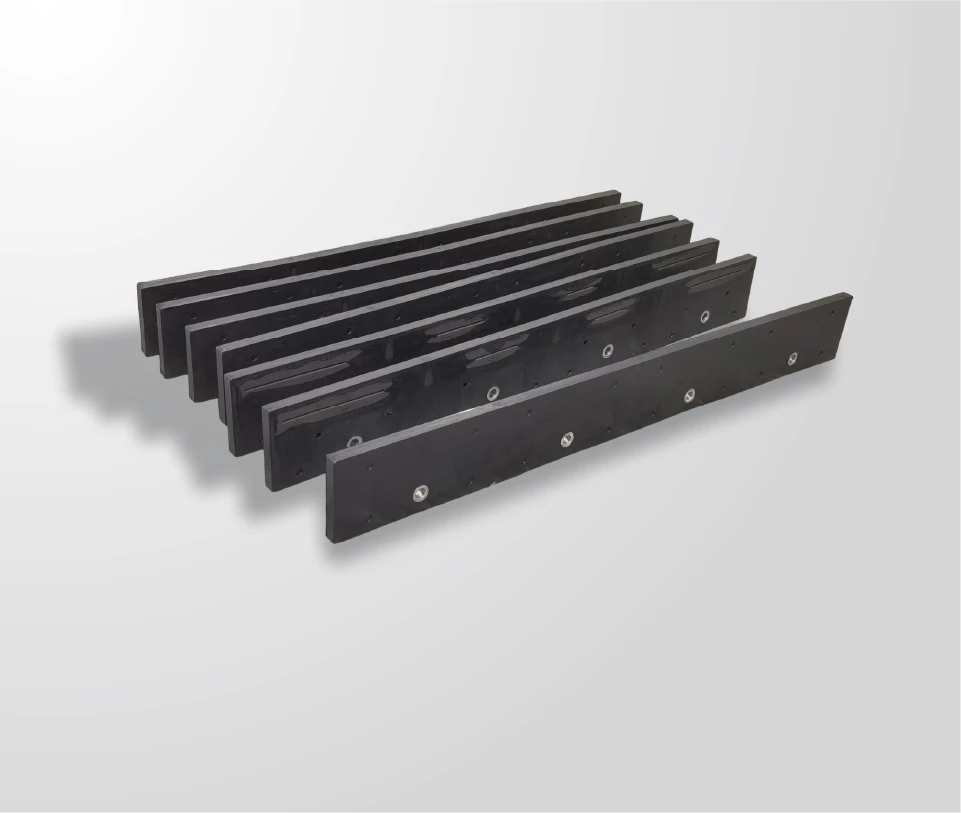
The design intent differs. Brazing is chosen where the insert and the blade are treated as one assembly, where a continuous joint distributes load across the whole insert base, and where the blade is exchanged as a unit at the end of its interval. Mechanical fixing is chosen where individual inserts are expected to be replaced in the field or in a workshop, where the fleet wants to keep the blade body in service across several insert sets, and where access for inspection matters.
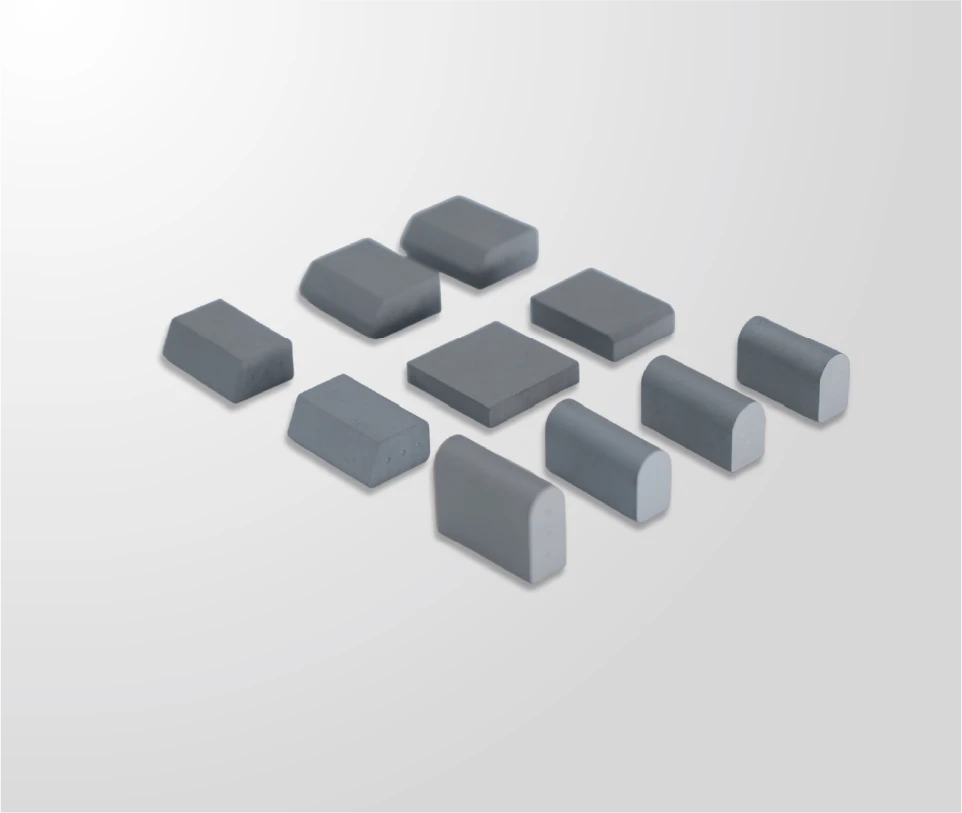
The retention decision also sets the failure mode a fleet should be inspecting for. A brazed joint fails progressively: voids, incomplete fill or contamination show up first as inserts loosening at the ends of the blade or in high-load positions. A mechanical fixing fails by loosening or by losing preload, which shows up as movement in the pocket before the insert leaves. Both are detectable, and both are ignored at the same cost. The wider set of insert retention designs covers the options beyond these two.
How the Two Retention Methods Differ in Service Life
A sound braze holds to wear-out; fixings can loosen first.
A properly brazed insert normally retires because the carbide has worn out, not because the joint failed. A mechanically fixed insert adds a second failure path: loose hardware, worn pockets and lost preload.
Service life therefore depends less on the method than on control of the method. On the brazed side, joint cleanliness, filler metal selection, heat control and cooling rate determine whether the bond is continuous across the insert base. Automated high-temperature induction brazing gives repeatable heat input at each position, which is why SENTHAI uses that process in Rayong, Thailand, rather than relying on manual torch work for production volumes. The joint itself is described in technical terms by TWI, and the process in production terms on the brazing for plow edges page.
On the mechanical side, service life depends on preload retention. Vibration, thermal cycling and surface wear in the pocket all reduce preload over time, which is why torque specifications and re-checks belong in the maintenance schedule rather than in the fitting instructions alone. A mechanically fixed insert that is inspected on the same interval as a brazed one, and re-torqued where required, will generally reach its wear limit rather than falling out.
Surface and Condition Differences Between the Two Methods
Impact and abrasive conditions separate the two methods more clearly than average wear. A continuous brazed joint distributes a shock load across the whole insert base, which reduces the stress concentration that a fixing point creates. On routes with rail crossings, broken pavement and manhole edges, that load distribution is the reason brazed assemblies survive impact that would loosen a bolted insert.
Abrasion affects both methods equally until the insert wears through, at which point the retention method determines what happens next. A brazed insert that wears through leaves the joint in contact with the road surface, where continued running can damage the blade body. A mechanically fixed insert that wears through loses its clamping height and may begin to move, which is usually detected earlier because the movement is visible in the pocket.
Chemical exposure belongs in the comparison too. Where a programme depends heavily on de-icing salts and abrasives, the resulting slurry accelerates corrosion in pockets and around fasteners, which affects mechanical fixings more than continuous brazed joints. The regulatory context for material use that many agencies now plan against is set out in the EPA’s municipal stormwater guidance.
Serviceability and Downtime Trade-Offs
The strongest argument for mechanical fixing is serviceability. A single damaged insert can be replaced without removing the blade, which suits fleets that maintain equipment in-house and want the shortest possible interruption. The strongest argument for brazing is that there is no hardware to check, no preload to maintain and no pocket to wear, which suits fleets that prefer to exchange complete assemblies and keep workshop variation out of the process.
Downtime arithmetic usually decides the question. If replacements are frequent and a workshop is available on site, individual replacement wins. If the blade has to be removed anyway, or if the work would fall inside a storm cycle, exchange of a complete assembly is the lower-risk option, because the workshop time is planned rather than reactive. The difference is not in the parts cost but in when the labour happens.
Inspection effort differs as well. A brazed joint is checked by looking for movement, incomplete fill and discolouration along the bond line, which is quick but requires the inspector to know what a sound joint looks like. A mechanical fixing is checked with a torque wrench and a visual check of pocket condition, which is slower per insert but more objective. Fleets should choose the method whose inspection they will actually perform on schedule.
Fitment and Equipment Compatibility for Brazed and Mechanically Fixed Inserts
Both methods fit the same mounting patterns; what changes is the interface inside the blade. SENTHAI works to plus or minus 0.02 mm dimensional tolerances on carbide components and validates fitment against AASHTO and DIN bolt patterns before release, with AASHTO published standards as the reference for agency specifications and DIN covering European and export conventions.
Retrofit is where compatibility has to be checked carefully. A blade designed around brazed inserts does not automatically accept a mechanical replacement, because the pocket depth, base support and clamping surface were not part of the original design. Where a fleet is considering a change of retention method on existing blades, the practical questions are whether the blade body can carry the clamping load, whether the pocket can be brought to the required tolerance, and whether the resulting assembly keeps the same overall profile.
Health and safety requirements for the workshop apply to both methods and should be written into the fitting procedure rather than assumed. General industry requirements for hand and power tool use and for workshop ventilation are set out in the OSHA occupational safety and health standards, and welding and brazing operations add their own ventilation and fire precautions described by the American Welding Society.
Cost Per Metre of Edge Compared Across Brazed and Mechanically Fixed Inserts
Cost per metre is the fair comparison because it captures labour and downtime alongside the parts. The model structure is set out on the cost per mile page; between retention methods the inputs move as follows.
| Input | Brazed insert | Mechanically fixed insert |
|---|---|---|
| Assembly price | Includes the joining process and inspection | Includes pocket preparation and the fixing hardware |
| Replacement unit | Usually the blade assembly | Individual inserts |
| Labour pattern | Concentrated at planned exchange | Spread across individual replacements |
| Hardware and consumables | Consumed in production, not in service | Fasteners and pocket components recur in service |
| Inspection | Visual check of the joint line | Torque check and pocket inspection per insert |
| Failure consequence | Blade body can be exposed if an insert wears through | Loosening detectable in the pocket before loss |
Two cautions belong with that table. Individual insert replacement looks cheaper per event but repeats the labour more often, and the repeat cost lands when the fleet is busiest. Exchange of a complete assembly looks more expensive per event but concentrates the labour into a planned window. The second caution is that a brazed assembly with an uncontrolled joint is not cheaper in any scenario: it converts a wear item into a premature blade replacement.

Carbide Insert Retention: Where the Choice Is Genuinely Operational
The decision resolves along two axes: how the fleet services equipment and what its routes punish. Where maintenance capacity sits on site and routes contain embedded debris that damages individual inserts, mechanical fixing keeps the fleet running by replacing parts rather than assemblies. Where the fleet exchanges complete units and routes load the edge continuously, brazing removes the hardware variables entirely and keeps inspection to a single visual check.
What matters beyond the choice is consistency. A fleet that runs both methods should keep their inspection intervals and their performance records separate, because a wear reading from a brazed assembly and one from a mechanically fixed assembly are not directly comparable. Keeping the two records apart is what makes the next season’s decision evidence-based rather than a repeat of the previous argument.
Brazing and mechanical fixing are two ways to hold the same insert, with different failure modes, inspection routines and labour patterns. Brazing gains its advantage from a controlled, continuous joint and loses it entirely if joint quality is not inspected. Mechanical fixing gains its advantage from serviceability and gives some of it back in hardware and pocket maintenance.
The specification should therefore name the retention method, the process control behind it, the inspection routine that goes with it, and the exchange unit the fleet will actually use. Those four points turn a comparison of methods into an operating decision.
Send SENTHAI the blade pattern, route conditions and how your workshop handles replacements, and the team will review the retention method, process control and inspection routine that fit your operation.
Frequently Asked Questions
How can a fleet tell whether a brazed joint is sound?
Look for movement, gaps and irregular discolouration along the bond line, and check inserts at the ends of the blade and in the most heavily loaded positions first. A sound joint shows a continuous, even bond along the insert base. Records matter as much as the visual check: noting where insert loss occurs, and on which truck, turns a single inspection into a pattern the supplier can act on.
Can mechanically fixed inserts be retrofitted to a brazed blade?
Sometimes, but it is a design question rather than a parts swap. The blade body must be able to carry the clamping load, the pocket must be brought to the required depth and tolerance, and the assembly must end up with the same overall profile. Without those checks the retrofit can reduce retention rather than improve it. Ask the supplier to confirm compatibility against the actual blade drawing before ordering.
What joint clearance is acceptable for brazing?
Brazing relies on capillary action drawing filler metal through the joint, so the gap has to be small enough for that to happen and consistent across the joint area. Clearance that is too wide leaves voids; clearance that is too tight prevents filler flow. The correct range depends on the filler metal and the assembly, which is why the process is controlled in production rather than set by eye on the bench.
Does the retention method change the blade’s fitment or bolt pattern?
No. The mounting pattern is set by the equipment and the blade, and it stays the same whichever method holds the inserts. What changes is the internal interface: pocket depth, base support and clamping surfaces. Confirm the pattern, the internal interface and the hardware set together at order stage so the delivered assembly matches both the machine and the maintenance plan.
Related articles
 Braze Quality Insert Retention: What the Joint Decides in ServiceCarbide Inserts
 Carbide Grade Selection for Cold and Abrasive ConditionsCarbide Inserts
 Trapezoid vs Bullnose Inserts: Which Geometry Fits the CutCarbide Inserts
 Micro Grain Carbide Inserts vs Standard Grain Grades: Choosing by Wear MechanismCarbide Inserts