
Wear Parts Cost Per Mile and Cost Per Lane Mile: Building the Model
Ask a fleet what its wear parts cost per mile is and the answer usually arrives as an invoice total divided by a guess at annual mileage. That produces a number that cannot be…
Ask a fleet what its wear parts cost per mile is and the answer usually arrives as an invoice total divided by a guess at annual mileage. That produces a number that cannot be used to compare two suppliers, two surfaces or two seasons, which is why so many edge decisions end up back at unit price.
This page builds the model properly: what the published record supports, which inputs decide the answer, what it means for buyers and suppliers, how regions differ, and what to watch over the next twelve months. Every input in the model comes from a fleet record, not from an industry average.
What the Data Shows
Cost per mile is a method, not a published number.
Fleet research shows how to construct a cost per mile from several operating lines; no published source supplies the wear parts figure for a specific fleet.
The method is well established elsewhere. Cost research on heavy vehicle operations, such as the work published by ATRI, treats cost per mile as a constructed figure with fuel, labour, maintenance and capital components, which is exactly how a wear parts figure has to be built. Transportation research from the Transportation Research Board supplies the road programme context, including how maintenance activities are compared across networks, and FHWA highway programme guidance covers how those activities are planned and funded.
On the material side, the inputs that make one blade last longer than another are testable. Hardness and grain size are demonstrated to published methods such as the material and test standards maintained by ASTM, and the measurement discipline behind dimensional claims follows the same route, with reference material from NIST on how measurement and traceability are handled.
What none of those sources does is tell a fleet the answer. A cost per lane mile for a mountain route in February and a cost per lane mile on a flat arterial are different numbers produced by the same fleet in the same season. The model, not the benchmark, is the deliverable.
The Inputs That Decide the Answer
A cost per mile model is only as good as its denominator and its wear data. Six inputs carry almost all of the result, and five of them are already recorded somewhere in the fleet.
The first input is the work unit: lane miles, tonnes moved or machine hours, measured by route class or application rather than as a fleet total. The second is consumable life in that unit, taken from change-out records. The third is the consumable cost, taken from the invoice or from the terms in the written quotation or order documents. The fourth is change-out labour, timed properly rather than estimated, including the second operator where the job needs one. The fifth is downtime valued as the work not completed. The sixth is the failure and fitment line: parts written off because they did not match the attachment.
| Input | Where the fleet gets it | Effect on cost per mile |
|---|---|---|
| Work unit by route class | Route records or plant production data | Sets the denominator, so it changes every other number |
| Consumable life | Change-out log tied to route class | Direct, and the variable a specification change targets |
| Change-out labour | Timed job, including a second operator | Often the largest controllable line |
| Downtime | Work not completed during the change-out or failure | Rises in proportion to how badly the route is delayed |
| Fitment failure | Scrap records and emergency orders | Removable through validation before the order |
| Consumable cost | Invoice or documented commercial terms | Small relative to labour in most fleet models |
The formula is arithmetic, not economics: total cost of the edge, the labour to change it and the share of downtime it caused, divided by the work it completed before it was replaced. Everything interesting happens in how carefully the inputs are taken.
What It Means for Buyers
Two denominators beat one fleet average.
Calculating cost per lane mile by route class exposes where the money goes, and a single fleet-wide average hides exactly that.
Start by splitting the fleet into two or three route or application classes, no more. A class that is too fine produces noise; a single class produces an average that no supplier can act on. Two or three classes are usually enough to show that one route is consuming most of the consumables budget, and that finding by itself changes where the specification effort goes.
Then measure the change-out properly once. Timing a single change-out, on the actual machine, with the actual fasteners, produces a labour figure that can be used for seasons. Most fleets estimate this figure and most estimates are low, because the messy parts of the job – a seized fastener, a lifted machine, a second operator, a job finished in the dark – are the parts that disappear from memory.
Third, compare specifications rather than suppliers where possible. If the model shows the labour line dominating, the useful question is whether a different profile or insert arrangement reduces change-out time, and that is a technical conversation with a manufacturer rather than a sourcing conversation with a distributor. The cost per mile breakdown shows how the lines combine when a specification changes.
Finally, keep the model on one page and one method. A model that changes its denominator between seasons cannot show an improvement, and improvements are the only reason to build it.
What It Means for Suppliers
Suppliers should bring the model, not a discount.
A supplier who can help a fleet structure the measurement is doing something a discount cannot do: making the next comparison easier for the buyer.
The practical offer is a short questionnaire followed by a specification recommendation. Ask for route classes, surface types, attachment details, current profile and grade, change-out frequency and observed failure mode. Those six answers are enough to propose a grade and profile, and enough to state what should change in the model if the proposal is adopted. It also gives the supplier a defensible reason to decline a conversation that is only about unit price.
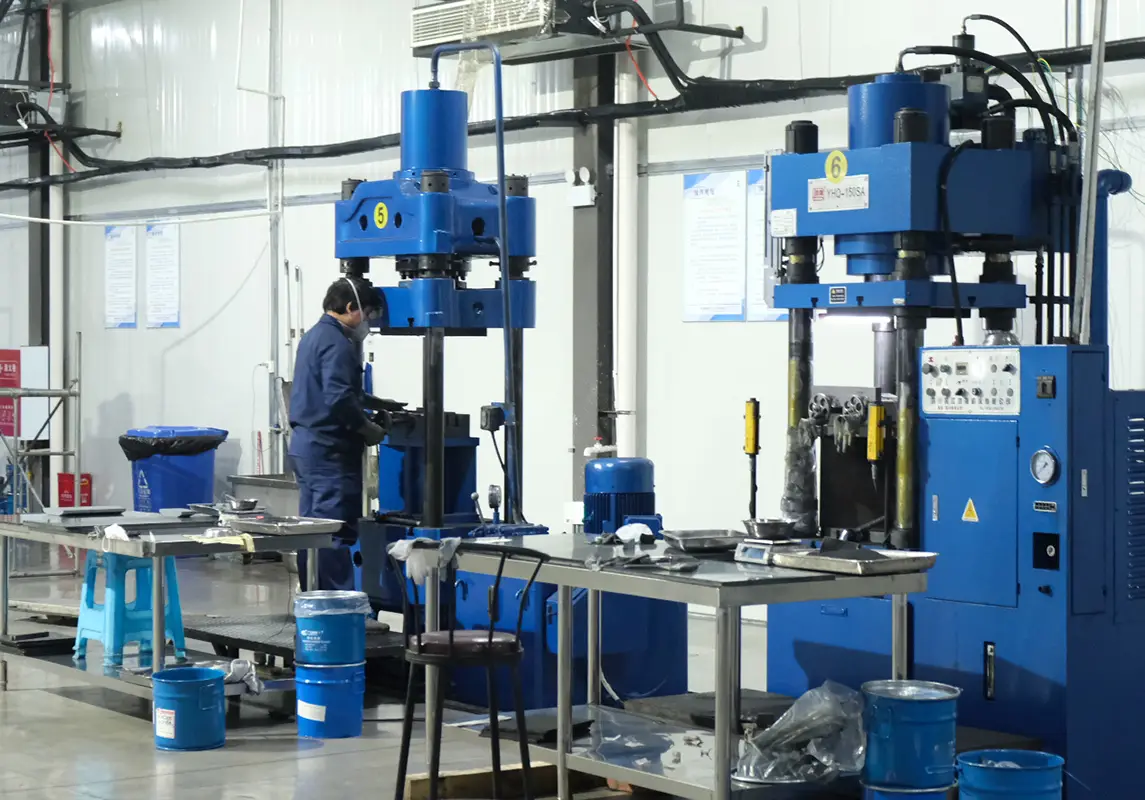
The second supplier-side point is consistency. A cost per mile model rewards predictable wear, so a manufacturer that controls powder preparation, pressing, sintering, brazing with annealing, vulcanization and finishing has an advantage that is measurable by the buyer. This is why the snow plow range is documented by grade and profile, and why lot-level traceability matters commercially rather than only technically.
The third is documentation at delivery. When a fleet runs a model, a failed part becomes a data point, and a data point needs an identity. A traceability reference with each delivery turns a dispute about a number into a short factual exchange, which protects both sides and reduces the buyer’s administration line.
Regional Differences
The model is portable; the inputs are local. Route classifications, labour rates and the value of a missed service window differ enough between regions that a model built in one place will not transfer to another without new inputs, even when the equipment is identical.
In North America, lane miles by route class is a familiar unit and agency reporting encourages it. In Europe, service contracts and technical files tend to make the work unit contractual, so the model often has to align with the measurement already written into an agreement. In the Middle East and parts of Asia, mixed fleets and different applications mean the more useful denominator may be machine hours or tonnes moved rather than lane miles, and fitment failures weigh more heavily because a replacement part travels further to arrive.
Freight and duty treatment affect the consumable cost input differently by region, and the only reliable way to handle it is to record the delivery term under which the part was bought. Two identical parts at the same unit price can produce different delivered costs, which changes the model without changing the specification.
What to Watch Over the Next 12 Months
Watch your own denominator drift, then the input costs.
Most models go stale because the routes change and the denominator does not; external input costs matter, but internal drift breaks the comparison first.
The first thing to watch is route or application change. New development, a reassigned route, a heavier attachment or a different surface all move the denominator without anyone updating the model, and the result is a trend that looks like a supplier problem when it is a measurement problem. Re-check the classification each season and note the change.
The second is the labour line, which moves with operator availability as much as with pay rates. Where a fleet is short of operators, the effective cost of a change-out rises, and the model will show that a faster or longer-wearing specification pays back sooner. That is a self-generated signal, and it is more reliable than any external forecast.
The third is availability of the specified grade. Watch re-order intervals rather than prices: a lengthening interval is the first visible sign of a supply constraint, and it is the point at which a second qualified source with validated fitment becomes worth the engineering effort.
How to Act on This
Build the baseline now, from three records.
A change-out log, a route or application list and one timed change-out are enough to produce a usable baseline this season.
- Split the fleet into two or three route or application classes and write them down.
- Start a change-out log: date on, date off, class, and reason for replacement.
- Time one change-out per class, on the machine, with the real crew.
- Add the fitment failures and emergency orders from the last two seasons to see the removable cost.
- Calculate cost per unit of work per class, then set one specification change and re-measure.
If the baseline shows the labour line dominating, the next step is a technical review of the profile and fastening rather than another round of quotes.
Cost per mile and cost per lane mile are constructed figures, and a fleet that builds them properly ends up with a better specification decision than a fleet that buys on unit price. The six inputs that carry the result are the work unit by class, consumable life, consumable cost, timed change-out labour, downtime valued as work not completed, and fitment failure. Measure once, keep the method stable, and use the model to test one specification change at a time.
Send SENTHAI your change-out log and route classes, and the technical team will review which profile, grade or fastening change would move the cost per lane mile figure most.
Frequently Asked Questions
What is cost per mile and why does it matter for wear parts?
It is a constructed figure: the cost of the part, the labour to change it and the share of downtime it caused, divided by the work completed. It matters because unit price cannot compare two edges that last different distances, and because it moves the conversation onto the labour and downtime lines, which are usually larger than the part itself.
What is the average cost of truck maintenance per mile?
We do not publish that figure, and general averages blend duty cycles too different to be useful. What a fleet can do is construct its own cost per mile from its own records for fuel, labour, maintenance and consumables, using a consistent method. Published fleet cost research describes how such a figure is assembled, which is useful for method rather than for a benchmark value.
How do we handle a mixed fleet with several attachment types?
Measure by application class rather than by machine. Two loaders on the same material can share a class even when the attachments differ, and that grouping keeps the sample large enough to be stable. Where an attachment genuinely changes the duty cycle, give it its own class, but keep the total number of classes small so the comparison stays readable.
What commercial information should be recorded with the model?
Only what the written quotation or order documents actually state, such as volume bands, packaging, sampling and delivery windows, together with the delivery term that fixes where freight and risk transfer. Keeping those terms beside the model makes the cost input auditable and prevents a verbal assumption from becoming the basis of a specification decision.
Related articles
 A Supplier Scorecard for Wear Parts: Metrics That Change BehaviourMarket intelligence, TCO and procurement
 Pricing Snow Removal Contracts: Where the Wear-Part Input BelongsMarket intelligence, TCO and procurement
 Total Cost of Ownership for Fleet Wear PartsMarket intelligence, TCO and procurement
 Snow Removal Industry Statistics and What They Mean for Fleet BudgetsMarket intelligence, TCO and procurement