
Top 5 Best Insert Retention Designs (Brazed, Isolated, Cladding & More)
An insert that leaves the blade is not a wear problem; it is a retention failure, and it turns a maintenance item into a mid-storm replacement. The design that holds the insert decides the…
An insert that leaves the blade is not a wear problem; it is a retention failure, and it turns a maintenance item into a mid-storm replacement. The design that holds the insert decides the season, and the five retention approaches — brazing with controlled surface prep, isolated layouts, rubber encapsulation, cladding, and mechanical fastening — each solve the problem differently. After ranking them for plow duty, the verdict is that a brazed insert with controlled surface preparation and bond verification is the best retention design, with the isolated layout close behind for impact-heavy corridors. This ranking explains each design and how to verify retention before production.
Retention decides the season before the carbide ever wears
The insert can have the best grade and the best geometry, but if the bond fails the edge is gone. Retention failures trace to surface contamination, brazing temperature control, impact overload, and corrosion at the joint, and each design below addresses a different subset of those causes. The ranking judges each design on holding force, crack control, repairability, and cost.
The ranking also assumes the failure history is known. A fleet that loses inserts after curb strikes has an impact story; a fleet that loses them mid-season without heavy impacts has a process story. The failure pattern decides which design to rank first, which is why the buyer should bring the changeout log to the selection, not just the catalog.
The five retention designs ranked by holding force and crack control
| Rank | Design | How it holds the insert | Score |
|---|---|---|---|
| 1 | Brazed insert with controlled surface prep | Sound metallurgical bond | 9.1 |
| 2 | Isolated insert layout | Contains crack paths, holds per unit | 8.8 |
| 3 | Rubber encapsulation | Absorbs impact around the bond | 8.2 |
| 4 | Carbide cladding | Continuous wear layer, no discrete teeth | 7.5 |
| 5 | Mechanical fastening | Pins or screws, serviceable but complex | 6.8 |
Designs ranked 5 through 3 hold under normal duty
5. Mechanical fastening. Pins or screws hold the insert mechanically, which makes replacement simple and avoids brazing variables. The trade-offs are the hardware itself, the drilling that can weaken the carrier, and the maintenance of the fasteners under vibration.
4. Carbide cladding. Cladding applies a continuous carbide wear layer instead of discrete teeth, so there is no tooth to pop out. The design trades insert-level repairability for surface coverage, which is the right trade on abrasion-dominated routes but not where impact concentrates on defined teeth.
The cladding design also changes the wear reading. Because there are no discrete teeth, the wear develops as a thinning of the layer, and the changeout decision follows the measured layer thickness rather than an insert-height check. The inspection routine should be updated to match the design, or the maintenance team will read the wrong signal.
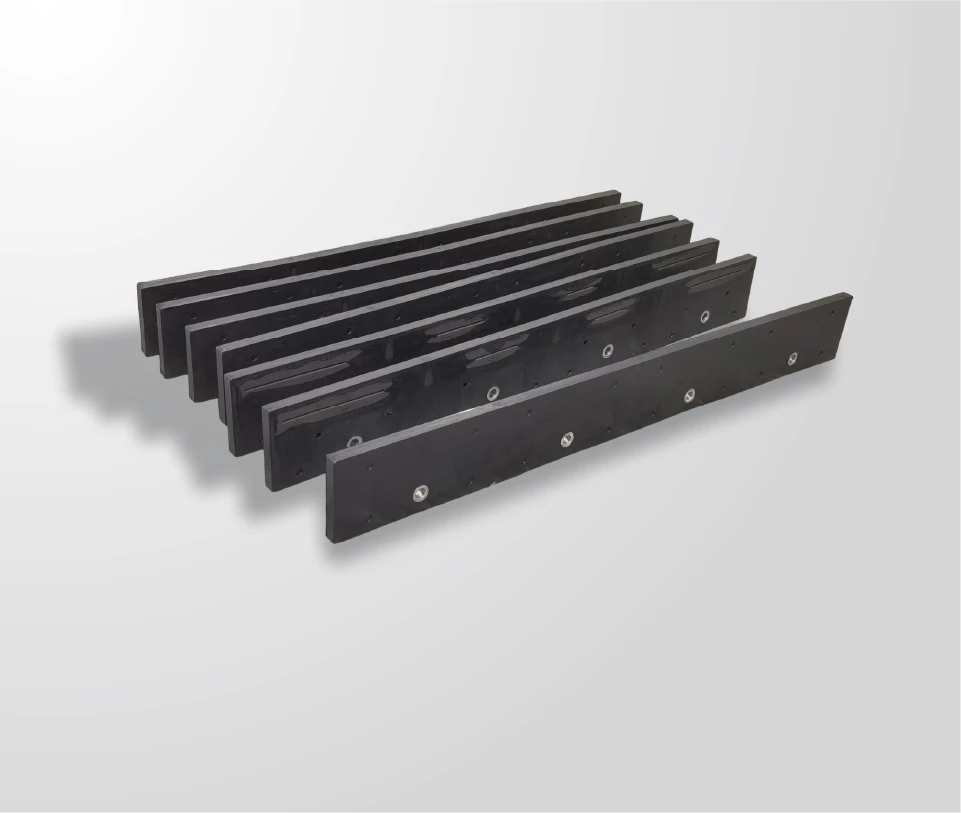
3. Rubber encapsulation. In the JOMA-style construction, the rubber shell cushions the impacts that would otherwise concentrate on the brazed joint. SENTHAI describes its process as chemically and mechanically integrating the holders into the rubber matrix, and the encapsulation protects the bond from the highest-energy strikes.
The top two designs survive the impact corridors
2. Isolated insert layout. Separating the inserts removes the crack path, so a single impact does not take the row with it. SENTHAI describes its isolated carbide insert design as preventing lateral cracking, and the layout is the difference between a contained repair and a section replacement on impact-heavy corridors.
The isolated layout also changes the economics of damage. A section that loses one insert can keep working and be scheduled for repair, while a continuous row that cracks is a section replacement. The graceful failure is the layout’s quiet value, and it is worth more on the corridors where the impacts are a weekly event.
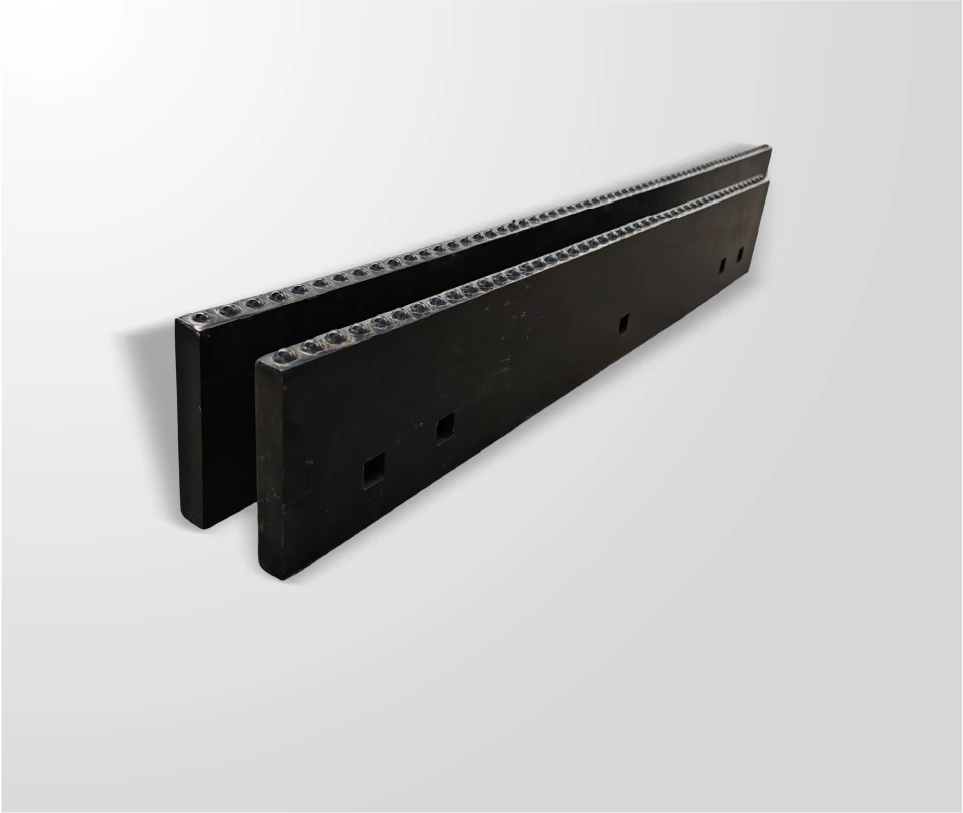
1. Brazed insert with controlled surface preparation. The champion is the metallurgical bond itself. SENTHAI describes a specialized surface preparation that cleans the insert and exposes the cobalt-rich layer for the brazing alloy to wet, and brazing controlled for temperature, alloy flow, and joint geometry. The bond is verified with acceptance criteria and batch records, and it is the design that holds the insert through the season on general duty.
The best retention design for impact duty combines isolation with a sound bond
The champion wins on general duty because the bond is the foundation of every other design: isolation contains cracks only if each insert is bonded soundly, and encapsulation cushions impacts only if the joint underneath is sound. On the highest-impact corridors, the best answer is the combination — a sound brazed bond in an isolated layout, with rubber encapsulation where the surface allows. SENTHAI describes its brazing technology as engineered to withstand high-velocity impacts, and the verification of the bond is the step that separates a retention design from a hope.
The combination also changes the repair economics. A section that loses one insert in an isolated layout can continue and be scheduled for repair, while a continuous row that cracks is a section replacement. The graceful failure keeps the unit on the route and the repair in the shop, which is the retention design’s quiet contribution to the season’s cost.
Verifying retention before production prevents field pop-outs
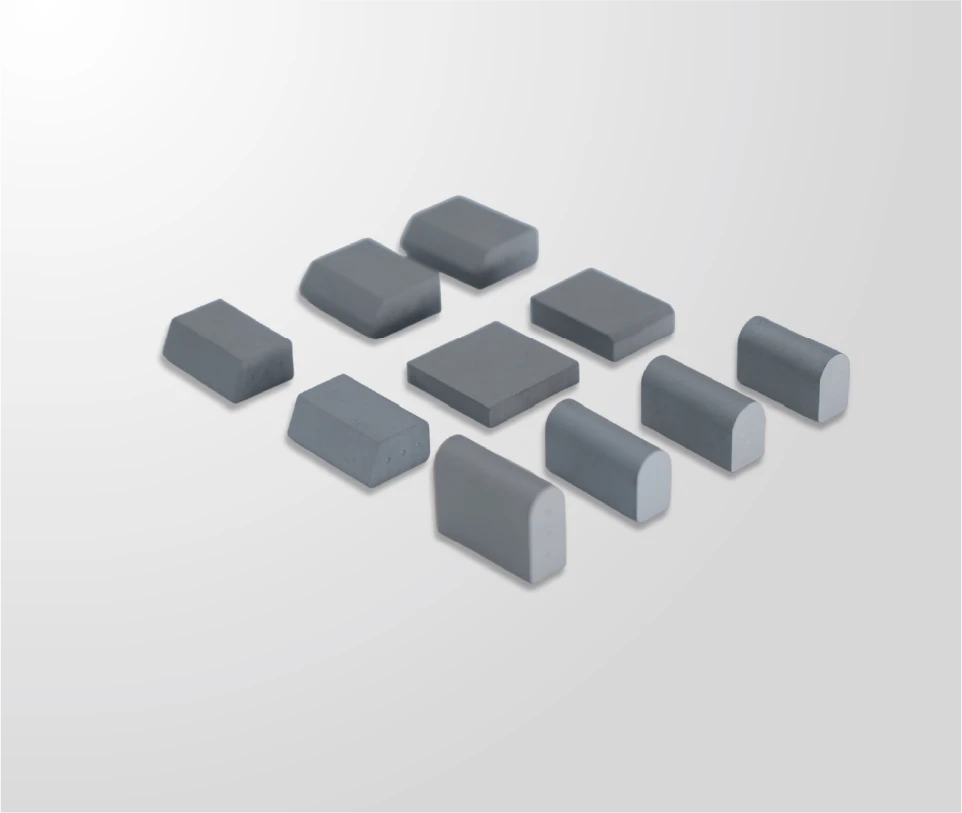
The verification belongs in the supplier qualification: ask for the surface preparation, the brazing acceptance criteria, and the inspection method, and run a sample on the worst route with the inserts inspected after a defined number of passes. The carbide inserts page documents the component side, and the packed ice carbide kit page shows the isolated layout in practice. SENTHAI states that sample blades can be arranged for field testing, which is the right way to validate retention. To confirm the design, send the application, the acceptance criteria, and the failure history through the contact page and ask for the bond verification plan.
The verification should also include the shop check. In the regular inspection, look for inserts that sit proud of the surface, rock slightly, or show a gap at the bond line, and check the bond zone after major impacts rather than only on the schedule. The shop check is the early-warning layer that catches the retention failure before the insert leaves the blade.
The shop check also feeds the supplier file. A pattern of bond failures on the same route, documented with the batch numbers, is the evidence the supplier conversation needs — the retention design is either confirmed or corrected with the data, not the impression. The record is what makes the retention verification repeatable.
The verification should also set the acceptance threshold before the trial. Define the number of passes, the inspection points, and the pass-fail criteria for the bond, and run the sample to that plan. The threshold makes the trial objective, and the objective trial is what the production decision is built on.
The threshold should also cover the batch link: the sample’s bond quality has to be traced to a production run, not a one-off, so the batch records are part of the acceptance. The link is what lets the fleet order the verified design with confidence in the repeat.
The verified design is the one the supplier file records, and the record is the basis of the next order.
Expert view — SENTHAI engineering team: “The bond starts on the surface, not in the flame. The preparation, the temperature, and the acceptance criteria are the retention design.”
Frequently Asked Questions
Why do inserts pop out of blades? The usual causes are surface contamination before brazing, brazing temperature control, impact overload, and corrosion at the joint. Each retention design addresses a different subset.
Is the isolated layout better than a continuous row? On impact-heavy corridors, yes: it contains the crack and prevents a single strike from taking the row. On general duty, a sound bond in either layout holds.
Does rubber encapsulation weaken the cutting? No. The rubber cushions impact around the bond while the carbide does the cutting; the encapsulation protects the joint without reducing the edge.
How do I verify retention before production? Ask for the surface preparation and acceptance criteria, inspect the joints beyond a visual check, and run a sample on the worst route with defined inspection intervals.
Can mechanical fastening replace brazing? It is an alternative for serviceable designs, but the hardware and the drilling add their own failure modes. Brazing remains the standard for plow duty.
What inspection catches a failing bond? Look for inserts that sit proud, rock, or show a gap at the bond line, and check the bond zone after major impacts. The feel check and the bond-line check are the shop’s early warnings.
Why does the isolated layout survive impacts better? Because the separation removes the crack path: a single strike damages one insert instead of traveling through a continuous row. The containment is the layout’s structural value.
What is the most common retention failure cause? Surface contamination before brazing, followed by brazing temperature control and impact overload. The verification of the surface preparation is the first line of defense.
Sources
Related articles
Best Snow Plow Blade Family for Your Fleet: Top 5 ScenariosKnowledge Top 10 Snow Plow Blade Types for Winter Fleets (Ranked by Duty Fit)Knowledge
 Top 5 Best Carbide Blade Configurations for Highway PlowingKnowledge
 Best Snow Plow Blade Materials Ranked: Steel vs Carbide vs Cladding vs Rubber-CarbideKnowledge