
Trapezoid vs Bullnose Inserts: Which Geometry Fits the Cut
Trapezoid vs bullnose inserts compared on wear pattern, surface fit, retention and cost per metre, with the specification points that decide the choice.

Two insert shapes can be made from the same grade, brazed with the same process and mounted on the same blade, and still produce different wear patterns by the middle of a season. Trapezoid and bullnose inserts place their contact area differently, which changes how the edge meets the surface, how load is distributed and how the shape behaves once wear starts. The geometry decision is usually made once per blade family, so it is worth getting right on evidence rather than on a parts diagram.
Trapezoid vs Bullnose Inserts: What Each Geometry Is Designed For
Trapezoid cuts in lines; bullnose rides over uneven ground.
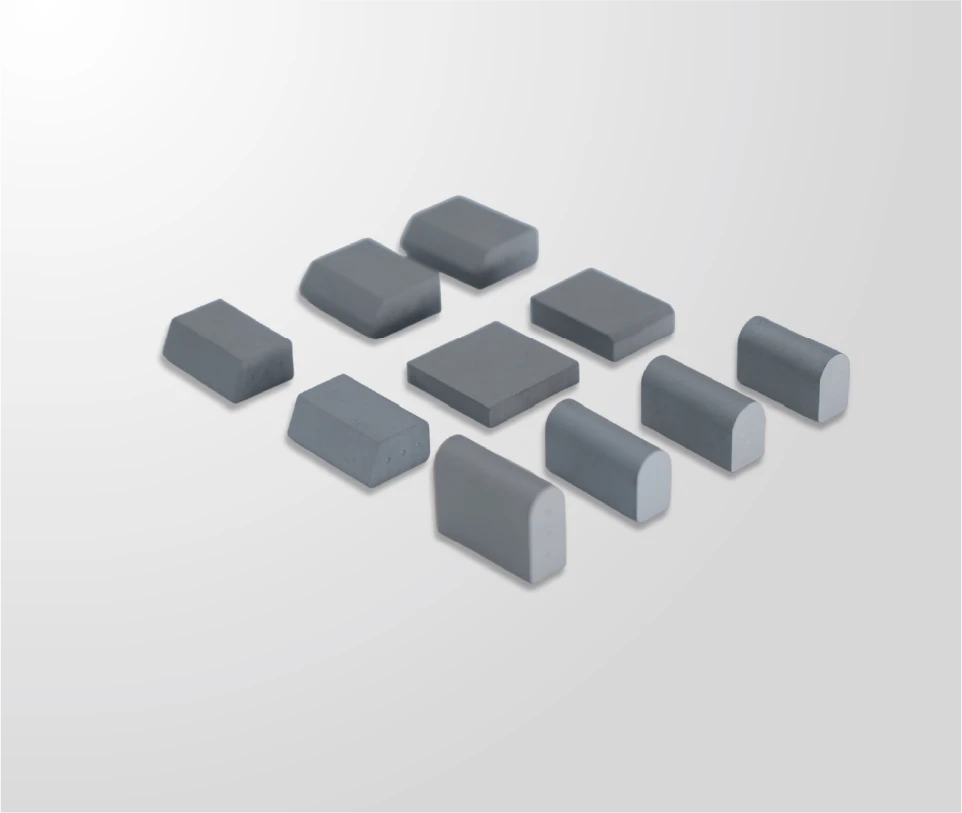
A trapezoid insert presents a defined leading face that concentrates contact along the scraping direction; a bullnose insert uses a rounded profile that tolerates changes in surface angle.
The difference is about how contact is established. A directional shape bites along a narrow band across the cutting width, producing a wear line that develops predictably and can be read from the yard. A rounded shape spreads contact as the blade moves across uneven ground, which reduces the tendency to dig in and catch on surface irregularities. Neither is more advanced; they are answers to different surface problems.
Shape also affects the load path into the blade. A directional insert transmits load along a defined axis, so the pocket or braze area behind it is loaded consistently. A rounded insert distributes load across a wider area and is therefore more tolerant of slight misalignment, which is one reason it appears on equipment that works across varying surfaces. The wider comparison of insert shapes covers the other options available, while this article stays with the decision between the two most common geometries.
How the Two Insert Shapes Differ in Wear and Service Life
Directional inserts wear in a line, rounded ones in a band.
A trapezoid insert concentrates loss along the leading face, so the wear line moves back steadily; a bullnose insert spreads loss over a curved face, so height reduces more broadly and change is less obvious.
That difference changes inspection, not just performance. A directional insert gives an inspector a clear reference: when the wear line reaches a defined point, the edge is due for rotation. A rounded insert demands measurement rather than observation, because the shape hides progressive loss until the change is well advanced. Fleets that run rounded inserts without a measurement routine tend to discover wear later, which compresses the rotation interval available to them.
Both shapes retire through the same two mechanisms: material loss at the contact area and loss of retention at the joint. Geometry influences the first directly and the second indirectly, because the contact area and the load path affect how much stress reaches the braze or pocket. Background on the joining process is published by TWI, and the material behaviour behind both shapes is described by the International Tungsten Industry Association.
Surface and Condition Differences Between the Two Shapes
Surface type separates the two shapes more decisively than any other variable. Hard-packed snow and refrozen surfaces reward a defined leading face that keeps a consistent scraping angle, which is the case trapezoid geometry is built around. Loose gravel shoulders, broken pavement and dirt roads reward a shape that does not dig in when the surface angle changes, which is where a rounded profile performs more predictably.
Abrasive material changes the picture again. On unsealed surfaces the abrasive load is high and constant, and the width of the contact band determines how quickly the insert loses height. A rounded insert spreads that load, which can lengthen the interval between rotations even though it removes material less aggressively. Where a fleet runs the same truck across a mix of surfaces, the shape should follow the dominant surface, and edge rotation should be used to even out exposure across the fleet.
Treatment decisions belong in the same discussion. Where a programme relies on abrasives and de-icing chemicals, the resulting slurry changes how quickly the contact area erodes, and the regulatory context for material use is set out in the EPA’s municipal stormwater guidance. That context shapes how many passes a fleet expects from an edge, which in turn affects how much shape optimisation is worth pursuing.
Retention and Handling Trade-Offs Beyond Wear
Handling differs in ways that crews notice. A directional insert with a defined leading edge is easier to align during fitting, because the correct orientation is visible, and misalignment is obvious. A rounded insert is more forgiving of slight misalignment but also easier to seat incorrectly without noticing, particularly where the pocket has worn. Both cases argue for a fitting check rather than relying on the operator’s judgement.
Retention behaviour follows the load path. A directional insert concentrates load, which makes the quality of the braze or the fit of the mechanical fixing more consequential; a rounded insert spreads load and tolerates small imperfections in the seat. Where a fleet has experienced insert loss on one shape but not the other, the difference is usually in the retention method rather than the geometry, and changing shape is an expensive way to solve a bonding problem.
Serviceability is the last consideration. Mechanically fixed inserts can be replaced individually in the workshop, which suits fleets with their own maintenance capacity. Brazed inserts are replaced as part of the blade assembly, which suits fleets that prefer to exchange complete units and avoid workshop variation. Neither approach is better; they place the work in different places.
Fitment and Equipment Compatibility for Trapezoid and Bullnose Inserts
Geometry does not change the mounting pattern, but it does change what the pattern has to carry. SENTHAI works to plus or minus 0.02 mm dimensional tolerances on carbide components and validates fitment against AASHTO and DIN bolt patterns before release, which matters more as the insert profile becomes more directional. AASHTO published standards remain the reference for agency specifications, with DIN covering European and export conventions.
Where inserts are supplied for retrofit onto an existing blade, the pocket geometry and the seat condition decide the outcome more than the insert’s external profile. Check that the seat is clean, flat and to depth, and confirm the retention method matches what the blade was designed for. Mixing a directional insert into a pocket cut for a rounded profile changes the contact pattern and the load path, even where the insert seats without obvious movement.
Cost Per Metre of Edge Compared Across Trapezoid and Bullnose Inserts
Cost per metre of edge is the comparison that resolves the shape question, and its inputs are the same for both geometries. The general model is set out on the cost per mile page; what changes between shapes is how the inputs behave.
| Input | Trapezoid insert | Bullnose insert |
|---|---|---|
| Unit price per insert | Depends on profile and grade rather than on the shape itself | Depends on profile and grade rather than on the shape itself |
| Contact band and wear rate | Narrow band, faster visible wear line, easier to read | Wider band, slower visible change, needs measuring |
| Insert count per edge | Set by spacing, which is a separate specification decision | Set by spacing, which is a separate specification decision |
| Inspection cost | Lower, because the wear line is visible from the yard | Higher, because height has to be measured at fixed points |
| Retention risk | Load concentrated along a defined axis | Load spread across a wider area |
| Surface fit | Hard-packed and refrozen surfaces | Unsealed, broken or angled surfaces |
The table shows why a simple price per insert rarely settles the question. Two shapes with the same unit price can produce different inspection costs and different intervals, and the difference usually appears in labour and in the risk of a change falling inside a storm cycle rather than in the parts line.

Insert Shapes: When Each One Is the Wrong Choice
A directional insert is the wrong choice where the blade works across surfaces that change angle constantly, because the defined leading face can catch on irregularities and transfer shock into the retention system. It is also the wrong choice where the fleet has no measurement routine, since the shape hides wear in a way that rewards operators who check and punishes those who assume.
A rounded insert is the wrong choice where the fleet needs a visible reference point for rotation decisions, or where the route is uniformly hard-packed and the extra tolerance for surface variation brings no benefit. It is also the wrong choice where the added inspection effort is not resourced, because a shape that requires measurement will not be measured if the schedule does not include it.
The most expensive mistake is switching shape to solve a retention problem. If inserts are leaving the blade rather than wearing out, the cause lies in the bond or the fixing, and a geometry change adds cost without addressing it. Photographs of the returned edges, taken at the same points each rotation, are the cheapest way to keep that distinction clear.
Trapezoid and bullnose inserts differ in where they place contact and how they distribute load, and those two properties drive wear pattern, inspection effort and retention risk. The choice follows from the dominant surface on the route and the fleet’s willingness to measure rather than glance.
Run the comparison on cost per metre of edge, with inspection and retention risk included, and confirm the pocket or fixing method the blade was designed for before ordering. That keeps the decision on the same footing as the blade and grade specifications it sits between.
Send SENTHAI the surface mix, carrier type and current insert pattern, and the technical team will review which geometry suits the route and what tolerance the blade pocket requires.
Frequently Asked Questions
Can trapezoid and bullnose inserts be used on the same blade?
They can be fitted to the same blade where the pockets accept both profiles, but mixing them complicates the wear record. Differences in insert height at inspection can then come from position or from shape, making it harder to judge the interval. Where a route has genuinely different sections, specify one shape for the dominant condition and manage exposure through edge rotation instead.
Which insert shape lasts longer?
Neither shape lasts longer in the abstract. A directional insert concentrates wear along a narrow band, so material loss becomes visible sooner but develops predictably. A rounded insert spreads wear across a wider area, which can extend the interval while making the change harder to see. The answer depends on surface type, abrasive load and how the fleet inspects its edges.
How many inserts per metre should a cutting edge carry?
Spacing is a separate specification decision from shape, and it trades cost against contact density and mass at the leading edge. Closer spacing can extend the interval between rotations but raises the cost per metre of edge. Specify spacing against the route and the rotation cycle, and keep it constant across the fleet so that wear readings remain comparable between trucks.
Does insert shape affect the bolt pattern or mounting hardware?
The mounting pattern is set by the blade and the equipment, not by the insert profile, so the bolt pattern does not change with shape. What can change is the load the pattern carries and therefore the hardware condition required to hold it. Confirm the pattern, hole condition and hardware set when changing profile on an existing blade, and ask the supplier to confirm compatibility in writing.
Related articles
 Micro Grain Carbide Inserts vs Standard Grain Grades: Choosing by Wear MechanismCarbide Inserts
 Brazing Carbide Inserts: Surface Prep and Bond StrengthCarbide Inserts
 Replaceable Carbide Inserts vs Full-Length EdgesCarbide Inserts
 Carbide Insert Retention: Preventing Pop-Out and Cold JointsCarbide Inserts