
Packed Ice Kit Replacement Intervals: Setting Them From Evidence
Packed ice kit replacement intervals set from measured evidence: what to track per component, what shortens an interval and when to replace the assembly.

Replacement intervals are usually inherited from a supplier’s general guidance or set to match the calendar, and both approaches ignore the two variables that actually decide the answer: the surface each group works and the load its operators apply. On packed ice routes, intervals also depend on whether the kit is losing material or losing contact, and those two conditions call for different replacement logic.
What Packed Ice Kit Replacement Intervals Have to Establish
An interval has to state what ends the life of a kit.
For a kit working abrasive surfaces, life ends when the remaining material reaches its working threshold. For a kit working refrozen surfaces, life often ends when contact can no longer be maintained, which may happen while material remains.
The distinction matters because a single interval figure cannot describe both. A fleet that sets its interval from material loss alone will keep a kit in service after it has stopped clearing, while a fleet that sets it from clearing performance alone may retire material that still has service left. The practical answer is to record both measures and set the interval on whichever is reached first for that group.
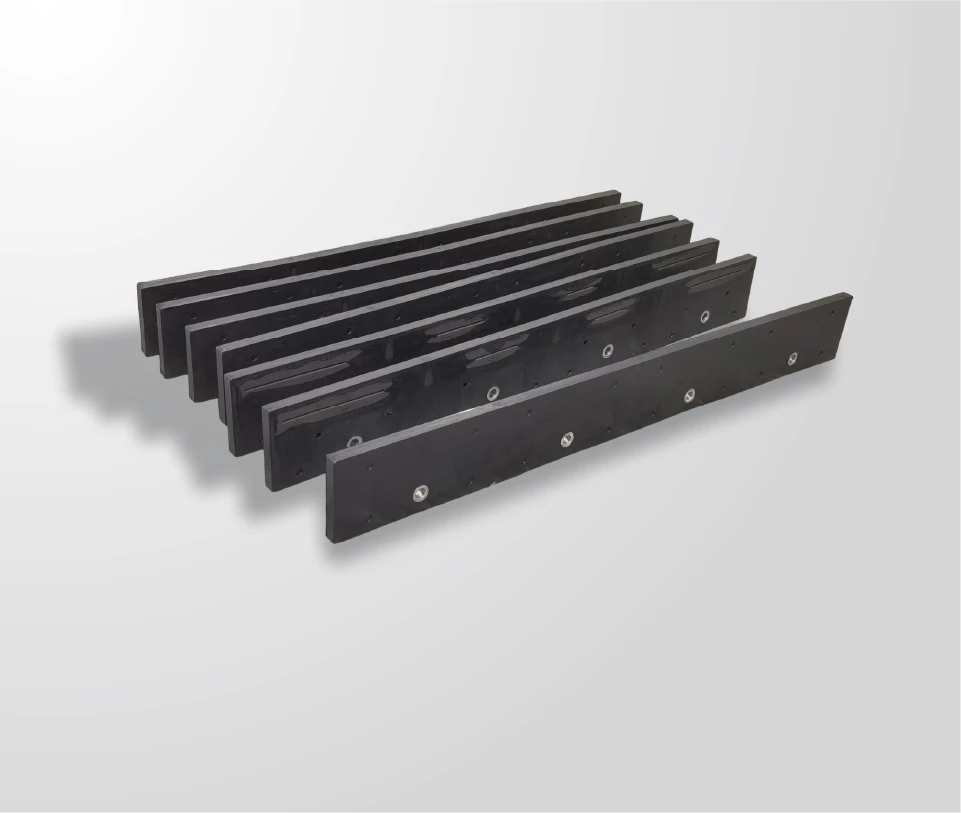
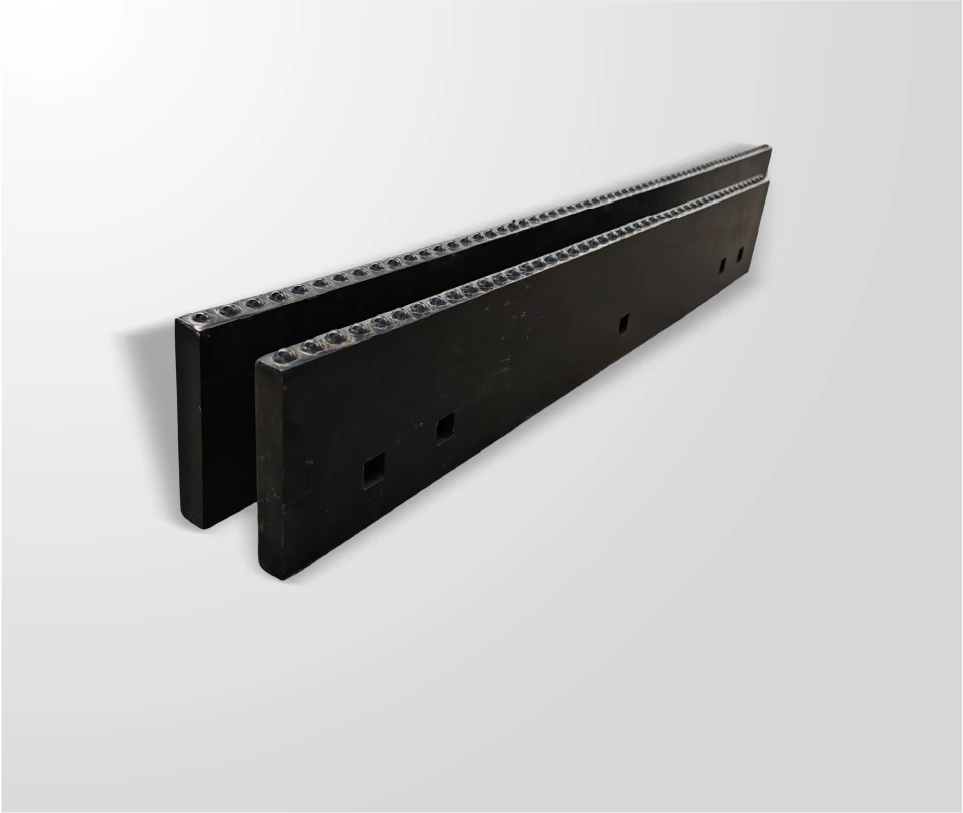
The specification and arrangement the kit was built to are described in the packed ice kit specification guide, and the measurement discipline behind the readings is set out in the guide to measuring a blade for replacement.
Component-Level Intervals and What Each One Depends On
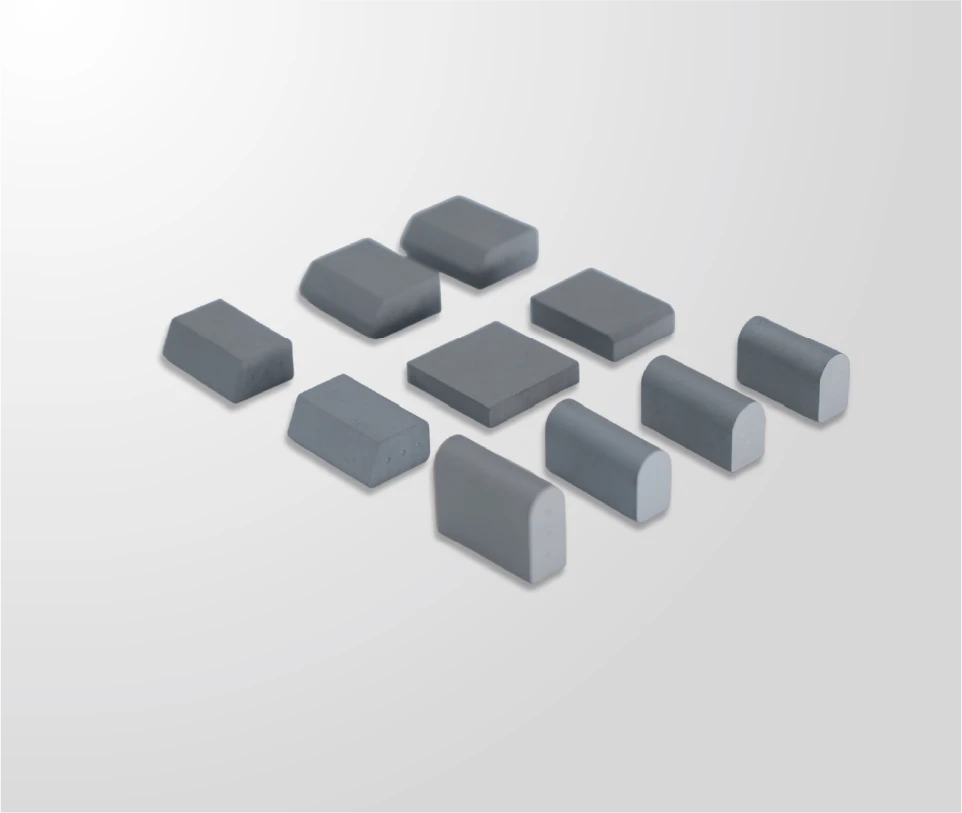
Different components reach their limit for different reasons. The carbide working surface is consumed by abrasion, and its interval depends on abrasive content in the surface and the distance covered. The joint between carbide and body is loaded by shock and by the pressure applied when contact is poor, so its condition depends on route debris and on operator behaviour as much as on distance.
The mounting hardware and the mounting face are the third component group, and they are the ones most often overlooked in an interval calculation. Fasteners lose preload over time and under vibration, and the mounting face wears as successive assemblies are clamped against it. Where a fleet replaces kits on a material interval without checking the mounting face, it eventually discovers the problem through loosening rather than through inspection.
A practical approach is to track three intervals per group rather than one: the material interval at which kits reach their working threshold, the hardware interval at which torque checks find declining preload, and the mounting face interval at which dimensional checks show the face is no longer a suitable base. Those three together describe the assembly’s service life rather than the cutting edge alone.
Measurements and Records That Set the Interval
The material interval is set from height readings at fixed reference points across the working width, taken at each check and compared with the previous reading. That gives a rate rather than a single figure, which is what allows an interval to be planned rather than discovered. The reading should be taken at the same points each time, with the same method and datum.
The hardware interval is set from torque values recorded at each check, with attention to whether any position declines repeatedly. A single low reading after a fitting can be corrected; the same position declining across checks points to the mounting face or to the hardware set rather than to the fasteners themselves. The mounting face interval is set from dimensional checks of flatness and hole condition, recorded each time the assembly is removed.
The record should also capture the reason each kit was removed. Retired for wear, retired after damage and retired because the season ended are three different outcomes, and only the first belongs in an interval calculation. SENTHAI inspects and archives every batch and works to plus or minus 0.02 mm dimensional tolerances on carbide components, so a question about a specific kit can be reviewed against its production record; the quality control and batch traceability page describes what that record contains.
Conditions That Shorten or Extend the Interval
Four conditions shorten an interval. Higher abrasive content in the surface, whether from gravel shoulders or from spread grit, increases material loss. Embedded debris damages the joint and can end a kit’s life before the material limit is reached. Hard, refrozen surfaces reduce contact, which encourages compensating down-pressure and shortens hardware life. And a mounting face that is already worn shortens the usable life of any kit fitted to it.
Conditions that extend an interval are the mirror image. Consistent, smooth surfaces with low abrasive content produce even wear, well-maintained mounting faces hold preload, and operators who can rely on contact working do not apply unnecessary pressure. Those factors are worth recording deliberately, because an interval improvement that follows a change in operating practice should be documented and repeated rather than treated as a fortunate season.
Weather variability should be accounted for explicitly. Where a season produces fewer refreeze events than usual, the interval measured from that season is longer than the underlying capability of the specification, and applying it to the next winter will produce an early failure. Recording the number and duration of ice periods alongside the interval keeps the figure in context, and seasonal guidance published by the National Weather Service provides a reference for the conditions the group actually worked.
A useful convention is to record ice periods in the same log as the wear readings, with dates and duration. The log then shows how a group’s usage is distributed across the winter rather than only its total, and a season with two severe weeks reads differently from a season with six moderate ones, even where the total wear is similar. That distinction matters when the interval is being used to plan the next winter’s holding.
Replacing Components Versus the Assembly
The decision between replacing parts and replacing the assembly follows the same logic as any retention choice. Where a single insert has failed and the surrounding bond is sound, replacement can be considered provided the work is done with controlled heat, correct filler and clean surfaces. Where several positions have moved or a section has failed, the assembly should be treated as unserviceable rather than patched.
Assembly replacement retires the remaining material along with the worn section but returns a kit with a consistent working face and controlled joint quality. Where a fleet works ice routes and contact is the limiting factor, that consistency has value, because a working face that varies between trucks makes the comparison of results difficult. Where wear is uneven and the mounting interface is sound, individual replacement or rotation uses material more efficiently.
Either way, the decision should be recorded with its reason. A fleet that records only that a kit was replaced has a consumption figure; a fleet that records why has an interval by cause, which is what supports the next specification decision. Property test methods published by ASTM allow a grade question to be checked where a failure is disputed, and the standard patterns published through AASHTO define the fitment the assembly was produced to.
Two practical consequences follow from that record. First, a fleet that replaces whole assemblies needs the units in stores to match the interval it is planning, so the holding quantity is derived from the interval and the number of trucks rather than from a percentage. Second, a fleet that replaces individual components needs the seat and mounting face condition recorded for each body, because an insert fitted into a worn seat will not reach the interval the material limit suggests.

The design intent behind the assembly, and the reason contact can fail before the material runs out, is described in the material on what a packed ice carbide kit is and how it works.
Tools and Safe Handling During Interval Checks
The tools needed to set an interval are the tools used for inspection: a straight edge or gauge, a torque wrench, a light and hand protection. Their calibration matters more than their complexity, because an interval built on readings from an out-of-calibration gauge is a precise number with an unknown basis.
Handling is the physical risk during replacement. Kits and edge assemblies are heavy and awkward, and removal often happens in poor conditions at the end of a shift. Assessment principles for load handling are published by the UK Health and Safety Executive, and general workshop requirements for hand and power tool use are set out in the OSHA occupational safety and health standards.
Reviewing Intervals at Season End
The review should be an arithmetic exercise rather than a discussion. For each group, calculate the interval from recorded readings, note how many kits reached the material limit and how many were retired for other reasons, and compare the result with the interval in force. Where they differ, the input that changed is usually identifiable: a different route assignment, a change in treatment practice, or a mounting face that has reached the end of its life.
Two adjustments follow. Where the material limit is consistently reached before the scheduled check, shorten the interval for that group. Where kits consistently retain substantial material at replacement, either extend the interval or examine whether the retirement is being driven by contact and hardware condition instead. Either way, the following season’s plan is set from the group’s own data rather than from a fleet-wide figure.
Packed ice kit replacement intervals are set from two limits rather than one: the material threshold and the point at which contact can no longer be maintained. Hardware and mounting face condition sit alongside both, because they decide whether a kit can be fitted accurately at all.
Measure at fixed points, record the reason for every removal, and calculate the interval per group at season end. That turns replacement from a calendar event into a decision supported by the fleet’s own records, and it makes the next specification change a comparison rather than a guess.
Send SENTHAI your measured readings, replacement records and route groups, and the technical team will review the intervals, thresholds and mounting face checks for each group.
Frequently Asked Questions
How do I set a replacement interval for a packed ice kit?
Set it from measured readings at fixed points, taken at each check and compared with the previous reading to give a rate. Then set the interval on whichever limit the group reaches first: remaining material, or the point at which contact can no longer be maintained. Record the reason for every removal so that only wear retirements feed the calculation.
Should the mounting face be part of the interval calculation?
Yes. The mounting face wears as successive assemblies are clamped against it, and once it is no longer flat, no correctly made kit will seat accurately. Track it with dimensional checks each time an assembly is removed, and record the results against the blade rather than the kit, since the face outlives several kits.
What happens if a winter produces less packed ice than usual?
The measured interval will be longer than the specification’s underlying capability, and applying it unchanged to a harder winter produces an early failure. Record the number and duration of refreeze periods alongside the interval so the figure can be interpreted in context rather than treated as a fixed property of the kit.
Can individual components be replaced instead of the whole kit?
Where a single insert has failed and the surrounding bond is sound, replacement can be considered if the work is done with controlled heat, correct filler and clean surfaces. Where several positions have moved or a section of the bond has failed, the assembly should be treated as unserviceable, because the load path becomes unpredictable and the blade body is at risk.
Related articles
Packed Ice Kit Compatibility Across Plow MakesPacked ice carbide kits Packed Ice Kit Storage and Season Prep: Protecting the AssemblyPacked ice carbide kits
 Packed Ice Kit Cost Model: Building a Programme CasePacked ice carbide kitsIce Control Alternatives Compared: Where Packed Ice Kits FitPacked ice carbide kits