
Carbide Grader Blades for High-Abrasion Road Surfaces
A carbide grader blade becomes the cheaper option at a definable point, not a matter of opinion. It arrives when the cost of changing steel edges — labour, fasteners and hours the machine is…

A carbide grader blade becomes the cheaper option at a definable point, not a matter of opinion. It arrives when the cost of changing steel edges — labour, fasteners and hours the machine is not grading — exceeds the premium on an edge that stays in the moldboard for the whole programme. On crushed surfacing, aggregate shoulders and gravel roads re-graded several times a season, that threshold is crossed quickly. On soft material with low annual hours, it never is.
Where Carbide Changes the Cost Equation
Carbide wins where abrasion and downtime both cost money.
A carbide grader blade pays for itself when the material is abrasive enough to consume steel edges quickly and an hour of downtime costs more than the edge premium; on soft material and light use it does not.
Steel edges fail by losing section. Carbide edges resist that loss because the working surface is cemented tungsten carbide rather than steel, so the profile holds and the machine keeps cutting instead of polishing. The economics follow: fewer changes per season, fewer fasteners, fewer shop hours, fewer passes to bring a road back to grade.
Two conditions must hold for the arithmetic to work. The material has to be genuinely abrasive. And the machine must be earning enough per hour that stopping it is expensive. A fleet grading soft shoulders twice a year will not recover the premium; a contractor on a gravel-road maintenance contract at production rates will.
The third condition is fitment. A carbide edge delivers its wear life only if it seats flat and stays clamped, which puts pattern accuracy, countersink condition and the flatness of the moldboard’s lower lip in the same discussion as the carbide itself. That is the difference between a carbide edge and a length of hardened plate.
Grade and Insert Geometry for Grading
Grade selection for grading is a hardness and toughness decision, and the two move in opposite directions. A harder grade resists abrasive wear and chips more readily under impact; a tougher grade absorbs shock and wears faster. The right balance follows from how much embedded stone, frozen material or buried obstruction the edge will meet.
Grain size is the second lever. Micro-grain carbide reaches high hardness with better transverse rupture strength than a coarse-grain grade of the same hardness, which matters on grading work where the edge sees intermittent shock as well as steady abrasion. The material properties that make this possible are documented by carbide producers such as Hyperion Materials & Technologies and Element Six, and the wear-mechanism background sits with industry references from ASM International.
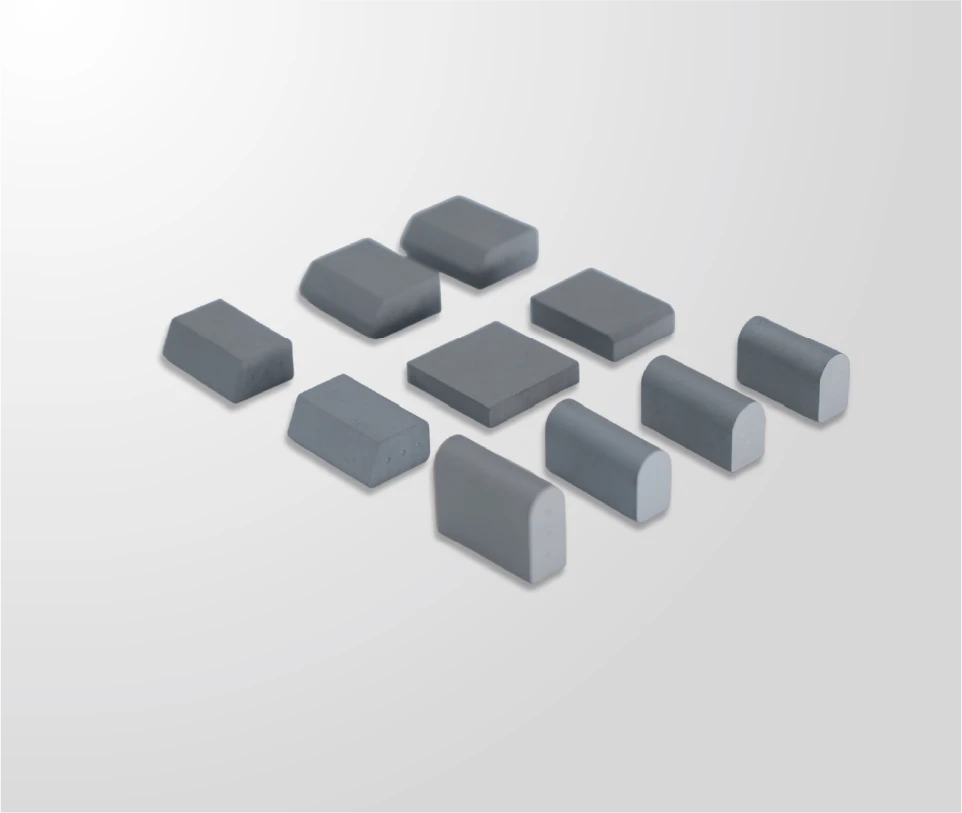
Geometry decides behaviour at the cutting line. Trapezoid profiles present a broad wear face and are used where the edge must hold a line under load; bullnose profiles concentrate the cutting action and suit material that has to be broken rather than shaved. Insert spacing sets how much steel body remains between inserts and therefore how the assembly wears once the carbide begins to recede.
None of this should be guesswork. Grade, grain size and geometry are documented attributes, and a buyer evaluating a supplier is entitled to see them named and held constant across orders.
How the Edge Is Fixed to the Moldboard
A steel body with brazed inserts, bolted like any edge.
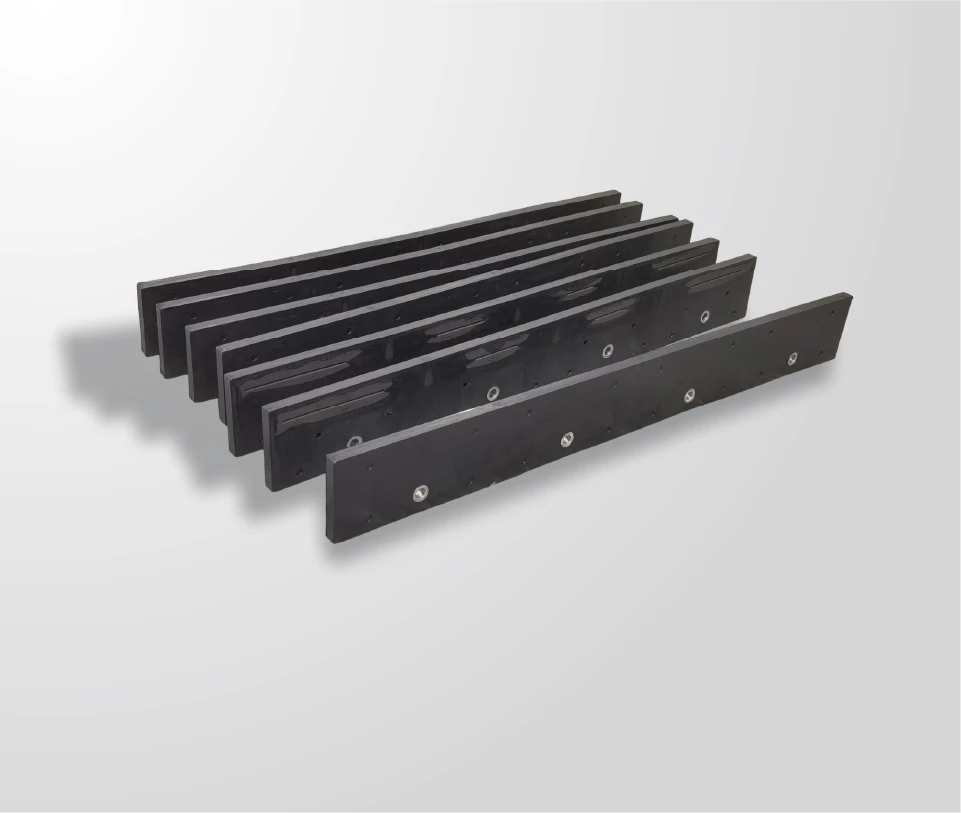
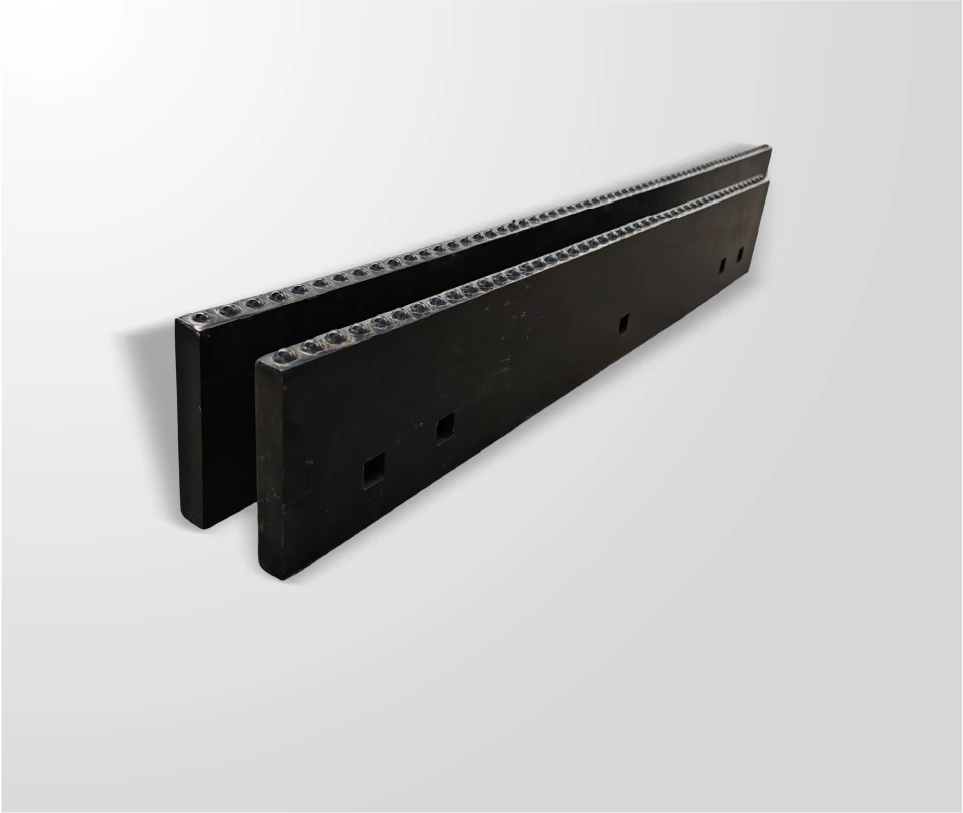
The carbide is brazed into pockets machined in a steel body; that body is then bolted to the moldboard through the same pattern a steel edge uses, so the mounting itself is unchanged.
What changes is the joint between the two materials. Brazing holds the inserts in place, and its quality decides whether the edge fails by wearing out or by shedding inserts. A sound braze penetrates and bonds across the full pocket area; a poor one leaves voids that become crack initiation points under repeated load. The mechanics of the process are described in the technical material published by TWI.
At SENTHAI, edges and inserts are joined by automated high-temperature induction brazing followed by annealing, the same production route used for the company’s carbide edges and inserts. The relevant point for a buyer is the consequence rather than the process name: a repeatable, documented joint instead of a bench operation whose result depends on the day.
The steel body matters too. It carries the bending load, holds the pattern and anchors the inserts. Body grade and section thickness are chosen to match the machine class, and both should be stated on the quotation rather than assumed from a catalogue length.
Fitment and Tolerance Requirements
A carbide edge is bought against a moldboard, so fitment data is part of the product definition. A quotation that names only a length and a machine model is not a specification: hole pattern, countersink angle, section shape and tolerance are all left open, and any one of them can render the edge unusable.
- Hole pattern. Spacing, diameter and hole-centre-to-edge distance, measured from the moldboard or taken from a drawing.
- Countersink. Matched to the fastener so plow bolts seat flush and hold torque.
- Section shape and thickness. Matched to the moldboard arc and the load the machine class imposes.
- Dimensional tolerance. SENTHAI works to ±0.02 mm on machined features; the tolerance should be quoted, not assumed.
- Flatness at the seating face. An edge that does not seat flat will rock, loosen and fail at the holes whatever carbide it carries.
One question is worth asking of any supplier before an order: is the pattern validated against a drawing or a physical sample before production? Fitment verification against a drawing or sample is a documented step at SENTHAI, and it prevents the most expensive outcome in this product category — a full order that cannot be fitted. Machine interface conventions behind those drawings are published by SAE, and the material and test standards a public buyer may need to reference come from ASTM and the AASHTO publications programme.
Documentation to Request With the Quote
Documentation separates a carbide edge supplier from a plate supplier, and it costs nothing to ask for it before the order is placed. A buyer evaluating a new source should be able to obtain the grade designation and its documented properties, the insert profile and spacing, the body section, the pattern drawing with tolerance, and the inspection and traceability arrangements that apply to the batch.
Traceability deserves specific attention. An edge that fails early must be attributable: which batch of powder, which brazing run, which inspection records. SENTHAI operates lot-level traceability, with every batch inspected and archived, so a failure can be investigated rather than argued about. A supplier that cannot describe its traceability in concrete terms is unlikely to resolve a performance dispute in the buyer’s favour.
For public-sector work, add the documents the tender actually requires: dimensional inspection results, material declarations where relevant, and packaging and labelling to the buyer’s specification. Handling and shipping documentation for any powders or regulated materials in the supply chain may also come into scope, which is where the powder-metallurgy industry material from MPIF and the tungsten industry data published by ITIA are useful references. It is cheaper to fix that list before the order than after delivery.

Failure Modes Specific to Carbide Edges
Carbide edges do not fail the way steel edges do, and reading the failure correctly is what makes a claim or a specification change meaningful. Four patterns account for most returns.
| Pattern | What it indicates | Corrective action |
|---|---|---|
| Insert loss with clean pockets | Braze coverage or joint strength at fault | Raise with the supplier and request braze process data |
| Chipped inserts at intervals | Impact loading, or a grade too hard for the duty | Move to a tougher grade and review operator technique |
| Even insert wear with body erosion between them | Normal service life; the body is now the limiting factor | Review body grade or insert spacing on the next order |
| Cracking outward from bolt holes | Edge not seating flat, or elongated holes in the moldboard | Inspect and correct the seating face before reordering |
Two of those patterns are not edge problems at all, which is why a supplier’s response to a failure report is a useful test. A supplier that asks for photographs, measurements and duty conditions is diagnosing. One that ships a replacement without asking is not.
Cost Per Lane Mile on Abrasive Surfaces
The comparison a procurement team needs is cost per lane mile of grading, assembled from four inputs the fleet already holds: edges consumed per lane mile, unit price per edge, the cost of one change-out, and the value of the grading hours lost while the machine is down.
On abrasive surfaces the first and third inputs do the work. A steel edge consumed three times in the interval a carbide edge covers multiplies both the part cost and the change-out cost by three, and each change also removes grading hours. Once those lines are included, the carbide premium is being weighed against a cost several times the steel unit price, not a little above it.
The model also shows where carbide is the wrong answer. If the material is soft, if annual hours are low, or if the machine is a spare that runs occasionally, change-out cost is small and the premium is not recovered. Publishing both sides of that calculation internally is what turns a purchase decision into a defensible specification, in the same way that public programmes justify edge choices through the documented material and maintenance references published by the AASHTO and FHWA programmes.
One caution belongs with any life claim. Multipliers quoted without the conditions they were measured under are not comparable: ask what material, machine class and down-pressure the figure came from, then hold the answer against the fleet’s own duty.
Carbide grader blades earn their place on abrasive roads, at high annual hours, where stopping the machine is expensive. Inside that envelope, five things decide whether the purchase succeeds, and all five are settled before the order: grade and grain size for the duty, insert profile and spacing, a body matched to the machine class, a validated pattern held to a stated tolerance, and documentation that makes the edge attributable. Get those right and cost per lane mile falls. Leave any of them unstated and the premium is being paid for an outcome nobody has defined.
Send SENTHAI the moldboard pattern, the material the machine grades and the current cost of a change-out, and the technical team will confirm grade, insert geometry, body section and fitment tolerance for the duty, together with the documentation that travels with the batch.
Related reading: wear parts beyond plows.
Frequently Asked Questions
How long does a carbide grader blade last compared with steel?
It depends on material and duty, so a single multiplier is not meaningful across programmes. The correct comparison is edges consumed per lane mile on the fleet’s own roads: carbide resists abrasive loss, so it returns more grading hours per unit on crushed surfacing and gravel. Ask any supplier for the material and conditions behind a life claim before using it in a budget.
Can a carbide grader blade be rotated or reversed like a steel edge?
It depends on the insert layout and body design of the specific part, so this is a question for the supplier rather than a general rule. Where inserts are distributed symmetrically on a reversible body, end-for-end reversal extends service life the same way it does on steel. Where the edge is designed for one orientation only, the replacement trigger is measurement.
What tolerance should a carbide grader edge hold at the bolt holes?
Ask for the tolerance to be quoted rather than assumed. SENTHAI works to ±0.02 mm on machined features and verifies the mounting pattern against a drawing or physical sample before production. The number matters because an edge that does not seat flat will loosen, crack at the holes and shed inserts, turning a wear part into a fitment claim.
Do carbide grader blades need different fasteners?
They use the same plow bolts and pattern as a steel edge of the same profile, so the fastener type does not change. What changes is the consequence of poor clamping: a carbide edge that is not held flat concentrates load at the inserts and at the holes. Replace fasteners with the edge and confirm the countersink matches before tightening to the specified torque.
Related articles
 Asphalt Milling Teeth: Grade, Holder and Cost Per TonneGrader blades and road grading cutting edgesGrader Blade Thickness, Hole Pattern and Bolt GradesGrader blades and road grading cutting edges
 Grader Blade Versus Cutting Edge: What Your Machine Actually NeedsGrader blades and road grading cutting edgesMotor Grader Cutting Edge Selection: Carbon, Heat-Treated and Carbide ComparedGrader blades and road grading cutting edges