
Packed Ice Kit Compatibility Across Plow Makes
Packed ice kit compatibility across plow makes: how pattern, width and mounting height decide fitment, and the checks to complete before ordering.

Compatibility is the question that decides whether a packed ice specification can be applied across a mixed fleet. Two plow makes can share a nominal blade width and still differ in hole diameter, hole row position and the height at which the blade sits on the moldboard. Because a kit changes the mass and the contact behaviour of the assembly, a fitment error that would be a minor inconvenience on a standard edge becomes a performance problem on ice routes.
Which Packed Ice Kit Compatibility Points Decide Fitment
Pattern, width and mounting height decide compatibility.
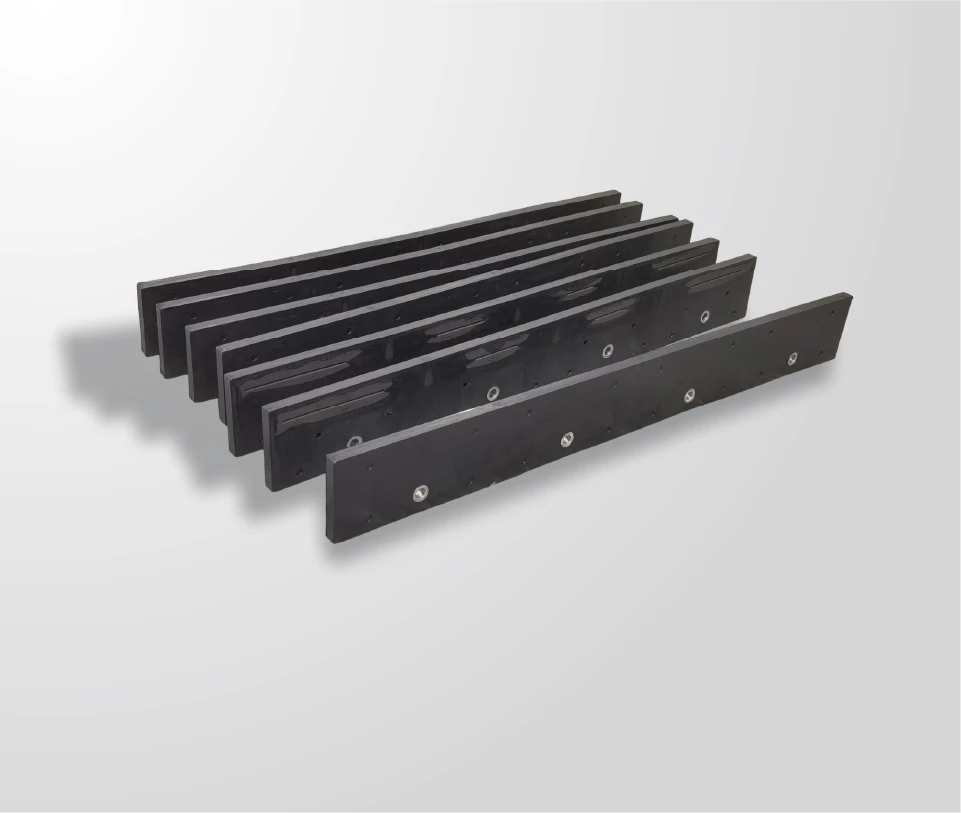
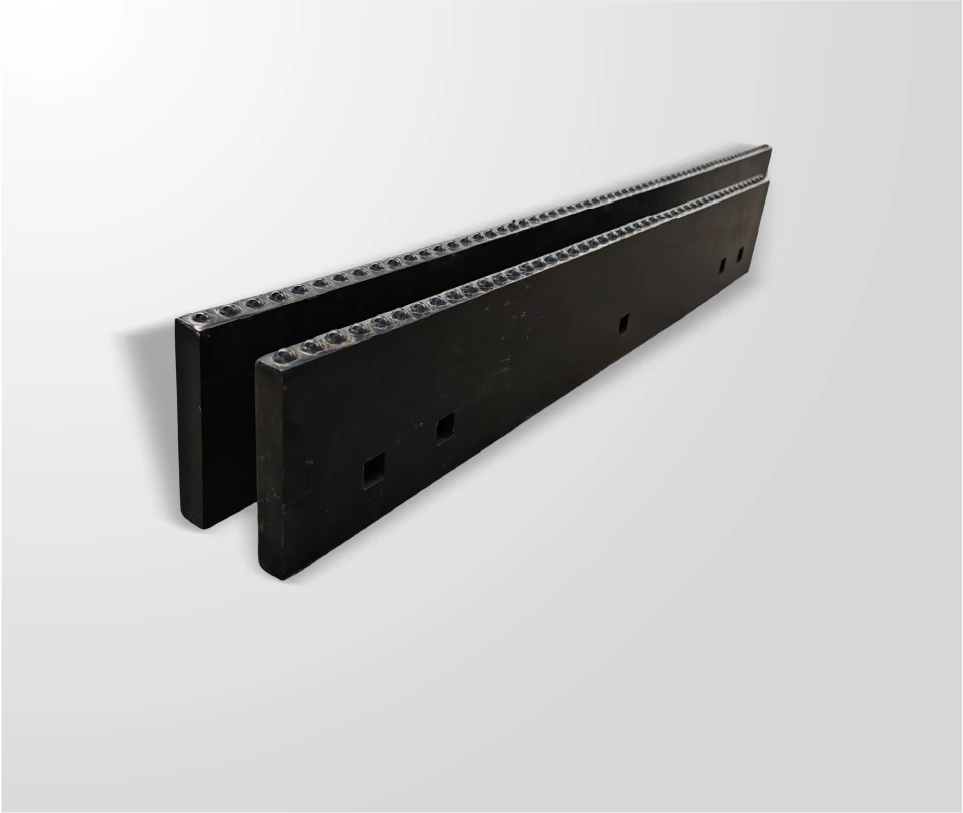
A kit is compatible with a plow when its mounting pattern matches the blade, its arrangement covers the measured installed length and the resulting assembly seats at the height the blade was designed to sit at.
The three conditions are independent, and each can fail separately. A pattern that matches may still belong to a narrower or wider blade, so the arrangement must cover the installed length rather than a nominal figure. A blade whose installed length matches may sit at a different height once a heavier assembly is fitted, which changes the contact angle at the surface. And a kit that satisfies both may still require a different hardware set, which is a compatibility question in its own right.
The measurement discipline behind those checks is set out in the guide to measuring a blade for replacement, and the configuration options are described in the packed ice kit specification guide. Compatibility is decided by the measured blade in service rather than by the make and model in a manual.
How Pattern, Width and Mounting Height Interact
A matching pattern can still produce an unsuitable assembly.
Additional mass at the leading edge changes where the blade meets the surface, so the height at which the assembly sits becomes part of the compatibility question. On some plows that effect is absorbed; on others it requires the shoes or skid settings to be reviewed.
The interaction appears in service rather than at fitting. A kit that mounts correctly but sits at a different height presents its working face differently, and the operator notices it as a change in how the blade behaves on hard surfaces. Because the kit is designed around contact, that difference matters more than it would on a standard edge, and it is the reason a fitment validation should confirm seating height rather than only hole alignment.
Width interacts with pattern through the arrangement. A kit that matches the pattern but covers less than the installed length leaves steel at the ends of the blade, and on a network where the outer sections meet the hardest surfaces, that is where the kit’s advantage is lost. Confirming coverage against the measured installed length rather than the nominal width is what prevents it.
Grade, Geometry and Material Choices Across Makes
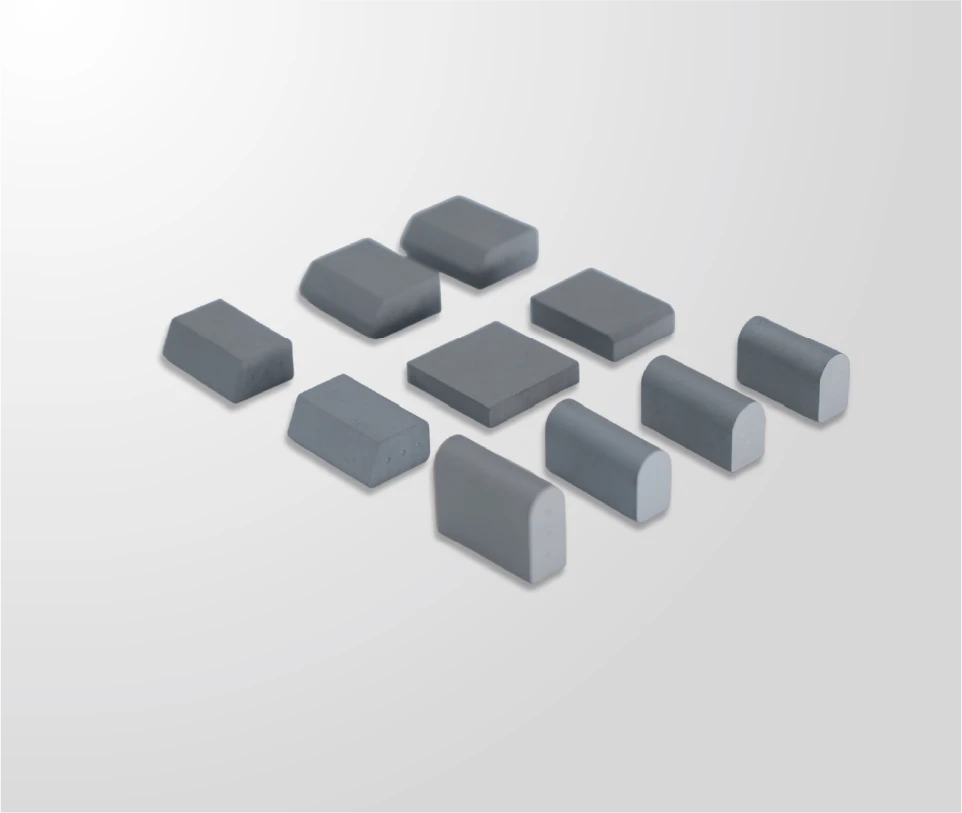
Where a kit is to be used across several plow makes, the grade and arrangement have to suit the most demanding application among them. SENTHAI engineers the hardness and toughness balance against stated service conditions using hardness on the HRA scale together with carbide grain size, and supplies micro grain inserts in trapezoid and bullnose shapes, which allows grade and geometry to be specified together for the surface the kit will work.
Geometry choices interact with the plow class. Where an operator can apply substantial down-pressure, an arrangement that concentrates carbide at the working positions can be used effectively. Where the carrier is lighter, the same arrangement may reduce contact, because the additional mass spreads the available load. That is a compatibility question expressed as a grade or geometry issue, and it is resolved by matching the specification to the plow class rather than by changing the material.
Production control supports cross-make use. SENTHAI manufactures in Rayong, Thailand, in a US-invested plant using non-China raw materials, with the full chain in-house from wet grinding and robotic pressing at up to 500 tons through vacuum and low-pressure sintering, automated high-temperature induction brazing and finishing, holding plus or minus 0.02 mm dimensional tolerances on carbide components so that a kit produced for one pattern is reproducible for the next order.
Fitment and Tolerance Requirements for Each Make
Each plow make should be treated as a separate requirement. SENTHAI validates fitment against AASHTO and DIN bolt patterns before release, with AASHTO published standards as the reference for agency specifications and DIN covering European and export conventions. Where an OEM mounting interface is involved, the equipment documentation is the authority, and SAE standards for mobile machinery describe the interfaces those designs were built around.
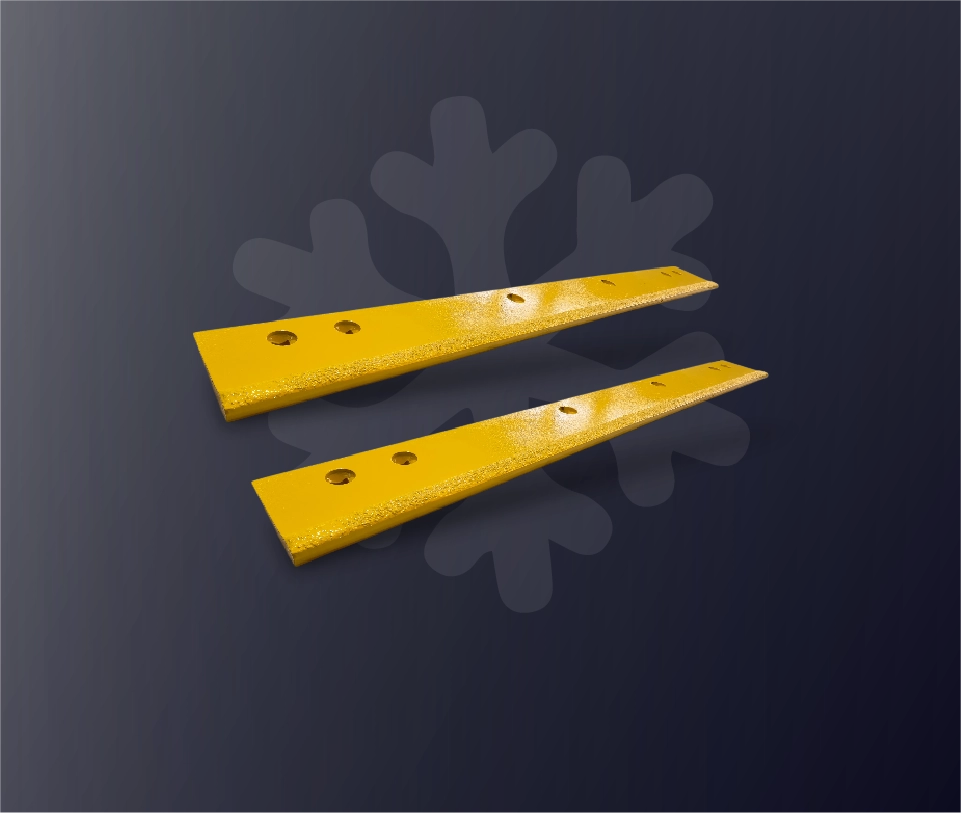
Four checks belong before a kit is specified for a group. Confirm hole diameter, because a nominally identical pattern can differ in hole size between manufacturers. Confirm hole rows, since a two-row blade is not interchangeable with a single-row one even where the outer dimensions agree. Confirm the installed length, so that the arrangement covers the working width. And confirm the seating height and hardware requirement, because a heavier assembly may change the shoes setting and the fasteners.
Where a fleet is consolidating from several configurations to fewer, consolidation should follow those checks rather than precede them. Two makes can share a kit where all four pass; where one does not, keeping the groups separate is cheaper than adapting a kit to fit equipment it was not designed for.
Where the checks show partial compatibility, a written statement of the limitation is worth having even if the specification proceeds. A supplier that confirms the pattern but notes that the seating height should be reviewed on one group has given the fleet something actionable, and the note belongs in the specification record. Compatibility confirmed without qualification across equipment that differs is not evidence; it is an assumption with a signature.
Evidence to Request With the Packed Ice Kit Compatibility Across Makes Quote
Compatibility is verifiable, which makes documentation the fastest way to compare offers. Ask for written confirmation that the arrangement matches the pattern and installed length supplied, the dimensional inspection results for the delivered kit, and the hardware set required including bolt length and torque value. SENTHAI inspects and archives every batch, and the quality control and traceability page describes what that record contains.
Two further items complete the package. Grade data referenced to a test method such as those published by ASTM, and a statement of the pattern standard the kit is produced to. Where the fleet operates several makes, require the confirmation to reference each group rather than the order as a whole, and ask the supplier to state any plow class or mounting face condition for which the offered kit is not recommended.
Where the fleet is publicly funded, supplier registration for federal awards is handled through SAM.gov, and general procurement guidance is published by GSA. Noting those requirements early lets bidders plan rather than discover them after award.

The assembly the arrangement has to fit is described in the material on what a packed ice carbide kit is and how it works.
Common Errors in Packed Ice Kit Compatibility Across Makes and Their Cost
The most common error is assuming that a shared blade width means a shared pattern. Hole diameter and row position vary between manufacturers, and a kit that fits one make may need modification for another. The second is sizing from a nominal width rather than a measured installed length, which leaves the ends of the blade unprotected and reduces the kit’s advantage on exactly the surfaces where it is meant to work.
The third is ignoring the change in seating height. A heavier assembly can alter how the blade meets the surface, and where the shoes setting is not reviewed, the result is a contact change that the fleet attributes to the kit. The fourth is assuming the hardware set transfers, which produces loosening in the first weeks of service and a fitting problem that looks like a product fault.
The costs fall in the same places: fitting time, unplanned hardware work and wear records that cannot be interpreted because two configurations are running without separate records. A measurement exercise covering each group, completed once, removes all four and produces the pattern record the fleet needs for every subsequent order.
A fifth error is subtler and appears when a fleet adds equipment. A plow purchased after the specification was written may share a make with existing units and differ in a detail such as hole spacing or row position. Where the fleet assumes compatibility from the make and model, the new truck becomes the one that does not fit anything in stores. Adding the measured pattern to the fleet record when a unit is acquired, rather than when a kit is ordered, closes that gap.
Writing Compatibility Requirements Into a Tender for Packed Ice Kit Compatibility Across Makes
A tender covering more than one plow make should state the requirement against each. Give the measured pattern, the installed length, the tolerance accepted at the mounting features, the requirement that the arrangement covers the full installed length, and the hardware set required. Then require written compatibility confirmation for each group rather than a single statement for the order.
Where an equivalent is permitted, define the properties and tolerances it must match for each group. Where the programme references published patterns, citing the relevant AASHTO standards keeps offers comparable and gives a receiving inspection a basis for acceptance. One clause is worth adding: require the supplier to state any group for which the offered kit is not recommended, since a negative answer is more informative than a general assurance.
Packed ice kit compatibility is decided by pattern, installed length and seating height, and all three have to be checked for each plow make. A shared nominal width is not evidence of a shared requirement.
Measure each group in service, require written confirmation against each pattern and state the hardware set that follows from it. Done once, that exercise turns a mixed fleet from a compatibility risk into a set of documented groups that can be specified and reviewed separately.
Send SENTHAI the plow makes in the fleet with measured patterns and blade lengths, and the technical team will confirm the kit arrangement, fitment and hardware required for each group.
Frequently Asked Questions
Can one packed ice kit configuration fit several plow makes?
It can where the mounting pattern, installed length and seating height requirements match across the makes, and where the carrier classes can work the additional mass. Those conditions should be confirmed against measured blades rather than catalogue widths. Where one does not hold, keeping the groups on separate configurations is usually cheaper than adapting a kit to equipment it was not designed for.
What measurements are needed for each plow make?
Record the hole diameter, centre-to-centre spacing, number of hole rows, the distance from the top edge to the first row and the installed blade length, taken from a blade in service. Note the plow class and available down-pressure as well. Those readings allow the arrangement to be specified and validated for each group rather than assumed from the model name.
Does a kit change where the blade sits?
It can, because additional mass and section change how the assembly sits on the moldboard. That affects the angle at which the working face meets the surface, which matters more for a contact-led specification than for a standard edge. Confirm seating height when the kit is specified and check whether the shoes or skid settings need reviewing.
What should be recorded when several configurations are in service?
Keep the wear and hardware records separate by group, even where the kits look similar. Once two configurations are running, a difference in result has two possible sources, and separating them afterwards requires reconstructing data that should have been recorded at the time. Record position, measured wear, hardware findings and the specification revision for each group.
Related articles
Packed Ice Kit Storage and Season Prep: Protecting the AssemblyPacked ice carbide kits Packed Ice Kit Cost Model: Building a Programme CasePacked ice carbide kitsPacked Ice Kit Replacement Intervals: Setting Them From EvidencePacked ice carbide kitsIce Control Alternatives Compared: Where Packed Ice Kits FitPacked ice carbide kits