
Isolated Carbide Edged Blade Systems: How They Work on Packed Ice
Isolated carbide edged blade systems explained for buyers: what the design is for, how it differs from a standard edge, and the fitment points to confirm.

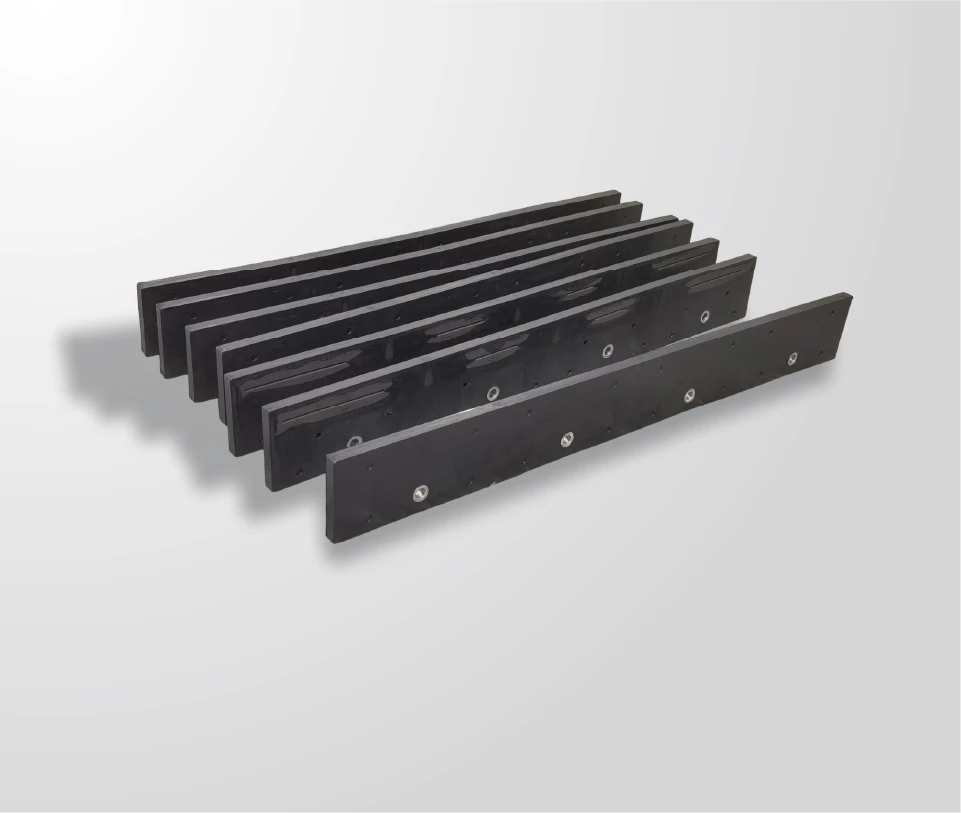
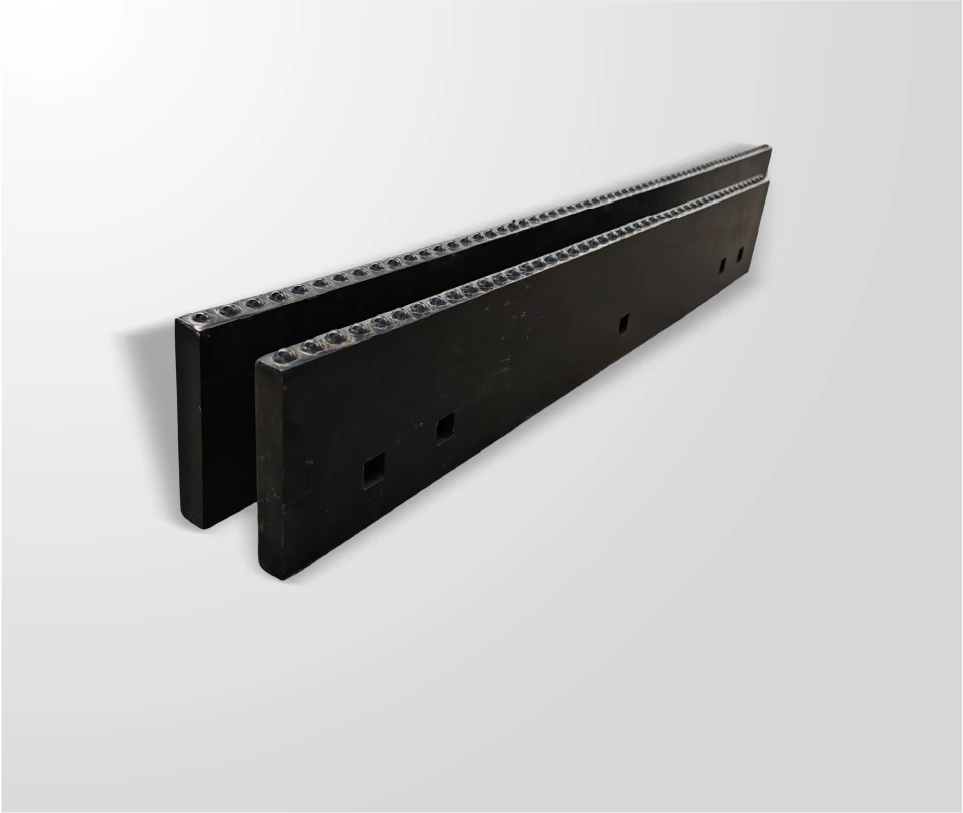
When a route produces bonded, refrozen snow every season, the maintenance argument stops being about edge life and starts being about contact. An isolated carbide edged blade system is designed around that problem: it changes where carbide sits relative to the scraping surface so the edge can work on a hard, uneven layer rather than riding across it. Understanding what the design does is the first step in deciding whether it belongs in a fleet specification.
What an Isolated Carbide Edged Blade Is Designed For
It keeps carbide in contact on hard, uneven surfaces.
A standard edge on refrozen snow skates across the high points, so contact is limited and down-pressure rises. Isolating the carbide changes where that contact is established, working against the refrozen layer instead of relying on edge weight alone.
The design intent follows from what packed ice does to a conventional edge. When the surface is hard enough that the leading edge cannot cut in, the operator compensates with down-pressure and passes, which loads the machine and produces localised wear. Isolating the carbide from the surrounding structure changes how the load path behaves and where contact is established, which is the property the system is built to deliver.
The technical background to the approach is explained on the page covering isolated carbide edged technology, so this article stays with the commercial and operational comparison. What matters to a buyer is that the specification names the condition the system is meant to serve, because a design intended for bonded ice is not automatically the right choice for a route that mostly runs loose, dry snow.
How It Differs From a Standard Edge in Service Life
It changes the wear pattern before it changes the wear rate.
On packed ice a standard edge wears unevenly because contact concentrates on the high points. An isolated carbide edged design spreads contact across the working width, so loss is not concentrated in scallops.
The practical consequence is a maintenance plan that becomes predictable. An edge that wears in a recognisable pattern across its working width can be measured, rotated and retired on a schedule, while an edge that scallops forces decisions on individual sections and often produces a mid-season change. Distribution of wear, rather than the headline interval, is what makes the difference in cost terms.
Service life also depends on what the assembly does between weather events. Packed ice is a seasonal condition on most routes, so the system runs on loose snow and bare pavement for part of its life as well. How it behaves in those conditions determines whether the fleet keeps it fitted all season or exchanges it back to a standard profile, which is a fleet policy decision rather than a product one. Maintenance practice around refrozen surfaces is a recurring topic in pooled research published by Clear Roads.
Surface and Condition Differences on Packed Ice
The condition the system addresses is specific. Bonded, refrozen snow that has been trafficked before it froze presents a hard, polished layer with local high points, and it appears most often on routes carrying traffic between a daytime melt and an overnight freeze. Shaded sections, bridge decks and poorly drained areas hold that layer longest.
Where the layer is broken by abrasives or by traffic, the requirement changes. A surface that has been treated with grit behaves more like an abrasive than like ice, and the wear mechanism shifts toward material loss rather than loss of contact. That distinction is why the same route can behave differently in two consecutive weeks, and why the specification should be based on the dominant condition across a season rather than on a single event.
Treatment practice therefore belongs in the specification discussion. Where a programme relies on liquid de-icing applied ahead of a freeze, surfaces may refreeze into a different state than where dry salt or abrasives are used, and the regulatory context that agencies plan material use against is set out in the EPA’s municipal stormwater guidance. Weather pattern guidance from the National Weather Service is useful when justifying which routes receive the specification first.
Operational Trade-Offs Beyond Wear With Isolated Carbide Edged Blade Systems
The first trade-off is mass and mounting. A system that changes how carbide is positioned at the cutting edge alters the load path into the blade and the moldboard, so the mounting interface has to be confirmed before the change is made. This is a fitment question rather than a performance question, and it is answered by a drawing review rather than by a trial on the fleet.
The second is handling. Any assembly with more carbide content and a different structure weighs more to move and to store, which affects how a workshop handles changes and how edges are racked at season end. Fleets with limited handling equipment should account for that in the changeover plan rather than discovering it in the first week of the season.
The third is consistency of operation. The benefit of the design depends on the edge making contact with the surface, which means operating practice matters: how the blade is set, how much down-pressure is applied and whether the operator trusts the edge to do the work. A fleet that fits the specification and continues to run the same compensating behaviour it used with a standard edge may not see the result it paid for. A fourth consideration is what happens outside ice conditions: packed ice is seasonal on most networks, and the routes that need this specification in January may be running bare pavement in March, so whether the assembly stays fitted or is exchanged with a standard profile is a policy decision that affects handling, storage and the number of units required.
Fitment and Equipment Compatibility for Isolated Carbide Edged Blade Systems
Fitment determines whether the system is even an option. SENTHAI validates fitment against AASHTO and DIN bolt patterns before release and works to plus or minus 0.02 mm dimensional tolerances on carbide components, with AASHTO published standards as the reference for agency specifications and DIN covering European and export conventions. Those checks matter more for a system that changes the load path than for a straight replacement edge.
The practical sequence is to identify the routes, then the carriers, then the patterns. Confirming the pattern means recording hole diameter, centre-to-centre spacing and the distance from the top edge to the first hole row from the blade in service, not from a manual. Where an OEM mounting interface is involved, SAE standards for mobile machinery document the interface the equipment was designed around.
One further compatibility question deserves attention before ordering: whether the blade body and trip mechanism were designed for the additional mass and altered load distribution. A supplier that validates fitment will ask for the blade drawing, and a fleet that supplies it gets a written confirmation instead of an assumption.
Cost Per Metre of Edge Compared Across Isolated Carbide Edged Blade Systems
Cost per metre is the comparison that settles whether the system earns its place. The model structure is set out on the cost per mile page; between a standard edge and an isolated carbide edged system, the inputs move as follows.
| Input | Standard edge on packed ice | Isolated carbide edged system |
|---|---|---|
| Unit or assembly price | Lower entry price | Higher entry price, reflecting additional carbide and structure |
| Wear distribution | Localised scalloping, section-by-section decisions | More consistent working contact across the width |
| Passes per event | More passes accepted because the surface is not breaking | Contact improves, which reduces the incentive to repeat passes |
| Load on machine | Higher down-pressure and more hardware distress | Lower reliance on compensating down-pressure |
| Inspection effort | Frequent, position-specific checks | Scheduled checks with comparable readings across the width |
| Season policy | Fitted throughout | May be exchanged with a standard profile outside ice conditions |
Two cautions belong with the comparison. The first is that a fleet which does not record passes and down-pressure cannot model the saving that comes from better contact, and the argument then rests only on the parts line, where the standard edge looks cheaper. The second is that the cost of a specification that goes unused on a mild winter is real; where a route sees bonded ice only in exceptional years, the money is better spent on the routes that see it every season.

Fitting the System Into a Fleet Programme
The system fits where packed ice is a recurring seasonal condition rather than an occasional event, and where the routes affected are known. Those are the routes that generate repeated passes, elevated down-pressure and hardware maintenance, and they are usually identifiable from a season of operator reports and inspection records.
A useful approach is to fit the specification to the worst-affected routes first and to keep the standard profile elsewhere, then compare wear records and operating feedback after a season. That produces an evidence base for the next purchasing decision and avoids committing the whole fleet to a design that suits only part of the network.
Two records make that review possible. The first is a short route profile for each truck in the trial, covering surface mix, gradient, traffic exposure and how often the route holds refrozen snow. The second is a maintenance log capturing passes per event, measured edge height at fixed points and any hardware intervention. Together they answer the question a purchasing decision actually needs: did the routes selected for the specification behave differently from the routes that kept the standard edge? Where a fleet operates across several jurisdictions, the answer can differ between them even for similar-looking roads, because treatment practice and traffic patterns change the surface.
An isolated carbide edged blade system addresses a specific failure: loss of contact on hard, refrozen surfaces. Its value shows up first in how wear is distributed across the working width and only later in any single interval figure.
Deciding well means naming the routes, confirming the patterns and the mounting interface in writing, and reviewing the result against recorded passes and wear data after a season. Handled that way, the specification is either justified by evidence or retired before it becomes an assumption.
Send SENTHAI the routes where packed ice recurs and the blade drawings for the carriers involved, and the technical team will review fitment, load path and the specification for each group.
Frequently Asked Questions
Is an isolated carbide edged blade suitable for all winter routes?
No. It addresses a specific condition: bonded, refrozen snow that a standard edge cannot cut into. On routes that mostly run loose, dry snow, a conventional carbide edge usually performs well at a lower entry price. The specification should follow the routes where the condition recurs, which is normally a subset of the network rather than the whole fleet.
Does the system require a different mounting pattern?
The mounting pattern is set by the equipment, so it does not change with the edge specification. What can change is the load carried through that pattern, because the assembly is heavier and distributes load differently. Confirm the pattern, the condition of the mounting holes and the hardware set with the supplier before the order, and request written fitment confirmation.
How do I measure whether it made a difference?
Record the same inputs before and after: measured edge height at fixed reference points, the positions of localised loss, hardware torque checks, the number of passes per event and operator feedback on contact. Wear distribution across the working width is the first indicator, because scalloping is the visible symptom of contact loss. Compare over a full season rather than a single storm.
Can it be used alongside standard edges in the same fleet?
Yes, and running both is a practical way to test the case. Keep the two specifications separate in the stores system and in the inspection records, so that readings from each can be compared without mixing conditions. Where a fleet runs both, the review at season end shows whether the routes selected for the specification were the right ones.