
JOMA Blade Compatibility Across Plow Brands
JOMA blade compatibility across plow brands: how brand differences appear at the mounting interface and how to verify fitment group by group.

Brand is a convenient way to organise a fleet and a poor way to specify a blade. Two trucks from the same manufacturer can carry different mounting patterns across model years, and a machine that has been repaired or refitted may no longer match its original drawing. Compatibility has to be established at the mounting interface, which is measured rather than looked up.
Which JOMA Blade Compatibility Points Decide Fitment
Pattern, arrangement and seated height decide it.
A blade is compatible with a plow when its mounting pattern matches the measured blade, its segment arrangement covers the installed length, and the assembly seats at the height the moldboard was designed for.
The three conditions are checked separately because each can fail on its own. A pattern that matches may belong to a different blade width, so the arrangement must cover the measured installed length rather than a nominal one. A blade whose length matches may sit differently once a different assembly is fitted, which changes how the working face meets the surface. And a compatible pattern and length may still require a different hardware set.
The measurement procedure behind the checks is set out in the guide to measuring a blade for replacement, and the mounting discipline is covered in the JOMA style compatibility guide. Both start from the blade in service rather than from the equipment documentation.
How Brand Differences Appear at the Mounting Interface
Differences appear in four places at the interface.
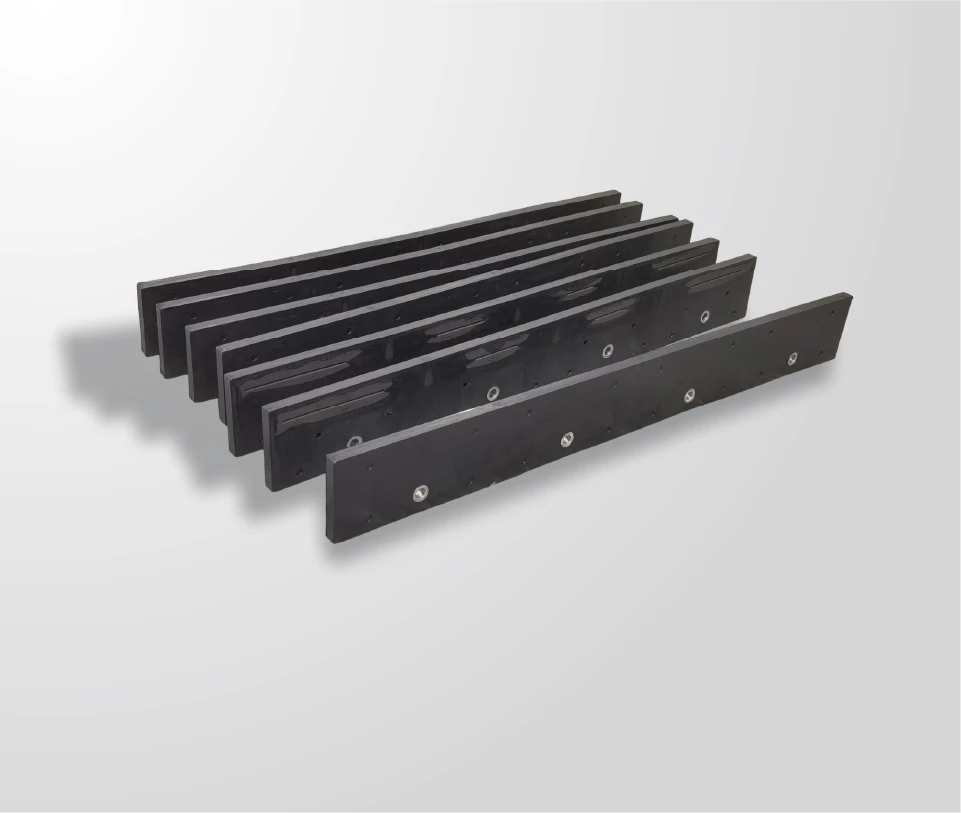
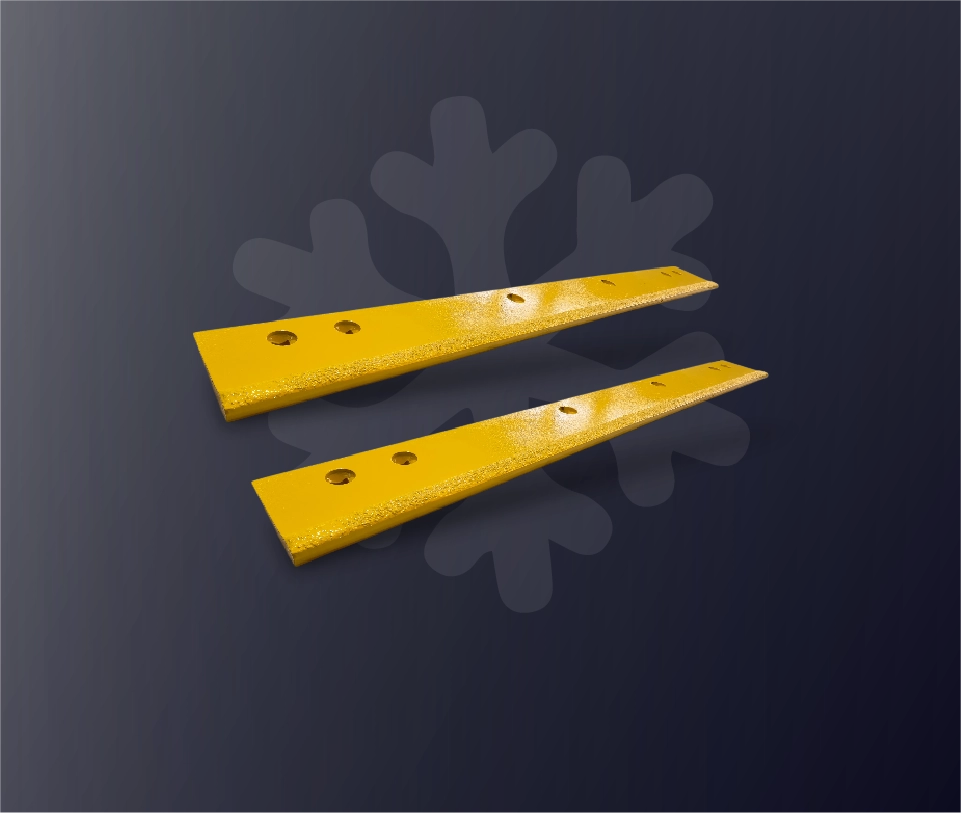
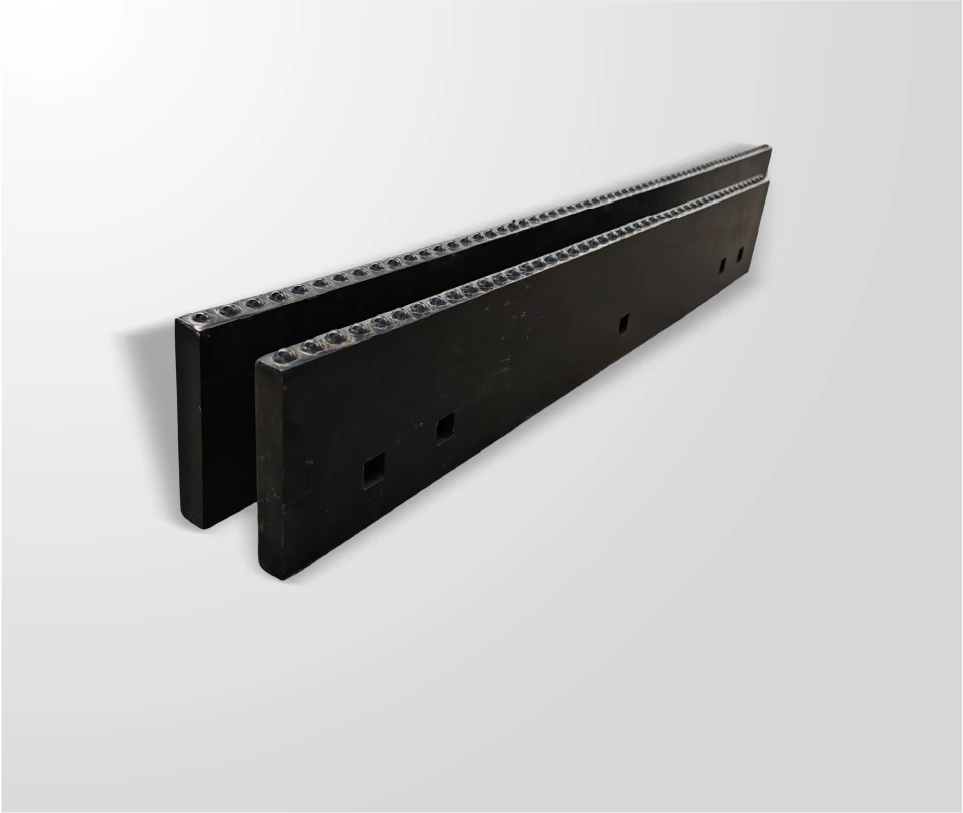
Hole diameter varies, and a pattern that matches on spacing can still be wrong on diameter. Row position varies, which changes seated height and the angle of the working face. Row count varies, so a two-row blade is not interchangeable with a single-row pattern. And installed length varies for a given width, which changes the arrangement.
Variation within a brand is as important as variation between brands. Model years change interfaces, aftermarket moldboards may not follow the original drawing, and a machine that has run several edge generations may carry worn or dressed holes. Where a fleet standardises on brand rather than measurement, the exceptions are discovered one at a time, usually during fitting in the first week of a season.
A practical approach is to treat each truck as its own requirement until measurements show that groups genuinely share a pattern. Grouping follows measurement rather than assumption, and the resulting groups are the units that specifications, spares holdings and records should use.
Two further factors produce exceptions within a brand. Repair work on a moldboard can change hole positions or leave a face that is no longer flat along its length, and a fleet that has replaced edges from several sources over the years may be running a mixture of patterns without knowing it. Both are visible from measurement and invisible from a fleet list, which is why the measurement exercise is the starting point rather than a follow-up step.
The record that comes out of that exercise has a second use. When a truck is retired or transferred, its pattern record tells the fleet whether the blades held for it can be reallocated to a remaining group or should be disposed of. Without the record, the blades follow the truck out of the fleet, and the replacement truck is specified from scratch.
Grade, Geometry and Material Choices Across Brands
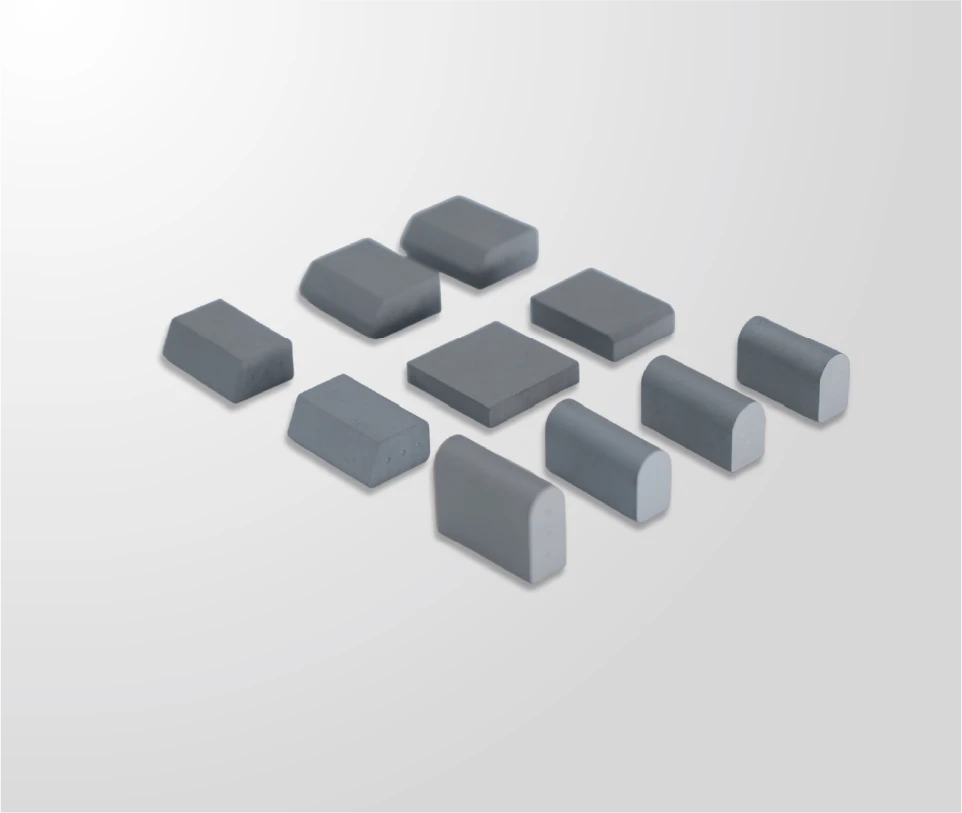
Where a blade is used across several brands, the specification has to suit the range rather than the average. SENTHAI engineers the hardness and toughness balance against stated service conditions using hardness on the HRA scale together with carbide grain size, and supplies micro grain inserts in trapezoid and bullnose shapes. Where brands differ in carrier class or route assignment, the grade that suits one group may be inadequate for another, and standardising across both on a single grade introduces a compromise.
Geometry interacts with the mounting interface in the same way. Additional mass at the leading edge is carried through the same number of fixing positions, so a heavier assembly on a pattern with fewer positions raises the load at each fastener. That is a compatibility question expressed as a mounting question, and it is resolved by confirming the assembly against the equipment rather than by changing the material.
Production control supports cross-brand use. SENTHAI manufactures in Rayong, Thailand, in a US-invested plant using non-China raw materials, with the full chain in-house from wet grinding and robotic pressing at up to 500 tons through vacuum and low-pressure sintering, automated high-temperature induction brazing and finishing. Holding plus or minus 0.02 mm dimensional tolerances on carbide components means a blade produced for one group is reproducible for the next order rather than approximating the drawing.
Fitment and Tolerance Requirements for Each Brand
Each brand and, where the measurements differ, each truck group should be treated as its own requirement. SENTHAI validates fitment against AASHTO and DIN bolt patterns before release, with AASHTO published standards as the reference for agency specifications and DIN covering European and export conventions. Where an OEM mounting interface is involved, the equipment documentation is the authority, and SAE standards for mobile machinery describe the interfaces those designs were built around.
Four checks belong before a blade is specified for a group. Confirm hole diameter and row position from the blade in service. Confirm the installed length so the arrangement covers the working width. Confirm the mounting face is flat and its holes are within tolerance. And confirm the hardware set, because a heavier or differently configured assembly may need different fasteners. Where any of the four is uncertain, written confirmation from the supplier against the measured dimensions is the item that prevents a fitting problem.
Where a fleet is consolidating configurations, consolidation should follow those checks rather than precede them. Groups that pass all four can share a specification; groups that do not are cheaper to keep separate than to adapt, because adapting a flexible blade to a pattern it was not designed for changes how it deflects and therefore how it works.
Evidence to Request With the JOMA Blade Compatibility Across Brands Quote
Ask for written confirmation that the blade matches the pattern and installed length supplied, the dimensional inspection results at the mounting holes, and the hardware set required including bolt length and torque value. SENTHAI inspects and archives every batch, and the quality control and traceability page describes what that record contains.
Two further items complete the package. Grade data referenced to a test method such as those published by ASTM, and a statement of the pattern standard the blade is produced to. Where the fleet is publicly funded, supplier registration for federal awards is handled through SAM.gov, and general procurement guidance is published by GSA.

Common Errors in JOMA Blade Compatibility Across Brands and Their Cost
The most common error is specifying by brand and model. It works until a model-year change, a repair or an aftermarket moldboard makes one truck an exception, and the exception is found during fitting. The second is consolidating before measuring, which produces a specification that suits the majority of trucks and fails on the rest.
The third is ignoring seated height. A blade that mounts correctly but sits differently changes the angle at which the working face meets the surface, and on a flexible blade that affects deflection behaviour as well as contact. The fourth is assuming hardware transfers between groups, which produces loosening in the first weeks of service and a fitting problem that looks like a product fault.
The costs fall in familiar places: fitting time, unplanned hardware work and wear records that cannot be interpreted because two configurations are in service without separate records. A measurement exercise covering each truck, completed once, removes all four and produces the grouping that every future order depends on.
A fifth error is specific to flexible blades and worth stating separately: fitting a segment that is correct on the pattern but wrong for the assembly’s arrangement. Because a segmented blade is located by several positions rather than two, a segment intended for one arrangement can mount on another and still leave a working face that does not match its neighbours. The result is uneven deflection and wear concentrated at the joints, which is then attributed to the material.
A sixth error is the quietest: not updating the pattern record after a change. Where a moldboard is repaired, holes are dressed or a segment is replaced with a different specification, the record has to move with the machine. A record that describes a previous state is worse than no record, because it is trusted.
Writing Brand Compatibility Into a Tender
A tender covering several brands should state the requirement against measured groups rather than manufacturer names. Give the measured pattern dimensions, the installed length, the tolerance accepted at the mounting features, the requirement that the assembly seats flat without force, and the hardware set required. Then require written compatibility confirmation for each group rather than a single statement for the order.
Where an equivalent is permitted, define the properties and tolerances it must match for each group. Where the programme references published patterns, citing the relevant AASHTO standards keeps offers comparable. One clause is worth adding: require the supplier to state any group for which the offered blade is not recommended, since a specific negative answer is more useful than a general assurance of compatibility.
JOMA blade compatibility is decided by pattern, arrangement and seated height, and each has to be confirmed against the blade in service. A brand reference describes what the equipment was, not what it is now.
Measure each truck, group it on what the measurements show, and require written confirmation against each group. Done once, that work turns a mixed fleet into documented groups that can be specified, stocked and reviewed without repeated fitment surprises.
Send SENTHAI your plow list with measured patterns and blade lengths, and the technical team will confirm the blade arrangement, fitment and hardware required for each group.
Frequently Asked Questions
Can a JOMA style blade fit several plow brands?
It can where the measured pattern, installed length and seated height requirements match, and where the carrier can work the assembly on ice or rough routes. Those conditions should be confirmed from the blades in service rather than from manufacturers’ documentation, because model years, repairs and aftermarket moldboards all change the interface. Where a group does not match, keeping it separate is cheaper than adapting.
What should be measured on each truck?
Record hole diameter, centre-to-centre spacing, the number of hole rows, the distance from the top edge to the first row and the installed blade length, all taken from the blade in service. Note the mounting face condition and the plow class as well. Those readings are what allow a blade to be specified for the group and a delivery to be checked on receipt.
Does seated height really affect performance?
Yes. The height at which the assembly sits determines the angle at which the working face meets the surface, which affects contact and, on a flexible blade, how the assembly deflects. A blade that mounts correctly but sits differently will behave differently, and that difference is easy to attribute to the product rather than to the fitment.
How should records be kept where several brands are in service?
Keep wear and hardware records by measured group rather than by brand. Once two configurations are running, a difference in result has two possible sources, and separating them afterwards requires reconstructing data that should have been recorded at the time. Record position, measured wear and hardware findings for each group separately.

