
Brazing Carbide Inserts: Surface Prep, Cobalt, and Bond Strength
Brazing starts with the surface, not the torch. The bond between a carbide insert and its steel carrier is decided before the heat is applied: by the cleanliness of the surface, the cobalt that…
Brazing starts with the surface, not the torch. The bond between a carbide insert and its steel carrier is decided before the heat is applied: by the cleanliness of the surface, the cobalt that is exposed, and the wetting of the alloy. A manufacturer that controls the surface controls the bond, and a manufacturer that skips the surface is building a joint that will fail under load.
This article is the brazing deep dive for manufacturers and buyers: the surface preparation, the cobalt-rich layer, wetting and alloy flow, the defects to prevent, and the testing that verifies the bond.
Brazing starts with the surface
Brazing joins the carbide to the steel with a filler alloy that melts and bonds to both surfaces. The quality of the bond depends on the alloy wetting the surfaces, and wetting depends on the surfaces being clean and active.
A contaminated surface, one carrying oils, mold release agents, oxides, or processing residues, will not wet properly. The alloy beads up instead of spreading, the joint is incomplete, and the insert that looks seated is held by a fraction of the bond it needs.
That is why the surface preparation is the first step of brazing, and why manufacturers like SENTHAI describe it as part of the process rather than a detail before it.
The surface story also explains why the same insert can braze well in one factory and poorly in another: the preparation, not the insert alone, decides the wetting. An insert engineered for brazing, with the surface conditioned and the cobalt exposed, gives the factory the best possible starting point, which is why the insert specification and the brazing process are designed together.
The buyer’s question, then, is not just “can you braze” but “what is your surface preparation and how do you verify it.” The answer, with the records behind it, is the difference between a joint that holds and a pop-out waiting for the first impact.
The verification of the preparation belongs in the batch record: the sandblasting parameters, the surface condition check, and the inspection of the brazed joints. A buyer who sees the preparation in the record and the joint in the sample has the evidence the process needs.
The same evidence supports the incoming QC on the buyer’s side. If the inserts arrive with the brazing surface documented, the receiving check can confirm the surface condition and file the record with the lot. The documentation travels with the part, which is what makes the brazing chain verifiable end to end.
The chain also has a maintenance endpoint: the bond’s performance in the field is the final evidence, and the fleet that records the insert losses and the bond failures closes the loop between the process and the route. A pop-out in the field is a finding for the brazing chain, not just a part failure.
The closed loop is what makes the brazing process a managed system: the surface preparation, the alloy, the temperature, the inspection, and the field record are one chain, and the buyer who verifies the chain at every link gets a bond that can be trusted. The chain is the specification.
And the specification, verified at every link, is what keeps the inserts in the blade and the blade on the road.
The road is where the bond is finally judged.
And the road is the buyer’s test as well.
The test, run each season, is the verdict.
The verdict is the bond’s long-term report.
The report is written on the road.
The road keeps the score.
The score is the bond’s.
And the bond is the blade’s.
What is the difference between brazing and welding here? Brazing joins the carbide to the steel with a filler alloy at a temperature below the melting point of the base materials; welding melts the base materials themselves. The terms are not interchangeable, and the process names should be used precisely in the specification.
What is the most common brazing defect? The cold joint: a partial bond from poor wetting or incomplete fill. It looks seated, passes a glance, and fails under the first serious impact, which is why the inspection goes beyond the visual.
Sandblasting and the cobalt-rich layer
The surface preparation that SENTHAI describes is precision sandblasting: cleaning the insert surface and exposing a cobalt-rich layer that the brazing alloy can wet.
The mechanism matters. Carbide is a composite of tungsten carbide grains and a cobalt binder, and the brazing alloy bonds best to the cobalt-rich surface. Sandblasting removes the contamination and the surface layer that would block the bond, exposing the cobalt that the alloy wants to wet.
The preparation has to be precise, not aggressive: enough to clean and expose, not so much that it damages the carbide or alters the dimensions. The precision is part of the process control, and the batch record should show it.
How do wetting and alloy flow affect bond strength?
Wetting is the alloy’s ability to spread across the surface and bond at the atomic level. The better the wetting, the more complete the joint, and the stronger the bond.
The alloy flow follows the wetting: a well-wetted joint fills the interface evenly, while a poorly wetted one leaves voids where the load concentrates. The void is a crack waiting for an impact.
The factors that control wetting and flow:
- The surface cleanliness and the exposed cobalt;
- The alloy composition and its compatibility with the carbide and the steel;
- The temperature and the heating rate, which control the alloy’s flow;
- The joint clearance, which the alloy must fill;
- The atmosphere and the flux, which protect the surfaces during brazing.
Each factor is a process parameter, and the process parameters are what the manufacturer controls and the buyer verifies.
How do you prevent cold joints and pop-outs?
A cold joint is a partial bond: the alloy did not fully wet or fill, so the insert is seated but weakly attached. The pop-out is the cold joint failing under load.
The prevention:
| Control | What it prevents |
|---|---|
| Surface preparation | Gives the alloy a clean, cobalt-rich surface to wet |
| Temperature and heating rate | Lets the alloy flow and fill the joint |
| Correct alloy selection | Matches the carbide and the steel |
| Joint inspection | Catches bonds that a visual check would miss |
| Sample bond verification | Confirms the bond with the method the application requires |
SENTHAI describes its brazing technology as engineered to withstand high-velocity impacts, which is the claim behind the retention. The claim is verified by the process control and the inspection, and the buyer should ask for both.
Testing bonds before production
The bond testing is the evidence the process works:
- Dimensional and visual inspection of the brazed joint;
- Destructive sampling where the application allows, to confirm the joint filled;
- Non-destructive methods, where specified, for the critical applications;
- Batch records that tie the brazing parameters to the shipped product;
- Field performance, which is the final test on the actual route.
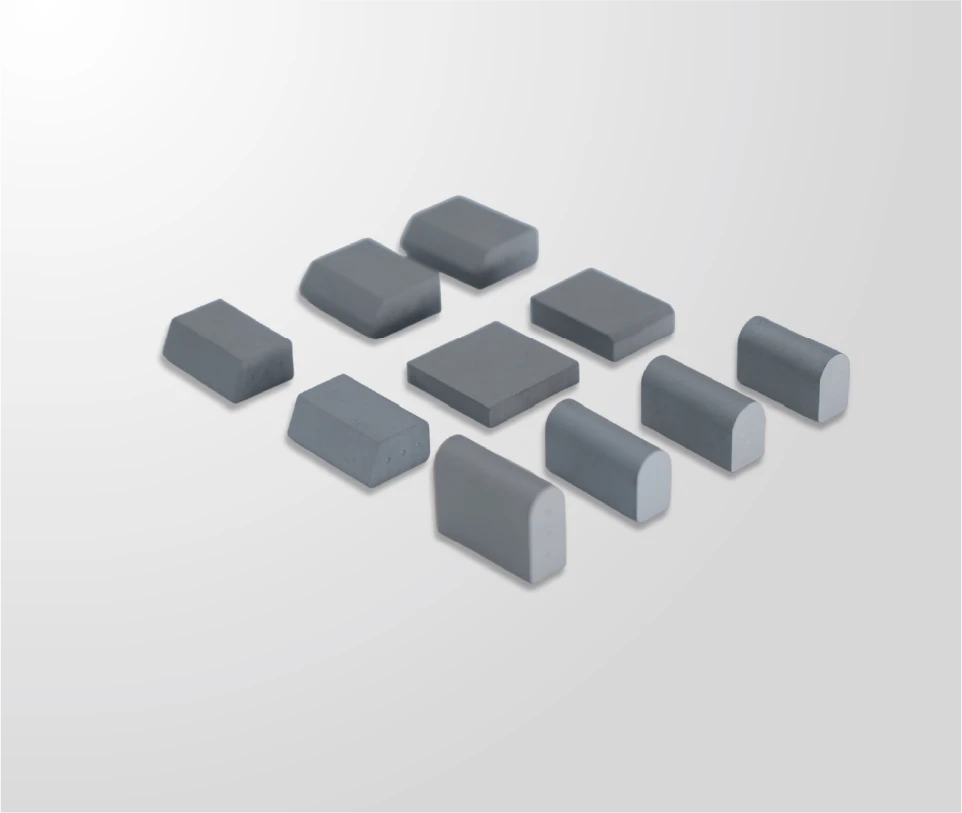
SENTHAI states that sample blades can be arranged for field testing, which is the validation that the bond holds under real impact. The carbide inserts page covers the insert side of the joint, and the JOMA-style blade page shows the segmented system that depends on it.
Source inserts engineered for brazing
For an OEM or a blade manufacturer, the inserts themselves should be engineered for brazing: the surface preparation, the cobalt exposure, and the dimensional consistency are part of the insert specification, not the blade assembly’s problem.
Send the brazing process, the joint requirements, and the acceptance criteria through the contact page and ask for the insert specification and the batch records. The bond starts with the surface, and the surface starts with the insert.
Expert view — SENTHAI engineering team: “The bond starts on the surface, not in the flame. The preparation is the joint’s first decision.”
Frequently Asked Questions
Why does the surface matter in brazing? The alloy can only wet a clean, active surface. Contamination blocks the wetting, and a poorly wetted joint is a weak bond.
What is the cobalt-rich layer? The cobalt binder exposed at the carbide’s surface, which the brazing alloy bonds to best. Sandblasting cleans and exposes it.
What is a cold joint? A partial bond where the alloy did not fully wet or fill the joint. The insert looks seated but is weakly attached, and the pop-out follows.
How do I prevent pop-outs? Control the surface preparation, the temperature, and the alloy, inspect the joints with defined acceptance criteria, and verify with samples.
What testing verifies the bond? Dimensional and visual inspection, destructive or non-destructive testing where specified, batch records, and field performance.
Does SENTHAI describe its brazing process? SENTHAI describes precision sandblasting and brazing technology engineered for high-velocity impacts; verify the process and the records per order.
What should I ask for an insert brazing specification? The surface preparation, the alloy and process parameters, the acceptance criteria, the inspection method, and the batch records.
Sources
Related articles
 Best Snow Plow Blade Family for Your Fleet: Top 5 ScenariosKnowledgeTop 10 Snow Plow Blade Types for Winter Fleets (Ranked by Duty Fit)Knowledge
 Top 5 Best Carbide Blade Configurations for Highway PlowingKnowledge
 Best Snow Plow Blade Materials Ranked: Steel vs Carbide vs Cladding vs Rubber-CarbideKnowledge