
Brazed vs. Mechanically Retained Inserts: Choosing a Retention System
Retention is a system decision, not a preference. The way an insert is held in its carrier decides how the blade handles impact, how the insert is replaced, and how the maintenance program works.…
Retention is a system decision, not a preference. The way an insert is held in its carrier decides how the blade handles impact, how the insert is replaced, and how the maintenance program works. Brazed retention and mechanical retention both have real strengths, and choosing between them means matching the retention to the blade design and the maintenance model, not picking the “newer” method.
This article compares brazed and mechanically retained inserts across strength, serviceability, and cost, and explains how to choose for a given blade design.
Retention is a system decision
The insert is the working edge, and the retention is the interface between the insert and the carrier. The interface decides three things: how the impact load transfers, how the insert is serviced when it wears, and what the blade costs to maintain over its life.
The decision belongs to the design stage, because the retention method changes the carrier geometry, the manufacturing process, and the maintenance plan. A blade designed for brazed inserts is not a blade that should be switched to mechanical retention in the field, and vice versa.
The buyer’s question is not which method is better; it is which method fits the blade’s duty and the fleet’s maintenance model.
The decision also has a quality dimension that is easy to miss: the retention method determines what the incoming inspection checks. A brazed blade is verified on the bond, with brazing and joint checks; a mechanical blade is verified on the interface, with fit and lock checks. The fleet’s inspection routine has to match the retention, which is another reason the choice belongs in the specification rather than the field.
The supplier’s process control also differs between the two: brazing requires the surface preparation and temperature control that SENTHAI describes, while mechanical retention requires the machining accuracy of the pocket and the consistency of the hardware. The qualification conversation should cover whichever process the chosen system depends on.
The choice also shapes the spare-parts plan. A brazed system needs section-level stock and a re-tip path; a mechanical system needs inserts and hardware, with the carriers in circulation. The fleet’s warehouse is designed around the retention method, which is one more reason the decision belongs early, before the stock plan is written.
The field inspection routine follows the same logic: the brazed system is checked on the bond, and the mechanical system is checked on the interface and the lock. The maintenance manual has to match the retention, and the training has to teach the difference.
How does brazed retention work?
Brazed retention bonds the carbide insert to the steel carrier with a brazing alloy, forming a metallurgical joint. The insert becomes part of the carrier, with the bond transferring load across the full interface.
The strengths of brazing:
- Strong, continuous load transfer across the joint;
- A low-profile edge, because there is no mechanical hardware at the cutting face;
- Proven performance in impact-heavy blade duty, which is why SENTHAI describes its brazing technology as engineered to withstand high-velocity impacts;
- A clean design that suits segmented and continuous-edge blades alike.
The trade-off is serviceability: a brazed insert is not designed for field removal, so the replacement happens at the section level, or through a controlled re-tipping process at the factory.
How mechanical retention works
Mechanical retention holds the insert in the carrier with a mechanical interface: a pocket, a clamp, a screw, or a wedge that locks the insert in place without a permanent bond.
The strengths of mechanical retention:
- Field serviceability: a worn insert can be replaced without a brazing operation;
- No thermal cycle in assembly, which avoids the brazing heat and its effects on the material;
- Component-level replacement, which can simplify the spare parts stock;
- Reuse of the carrier across multiple insert cycles.
The trade-offs are the hardware at the interface, the potential for loosening under vibration, and the design constraints the mechanical pocket places on the edge profile.
How do the systems compare on strength, serviceability, and cost?
The comparison is a table of trade-offs:
| Factor | Brazed retention | Mechanical retention |
|---|---|---|
| Load transfer | Continuous across the bond | Through the mechanical interface |
| Impact behavior | Proven in heavy blade duty | Depends on the lock design |
| Serviceability | Section replacement or factory re-tip | Field insert replacement |
| Assembly | Brazing process, controlled heat | Mechanical assembly, no heat |
| Edge profile | Low-profile, clean | Interface hardware may constrain profile |
| Carrier reuse | Limited by re-tip feasibility | Designed for multiple insert cycles |
| Cost per cycle | Lower insert cost, section-level change | Higher hardware, component-level change |
Neither column wins outright. The brazed system suits impact-heavy duty where the bond’s continuous load transfer matters; the mechanical system suits operations that need field serviceability and carrier reuse.
The cost comparison should also include the full lifecycle, not the first cycle. A brazed blade is replaced at the section level, and its cost per season is the section price divided by the sections used; a mechanical system spreads the carrier cost across the insert cycles, and its cost per season includes the hardware and the insert replacements. The fleet’s changeout data is the input that makes the comparison real.
The lifecycle comparison should also include the downtime cost of the changeout method. If the mechanical system’s field serviceability saves a shop visit per changeout, that saving belongs in the comparison; if the brazed system’s section changeout is faster and simpler, that belongs on its side. The maintenance model, not the invoice, decides which retention is cheaper to run.
The comparison should be revisited when the fleet’s maintenance model changes, because the retention that fits a shop-based operation may not fit a field-service operation. The decision is a living one, and the review is part of the season cycle.
The final confirmation belongs on the drawing: the retention, the carrier, and the replacement plan are all part of the specification, and the manufacturer’s confirmation closes the decision.
The closed decision is the one the maintenance plan can follow.
The plan, matching the retention, is the system working.
The system, verified at the dock and in the shop, is the whole decision.
Can a fleet run both retention systems? Yes, and mixed fleets often do: brazed blades for impact-heavy duty and mechanical systems where field serviceability matters. The retention is specified per blade family, and the maintenance plan follows the system.
Choosing for your blade design
The choice follows the blade design and the maintenance model:
- Impact-heavy blade duty favors brazed retention, where the continuous bond and the proven impact performance matter most;
- High-changeout operations favor mechanical retention, where field replacement saves downtime;
- Carrier-heavy designs favor mechanical retention, where the carrier is designed for reuse;
- Segmented and ice-breaking systems, where the bond is part of the structure, favor brazed construction;
- Mixed fleets may run both, with the retention matched per blade family.
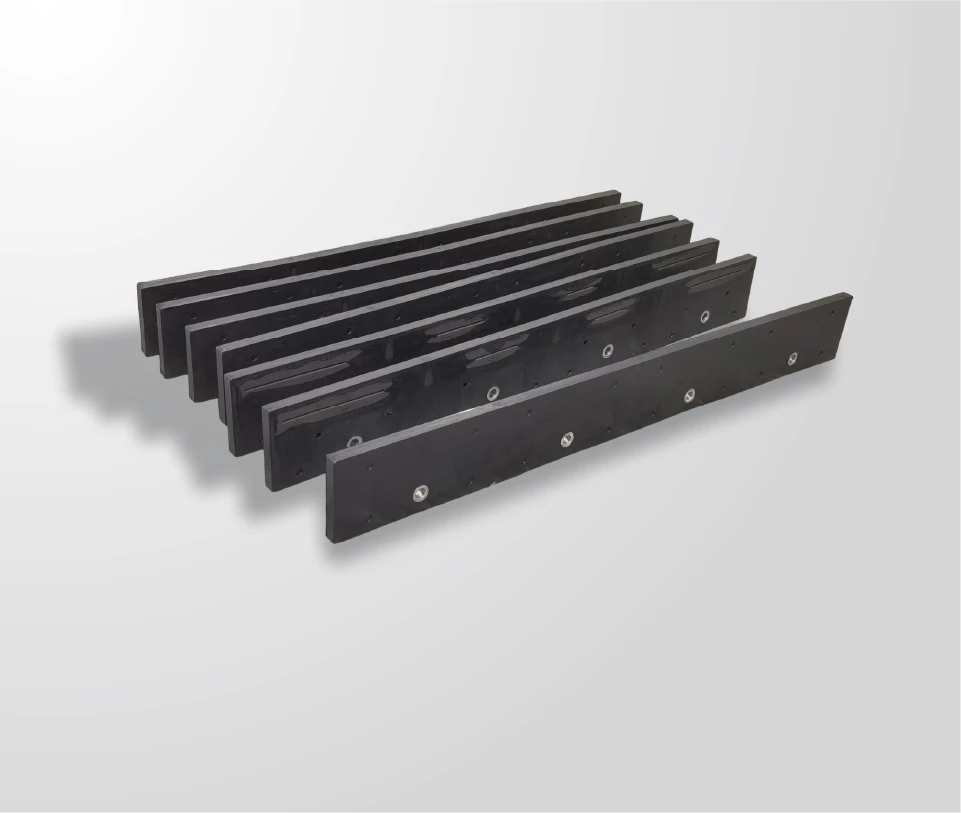
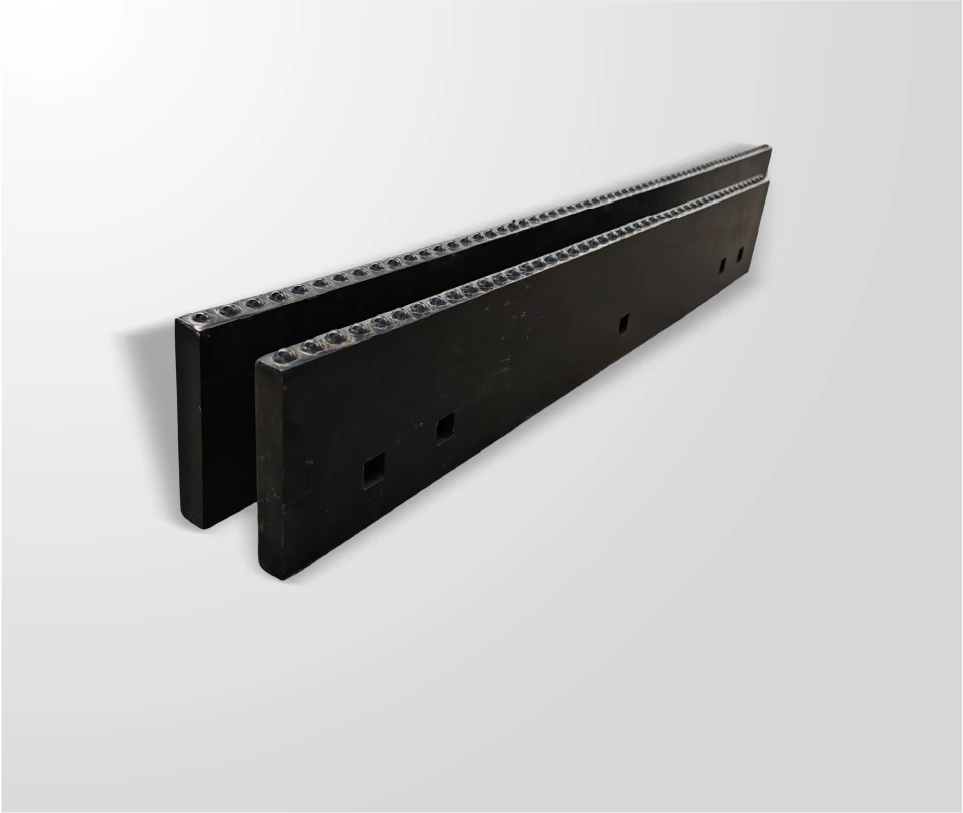
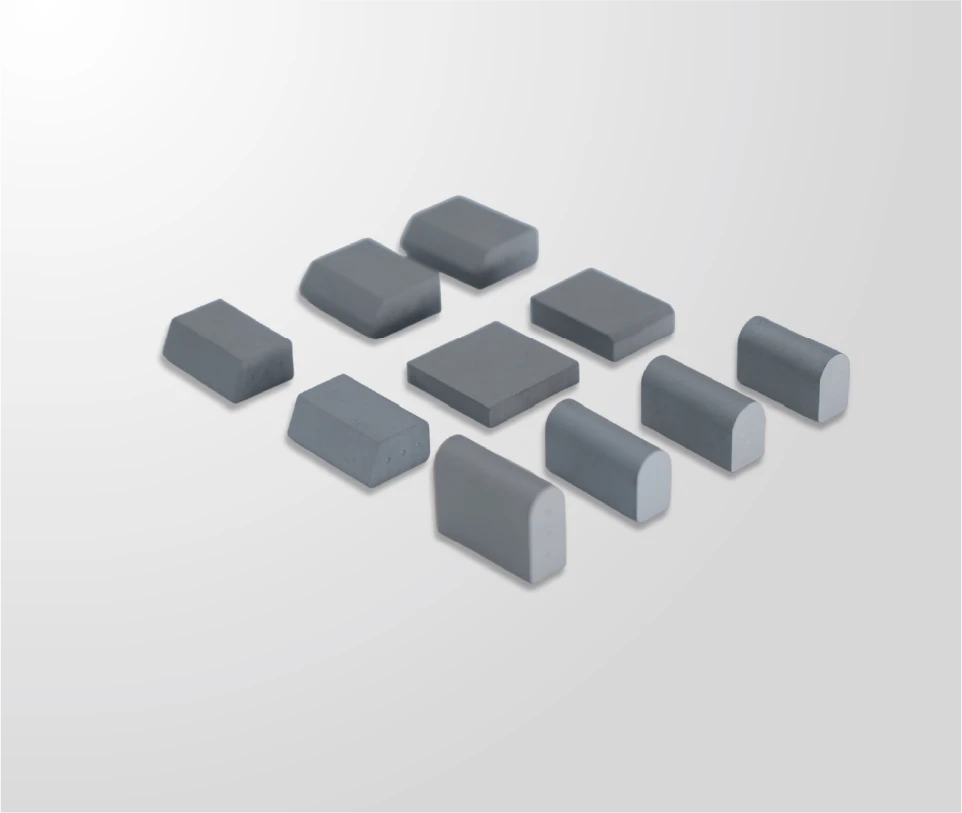
SENTHAI’s carbide inserts page covers the insert side of the brazed system, and the carbide snow plow blade page shows the brazed construction in the blade family. The design conversation decides which retention belongs where.
Match retention to your maintenance model
The maintenance model is the deciding input. A fleet with a well-equipped shop and a preference for field serviceability may choose mechanical retention for the applications where it fits; a fleet that runs impact-heavy duty and plans section-level replacement will find the brazed system the better match.
To make the choice, define the duty, the changeout model, and the shop capability, then confirm the retention and the replacement plan with the manufacturer. SENTHAI’s engineering team can confirm the configuration through the contact page, and the decision is documented in the specification so the maintenance plan matches the design.
Expert view — SENTHAI engineering team: “Retention is a system decision, not a preference. The brazed bond and the mechanical lock serve different seasons.”
Frequently Asked Questions
What is the difference between brazed and mechanical retention? Brazed retention bonds the insert to the carrier with a brazing alloy; mechanical retention holds it with a pocket, clamp, screw, or wedge.
Which is stronger? Both can be engineered for the duty. Brazed retention gives continuous load transfer and proven impact performance; mechanical retention depends on the lock design.
Which is easier to service? Mechanical retention allows field insert replacement; brazed inserts are replaced at the section level or through a factory re-tip.
Does mechanical retention cost more? The hardware adds cost per insert, but the carrier can be reused across cycles. The cost comparison depends on the changeout model.
Can a blade be switched between retention systems? No. The carrier geometry and the manufacturing process are designed for one method, so the choice belongs at the design stage.
Which retention suits impact-heavy duty? Brazed retention, where the continuous bond transfers the impact load across the interface and the performance is proven in blade duty.
How do I choose for my fleet? Define the duty, the changeout model, and the shop capability, then confirm the retention and the replacement plan with the manufacturer.
Sources
Related articles
 Best Snow Plow Blade Family for Your Fleet: Top 5 ScenariosKnowledge
 Top 10 Snow Plow Blade Types for Winter Fleets (Ranked by Duty Fit)Knowledge
 Top 5 Best Carbide Blade Configurations for Highway PlowingKnowledge
 Best Snow Plow Blade Materials Ranked: Steel vs Carbide vs Cladding vs Rubber-CarbideKnowledge