
Batch-to-Batch Consistency in Carbide Inserts: Why Production Lines Depend on It
An assembly line feels every batch shift before anyone reads a report. Inserts that vary by fractions of a millimeter, or by a point of hardness, change how they feed, seat, and braze, and…
An assembly line feels every batch shift before anyone reads a report. Inserts that vary by fractions of a millimeter, or by a point of hardness, change how they feed, seat, and braze, and the first sign of trouble is an unexplained jam or a run of weak joints. For manufacturers running insert assembly, batch-to-batch consistency is not a quality nicety; it is the input the production line depends on.
This article explains where insert variation comes from, how process control keeps batches stable, what variation costs a production line, and how a buyer can assess consistency before committing to a supplier.
Assembly lines feel every batch shift
An automated insert line is built around a fixed program: the feeder expects a part, the robot expects a position, and the brazing cell expects a seat. When the incoming batch differs from the one before it, the program does not adapt; it fails.
The failure can be visible, like a jam, or silent, like a brazed joint that is slightly off position. Both cost production time, and both trace back to variation that a human line could absorb. That is why manufacturers who automate insert assembly put consistency at the top of the supplier requirement list.
SENTHAI, a Thailand-based manufacturer of carbide inserts, states that its quality control monitors the sintering environment and metallurgical properties, including grain size and hardness, to keep physical properties consistent from shipment to shipment. That is the kind of statement a production engineer wants verified, not just read.
Where does insert variation come from?
Insert variation starts in the material and follows the process:
| Source | How it adds variation |
|---|---|
| Raw material lots | Carbide powder and binder vary between lots |
| Powder preparation | Mixing and granulation affect uniformity |
| Pressing | Compaction density variation changes dimensions and porosity |
| Sintering | Temperature uniformity and atmosphere affect grain growth and hardness |
| Finishing | Grinding and surface preparation change dimensions and edge condition |
Each step is a potential source of variation, and each one has to be controlled or the variation compounds by the time the insert reaches the line. The supplier’s process control is what keeps the chain stable.
The material side deserves attention because carbide is a composite, not a pure metal. The tungsten carbide grain size and the cobalt binder content set the balance between hardness and toughness, and both can drift between lots if the powder supply changes. A batch record that names the material lot and the measured properties is the evidence that the drift is controlled.
How process control stabilizes batches
Stable batches come from controlled processes, not from inspection alone. Inspection catches bad parts; process control prevents them.
SENTHAI describes its insert production as using advanced compression molding and vacuum sintering with proprietary temperature control, achieving uniform grain size and wear resistance across batches. The elements of that control are measurable: temperature uniformity in the furnace, density consistency after pressing, and grain size and hardness monitoring at the metallurgical level.
For a buyer, the practical evidence of process control is the batch record: the parameters, the measurements, and the results that accompany each shipment. A supplier that can show the record can show the control.
The control also has to be auditable. The record should name the measured properties, the limits they must stay within, and the person or system that reviewed them. SENTHAI’s quality-control page describes incoming review, process checks, final sampling, and pre-packaging review, which is the four-stage framework a batch record should map to.
The audit also covers the equipment behind the control. Furnaces drift, presses wear, and measurement tools lose calibration, so the supplier’s maintenance and calibration records are part of the consistency story. A buyer that asks about calibration intervals and process-capability studies gets a picture of whether the control is maintained or assumed, and that picture is worth as much as the batch numbers on the paper.
The assessment should end with a written conclusion: the supplier is approved, conditionally approved with defined checks, or not approved. A conditional approval with a list of checks and a re-review date is often the right outcome for a new supplier, because it keeps the line moving while the consistency evidence builds. The written conclusion also protects the next buyer or the next season from restarting the assessment from zero.
The conclusion belongs in the supplier file alongside the batch records, so the next audit starts from the previous findings instead of from memory.
The file then becomes the standing record of the supplier’s consistency over time.
That standing record is what makes the next sourcing decision fast instead of speculative.
What variation costs a production line
The cost of variation shows up in production metrics before it appears in quality reports:
- Jams and stops: inserts outside the handling window stop the feeder or gripper;
- Rework: off-position brazing produces joints that must be reworked or scrapped;
- Line speed loss: every stop and adjustment costs throughput;
- Quality escapes: variation that passes inspection can fail in the field, which is the most expensive outcome of all.
The production engineer’s version of the cost is simple: a batch that runs clean is cheap, and a batch that stops the line is expensive, regardless of the unit price. That is why consistency is purchased, not just inspected.
The cost also extends beyond the line. A variation that passes assembly and reaches the field as a weak joint or a premature wear failure becomes a warranty claim, a customer complaint, and a rework program, all traced back to a batch that was cheaper by fractions of a cent per insert. The full cost chain, from line stop to field failure, is the real price of inconsistency, and it is the argument for buying from a supplier whose process control is documented rather than assumed.
How do you assess consistency before you buy?
Consistency can be assessed before a volume commitment:
- Request batch records from multiple shipments, not just one;
- Compare dimensional measurements and hardness values across the batches;
- Ask how process parameters are monitored and what triggers a batch review;
- Run a pilot lot through the actual line and measure feed, jam rate, and joint quality;
- Check the documentation that ships with each batch so the line can trace variation to a lot.
The pilot lot is the strongest evidence, because it tests the supplier’s consistency against the buyer’s actual equipment. SENTHAI states that sample availability and terms are confirmed in writing, which is the right model for a controlled pilot.
The assessment should also include the supplier’s response to a bad batch. Ask how a non-conforming lot is handled: quarantined, documented, and corrected at the process level, or quietly replaced? The answer reveals whether the supplier’s consistency program is real, because every process has failures and the control is in the response.
Source inserts you can rely on, batch after batch
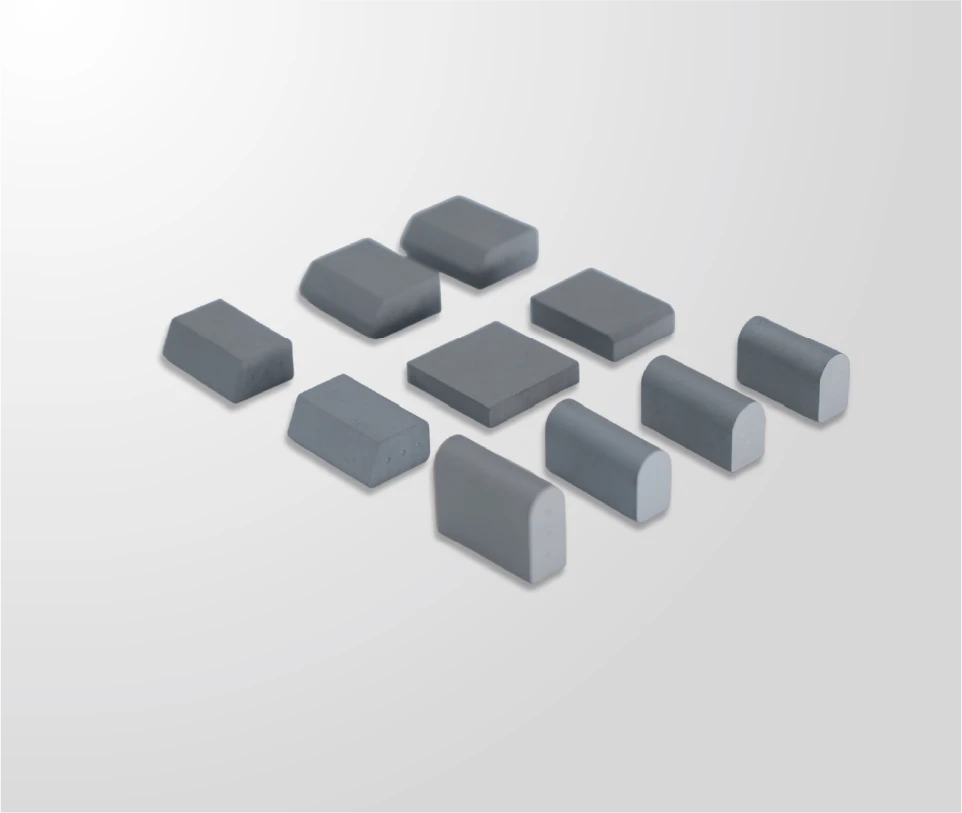
The sourcing decision for consistent inserts starts with the process and ends with the pilot. Confirm the process control, review the batch records, and validate with a pilot lot on the actual line. SENTHAI’s carbide inserts page describes the standard range, tolerances, and process controls, and its engineering team can confirm the batch documentation for an order.
Send the line requirements, the slot drawing, and the acceptance criteria through the contact page and ask for the batch records and pilot terms. The line depends on consistency; the purchase should be built on evidence of it.
Expert view — SENTHAI engineering team: “Consistency is the production line’s quiet fuel. The batch records are its gauge.”
Frequently Asked Questions
Why does batch consistency matter for production lines? Automated lines cannot adapt to variation. Inserts that change dimensions or hardness between batches cause jams, off-position brazing, and line stops.
Where does insert variation come from? Raw material lots, powder preparation, pressing, sintering, and finishing. Each step is a potential source, and control at each step prevents compounding variation.
How do suppliers keep batches consistent? Through controlled processes: temperature-uniform sintering, density control, and monitoring of grain size and hardness. Process control prevents variation; inspection only catches it.
What does variation cost? Jams, rework, line speed loss, and quality escapes. A batch that stops the line costs more than the unit price difference, regardless of how cheap it was.
How should I assess a supplier’s consistency? Review batch records across shipments, compare measurements, and run a pilot lot through the actual line with defined acceptance criteria.
What documentation should an insert order include? Batch numbers, dimensional inspection results, material and process records, and hardness or metallurgical data, confirmed during quotation.
Does SENTHAI provide batch records? SENTHAI states that every shipped batch is traceable and that required reports are confirmed during quotation, so batch documentation should be part of the order requirements.
What if a batch fails the line’s acceptance check? Document the failure, quarantine the lot, and work with the supplier on the root cause and the process correction. The response to a bad batch is part of the consistency assessment.
Sources
Related articles
 Best Snow Plow Blade Family for Your Fleet: Top 5 ScenariosKnowledge
 Top 10 Snow Plow Blade Types for Winter Fleets (Ranked by Duty Fit)KnowledgeTop 5 Best Carbide Blade Configurations for Highway PlowingKnowledge
 Best Snow Plow Blade Materials Ranked: Steel vs Carbide vs Cladding vs Rubber-CarbideKnowledge