
A snow plow cutting edge is a small component with an outsized effect on fleet uptime, scrape quality, replacement labor, and winter-route reliability — so the right decision starts with equipment fit and route conditions, not simply the lowest initial blade price. For OEMs, distributors, and fleet buyers, the practical sourcing question is which edge architecture fits the plow position, mounting system, roadway exposure, and validation requirements of a specific fleet.
(Last modified date: August 31, 2026)
Key Takeaways
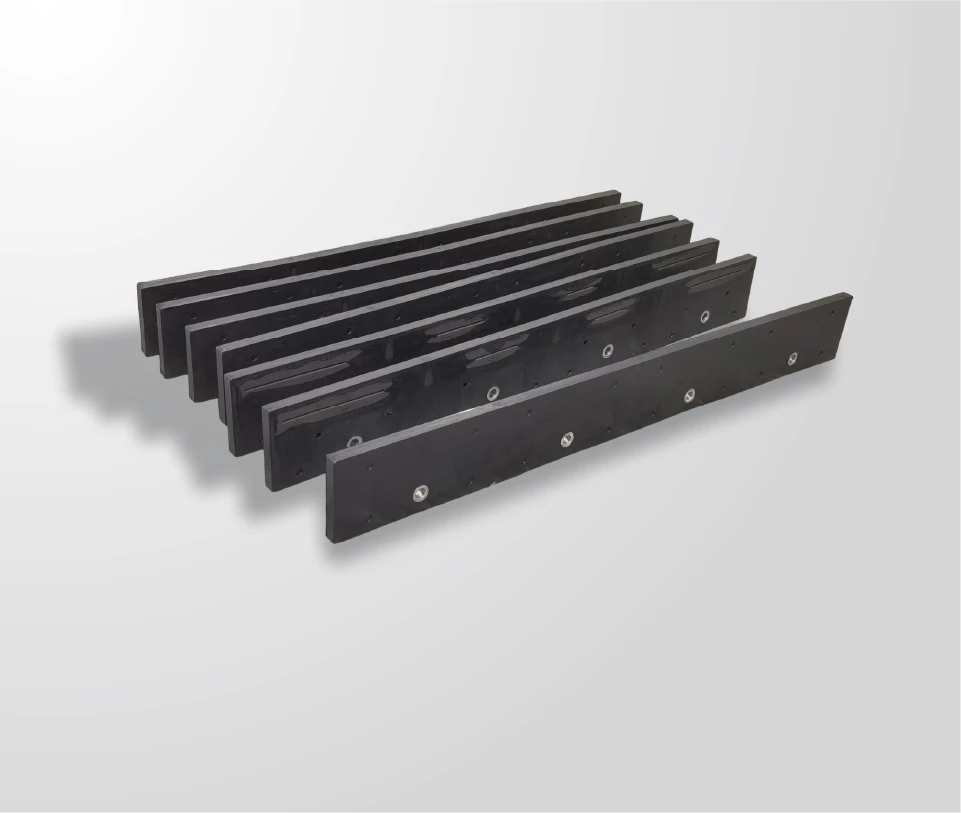
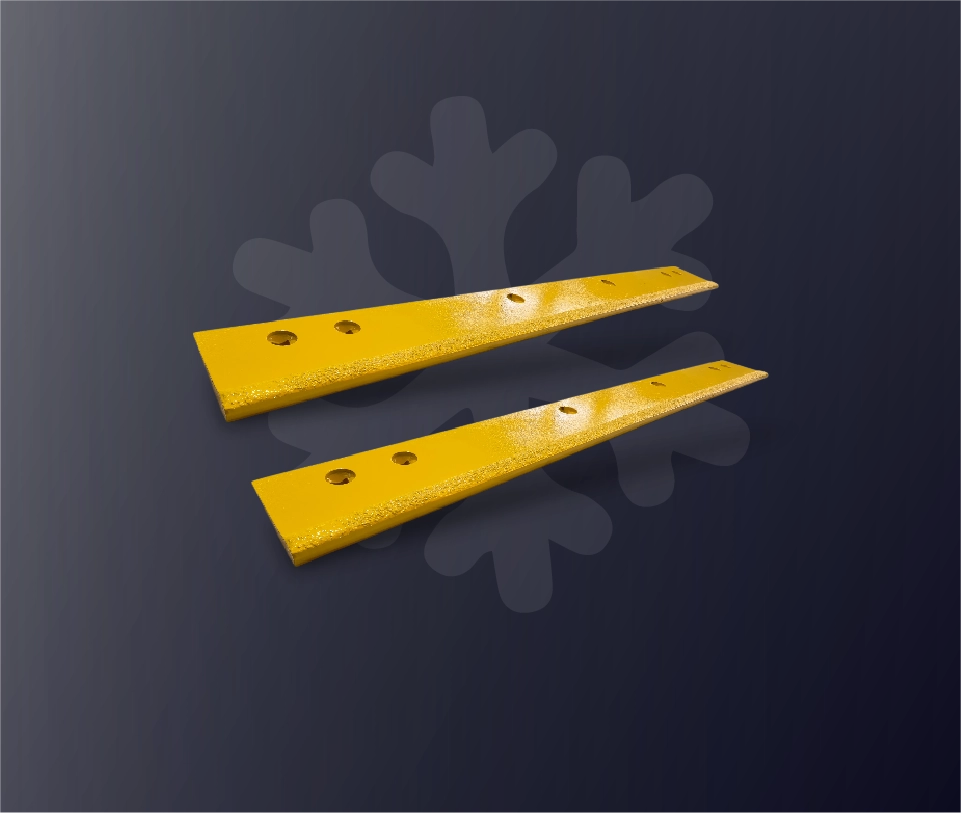
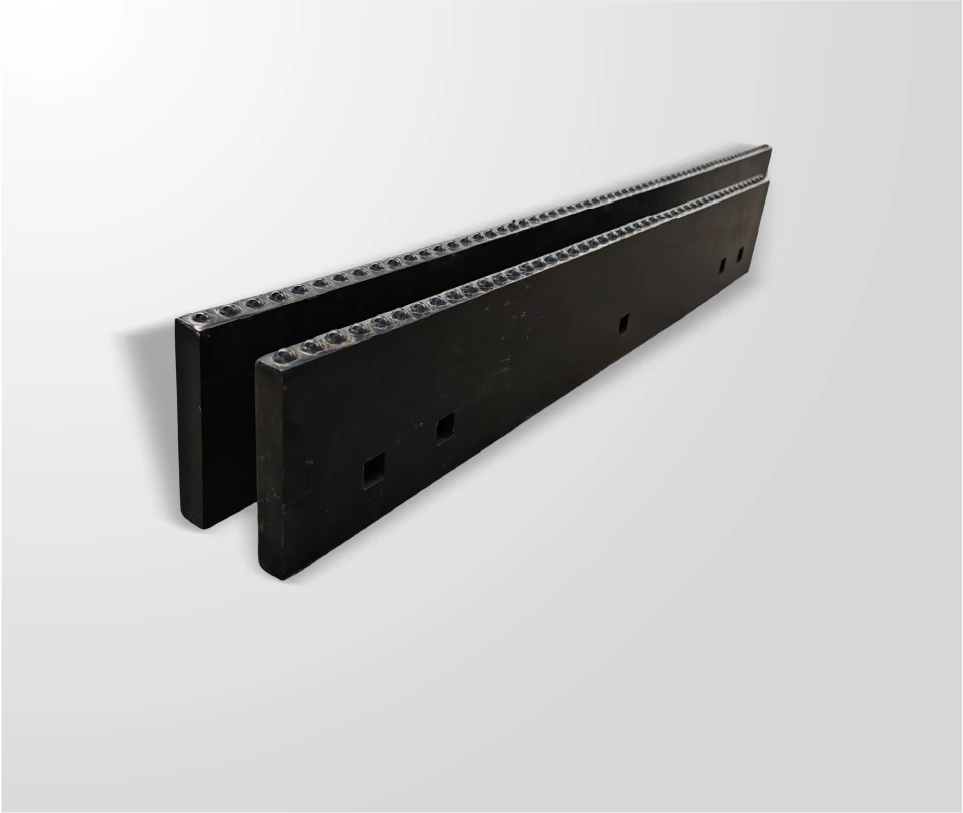
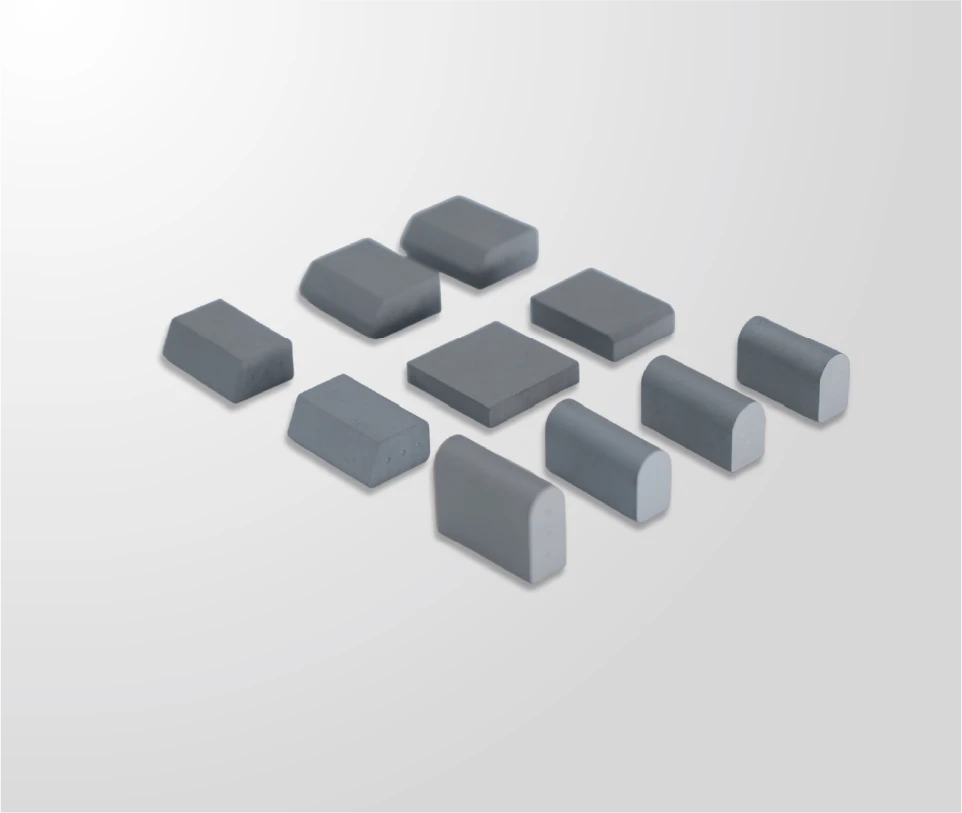
- “Snow plow cutting edge” covers several architectures: steel-backed carbide edges, JOMA-style segmented systems, packed-ice carbide systems, and bare tungsten carbide inserts.
- Fit is an engineering issue — confirm against the equipment drawing, hole spacing, thickness, clamping arrangement, and approved hardware.
- Carbide performance depends on grade, microstructure, binder, density, geometry, and joining design; higher hardness alone is not the best answer for impact-heavy routes.
- Do not modify, drill, weld, or heat-repair carbide edges in the field; see the buyer’s qualification checklist.
What Is a Snow Plow Cutting Edge?
A snow plow cutting edge is the replaceable wear component mounted along the working bottom edge of a snow plow. It contacts snow, ice, pavement, abrasives, joints, and obstacles while transferring scraping forces from the plow to the road surface. Key selection factors include plow position (front, underbody, wing, or another approved mounting location); edge geometry, overall length, thickness, hole pattern, clamp arrangement, and mounting hardware; route conditions including pavement type, packed snow, ice, gravel, joints, manholes, abrasives, and operating speed; and the balance between abrasion resistance, impact tolerance, flexibility, and replacement strategy.
Why Selecting This Wear Part Is Harder Than It Looks
Fit is an engineering issue, not a catalog assumption. A cutting edge must match the actual equipment drawing, blade architecture, hole spacing, thickness, clamping arrangement, and approved hardware; similar-looking edges may not install or operate the same way. Wear resistance and impact tolerance require trade-offs. Carbide performance depends on the grade and microstructure, binder system, density, porosity, geometry, joining design, and operating conditions. Road exposure changes the preferred architecture: long highway routes create sustained abrasion, while urban routes introduce manholes, bridge joints, curbs, uneven pavement, and frequent starts and stops; packed ice, gravel contamination, road brine, and changing temperatures further change the ideal solution. See also the cutting-edge manufacturer guide and high-performance industrial blades.
How the Sourcing and Validation Process Works
- Send the current drawing revision, hole pattern, material requirements, inspection criteria, and sample condition.
- Confirm fit against the equipment model, approved drawing, edge thickness, mounting structure, and hardware grade.
- Select the architecture and request product-specific carbide grade, steel carrier, rubber specification, insert geometry, and joining design.
- Validate a sample with physical installation and a field trial before volume orders.
- Request applicable incoming-material records, dimensional reports, inspection criteria, production-lot identification, and packaging review.
See also how to build a reliable winter wear-parts sourcing program and how high-frequency testing ensures braze integrity.
Frequently Asked Questions
What is the difference between carbide and steel snow plow cutting edges?
Steel and carbide-equipped edges differ in material behavior, geometry, joining method, and potential wear profile. Selection should reflect the route, impact exposure, plow configuration, and a fleet’s ability to validate actual field results.
How does a JOMA-style blade differ from a conventional carbide snow plow blade?
A JOMA-style blade is a segmented system combining carbide inserts, steel segments, and a rubber shell. A conventional carbide blade uses a different steel-and-carbide architecture, so neither should be specified using the other’s dimensions or performance assumptions.
Is a packed-ice carbide kit the same as a JOMA-style blade?
No. SENTHAI presents the packed-ice carbide kit as an isolated carbide-edged solution. Treat it as a distinct product architecture and validate it for the relevant ice, impact, mounting, and road-surface conditions.
Can SENTHAI manufacture to a drawing or sample?
SENTHAI states that it can discuss customization based on drawings, samples, or required specifications. Send the current drawing revision, hole pattern, material requirements, inspection criteria, and sample condition so the quote can be evaluated accurately.
What carbide grade, steel, and rubber specification should a buyer request?
Request the product-specific carbide grade or material designation, steel carrier requirement, rubber requirement where applicable, insert geometry, joining design, and associated inspection records — based on intended service conditions, not generalized from another blade type.
Are samples, MOQ, price, and lead time fixed?
No. These commercial terms should be confirmed for the specific part, quantity, customization level, packaging requirement, production schedule, and destination. Ask for a current written quotation.
Will the edge fit every truck, tractor, or snow plow?
No. Fit must be confirmed through the equipment model, approved drawing, hole spacing, edge thickness, mounting structure, hardware grade, and physical verification. Do not treat a cutting edge as a universal-fit or automatic drop-in replacement.
What quality and traceability information should buyers request?
Request applicable incoming-material records, dimensional reports, inspection criteria, production-lot identification, packaging review requirements, and agreed testing documentation. For carbide-to-steel or rubber-encased systems, specify the relevant joining or bonding inspection requirements.
Should operators grind or modify carbide cutting edges in the field?
No. Do not modify, drill, weld, heat-repair, or grind carbide edges in the field without equipment-manufacturer and engineering approval — field modification voids performance and safety assumptions.
Related Articles
- How to Qualify a Carbide Snow Plow Blade Manufacturer: A Buyer’s Checklist
- Snow Plow Cutting Edge Manufacturer: Custom Wear Parts
- Snow Plow Cutting Edge Supplier: Build a Sourcing Program
- Industrial Snow Plow Blades for Harsh Winters
- How Can High-Frequency Testing Ensure Braze Integrity?
Official Resources
- SENTHAI — Carbide Snow Plow Blade
- SENTHAI — JOMA-Style Blade
- SENTHAI — Packed Ice Carbide Kit
- SENTHAI — Carbide Inserts
- SENTHAI — Contact
Sources
- FHWA — Snow and Ice Road Weather Management
- OSHA — Crystalline Silica Overview
- U.S. CBP — Marking of Country of Origin
- SENTHAI — Snow Plow Products