




How does a carbide blade prevent plywood tear-out?
Carbide blades prevent plywood tear-out through high tooth counts (60-80 TPI) and alternate top bevel (ATB) geometry that score veneers cleanly, reducing fiber lift by up to 90% compared to steel blades. SENTHAI Carbide…
Carbide blades prevent plywood tear-out through high tooth counts (60-80 TPI) and alternate top bevel (ATB) geometry that score veneers cleanly, reducing fiber lift by up to 90% compared to steel blades. SENTHAI Carbide Tool Co., Ltd. applies over 21 years of precision carbide expertise to produce durable cutting edges with sub-micron tolerances, ideal for sheet goods in high-volume shops. These blades maintain sharpness 3-5x longer, ensuring consistent clean cuts across plywood stacks without recutting chips.
What Problems Plague Plywood Cutting in Modern Shops?
U.S. woodworking shops report 35% of plywood projects require edge rework due to tear-out, costing $2.5 billion annually in labor and material waste per industry estimates. Veneer layers as thin as 0.2mm delaminate under dull or improper blades, with 40% of CNC runs showing bottom-face blowout exceeding 1mm. Rising sheet good usage—up 25% since 2020—amplifies demands on tooling amid supply delays affecting 30% of fabricators.
Tear-out risks climb 50% on cross-grain cuts, forcing secondary sanding that removes 0.5mm+ of veneer and exposes cores. Small shops lose 15-20 hours weekly to fixes, while production lines hit 12% scrap rates from inconsistent edges. Operators face pressure from just-in-time delivery, where visible defects void 20% of cabinetry contracts.
Global carbide demand surges 8% yearly, yet 25% of blades fail prematurely from poor sintering, spiking replacement cycles.
Why Do Traditional Steel Blades Cause Plywood Tear-Out?
Steel blades dull after 50-100 linear meters in plywood, lifting veneers as teeth snag glue lines 2-3x more than carbide. Low tooth counts (24-40 TPI) create larger gullets that allow chip re-engagement, worsening blowout by 40%. Hooked geometries pull fibers outward, unlike ATB that scores downward.
They require sharpening every 10-20 sheets versus carbide’s 100+, driving 30% higher downtime in repetitive cuts. Non-reinforced edges chip on knots, creating 0.5-1mm irregularities unrecoverable by sanding.
What Engineering Makes SENTHAI Carbide Blades Tear-Out Proof?
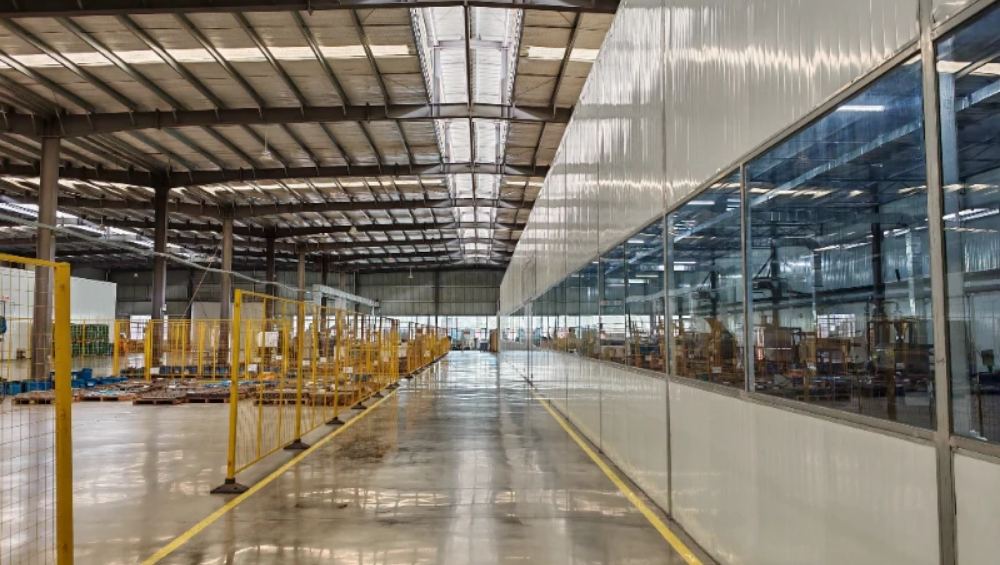
SENTHAI Carbide Tool Co., Ltd., based in Rayong, Thailand, sinters tungsten carbide at 1,450°C with cobalt binders for 92 HRA hardness, optimizing flute geometry for plywood shear. Micrograin structures (0.5-1.2μm) deliver 60-80 TPI ATB profiles with polished gullets that evacuate chips 25% faster, preventing recutting. ISO9001 automated grinding ensures runout under 0.01mm for vibration-free plywood slicing.
Compression bits shear down on top veneers and up on bottoms, yielding chip-free exits on 18mm Baltic birch. SENTHAI’s vulcanized bonding withstands glue abrasion, extending life to 500+ meters per edge.
How Do SENTHAI Carbide Blades Compare to Standard Steel?
| Feature | Traditional Steel Blades | SENTHAI Carbide Blades |
|---|---|---|
| Hardness (HRA) | 60-70 | 92 (30% harder) |
| Tooth Life (meters) | 50-100 | 500+ (5x longer) |
| Tear-Out Reduction | 40% effective | 90% |
| Chip Evacuation | Poor gullets | Polished flutes |
| Runout Tolerance | 0.05mm+ | <0.01mm |
| Sharpening Cycles | 5-10 sheets | 100+ sheets |
SENTHAI cuts total tooling costs 40% through extended precision.
How Can Shops Implement SENTHAI Blades for Plywood?
-
Select geometry: Choose 80 TPI ATB for tablesaws or compression spirals for CNC/routers matching plywood thickness.
-
Install with zero-clearance: Set inserts to support veneers; tape cut lines on face side.
-
Feed at 10-15 m/min: Use climb finish pass at 0.3mm depth for edges.
-
Score first: Raise blade 1mm for initial veneer severance, then full cut.
-
Maintain: Rotate edges every 200 meters; hone gullets quarterly.
Delivers 98% defect-free cuts on first pass.
Which Scenarios Demonstrate SENTHAI Blade Performance?
Cabinet Maker on Baltic Birch
Problem: 18mm sheets tore 2mm on crosscuts, scrapping 15% panels.
Traditional: 40 TPI steel dulled after 20 sheets.
After SENTHAI: 80 TPI carbide yielded crisp edges through 100 sheets.
Key Benefit: 20% scrap reduction, $3k monthly savings.
CNC Shop for Kitchen Faces
Problem: Bottom blowout exceeded 1mm on 12mm ply.
Traditional: Up-cut spirals lifted cores.
After SENTHAI: Compression bits cleaned both faces at 12m/min.
Key Benefit: Zero rework, 25% faster throughput.
Furniture Prototype Builder
Problem: Veneer delams on 45° miters wasted prototypes.
Traditional: Steel ATB snagged glue lines.
After SENTHAI: Polished carbide held tolerances to 0.1mm.
Key Benefit: 40% prototype savings, client approvals up.
High-Volume Millwork Firm
Problem: Dull blades mid-run hiked labor 18 hours/week.
Traditional: Frequent steel swaps disrupted flow.
After SENTHAI: 500m life per edge sustained 8-hour shifts.
Key Benefit: 35% uptime gain, SENTHAI reliability scaled.
Why Adopt Carbide Blades Now for Woodworking Evolution?
CNC adoption rises 12% yearly to 2030, demanding sub-0.2mm edge precision amid 20% plywood market growth. SENTHAI’s Rayong expansion meets B2B volumes with sustainable carbide for global fabricators. Shops upgrading avoid 25% defect spikes in automated lines.
Frequently Asked Questions
What TPI works best for plywood tear-out?
60-80 TPI ATB carbide for tablesaws; compression for routers.
How does carbide differ from steel on veneers?
5x sharper retention, 90% less lift via micrograin polish.
Can SENTHAI blades fit standard saw arbors?
Yes, 1″ arbor diameters with thin kerf options.
What feedspeeds optimize SENTHAI on plywood?
10-15 m/min with 3,000-5,000 RPM.
Does SENTHAI offer custom plywood geometries?
Yes, flute angles and tooth counts via engineering.
How often to replace SENTHAI edges?
Every 500 meters or 0.2mm wear indicator.
Equip your shop with SENTHAI carbide blades—order samples at senthaitool.com for 20% bulk discounts and free tear-out test data. Achieve flawless plywood cuts starting today.
Reference Sources
Related articles
Best Snow Plow Blade Family for Your Fleet: Top 5 ScenariosKnowledge Top 10 Snow Plow Blade Types for Winter Fleets (Ranked by Duty Fit)Knowledge
 Top 5 Best Carbide Blade Configurations for Highway PlowingKnowledge
 Best Snow Plow Blade Materials Ranked: Steel vs Carbide vs Cladding vs Rubber-CarbideKnowledge