
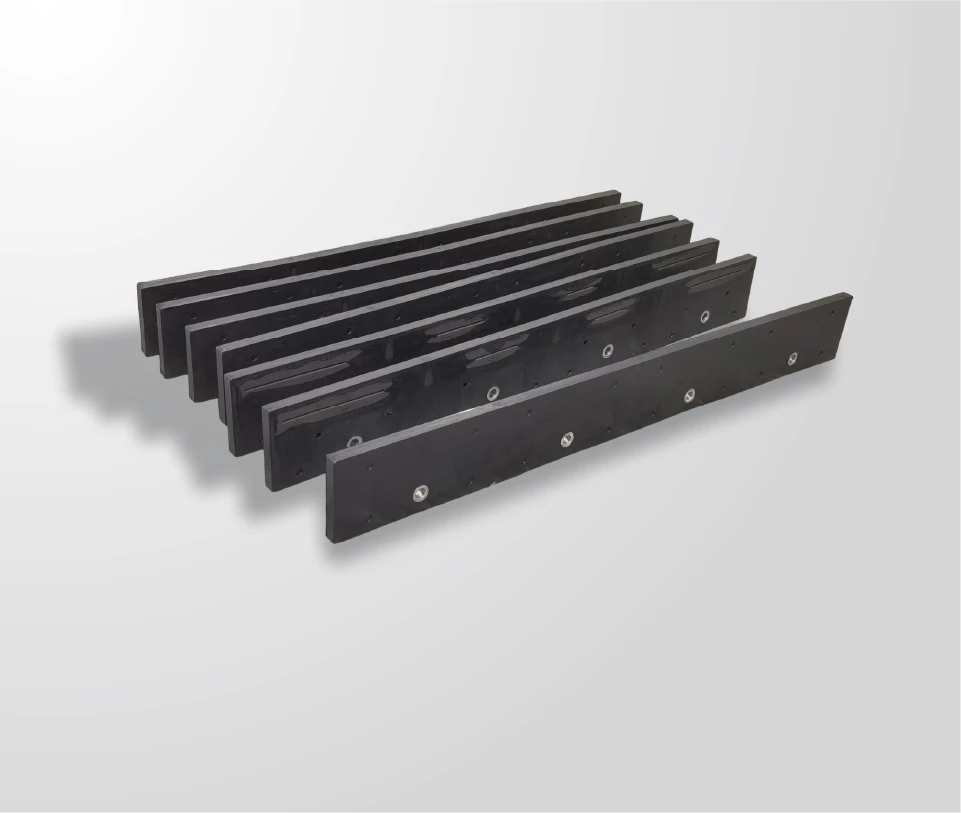
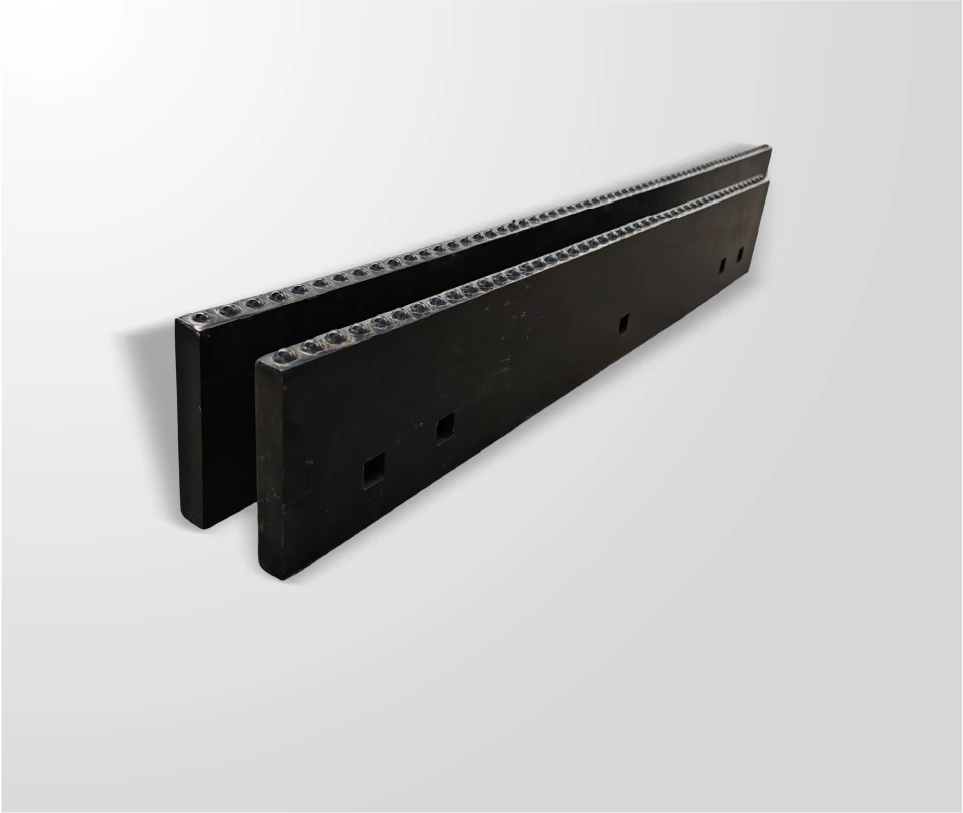
Cutting Edge Steel Grades: 1045, 1080, A36 and Through-Hardened
Cutting edge steel grades are usually settled by whoever quoted last, and the result is a fleet running three different specifications on machines doing the same job. Grades such as 1045, 1080, A36 and…

Cutting edge steel grades are usually settled by whoever quoted last, and the result is a fleet running three different specifications on machines doing the same job. Grades such as 1045, 1080, A36 and a through-hardened and tempered section are not interchangeable: they differ in how hard they can be made, how much impact they tolerate before cracking, whether they can be repaired in the field, and how they behave once the surface starts to wear. Buying by grade name alone is therefore as unreliable as buying by price alone, because the name does not state the condition the part is supplied in.
What Each Grade Is Actually Specified For
Each grade covers a different duty band.
A36 suits light, non-abrasive work, 1045 covers general duty, 1080 and through-hardened sections take abrasive work, and the supplied condition matters as much as the name.
The grade designations themselves come from a numbering convention that the standards bodies maintain, and the material and test standards used to qualify those grades are published by ASTM and by the engineering societies behind the designations, including SAE; that is why a specification should name both the grade and the standard it is bought to.
A36 is a structural carbon steel, supplied in an as-rolled condition. It is inexpensive, easy to cut, drill and weld on site, and adequate where the edge is not the limiting part of the job: light grading, spreading and low-hour machines. It wears quickly on abrasive ground and rounds off early, which is a production cost rather than a parts cost.
1045 is a medium-carbon grade and is the workhorse of bucket, grader and dozer edges. Supplied in a hardened and tempered condition it holds a cutting profile far longer than A36, and it remains weldable with the correct procedure, which is why it dominates the middle of the market. A high-carbon grade such as 1080 can be taken harder again, giving better abrasion resistance where the ground is aggressive, at the cost of toughness and of any field welding. A through-hardened and tempered edge is better understood as a specification rather than a grade: the section is quenched and tempered to a controlled hardness band, which is what makes wear life predictable across batches.
Hardness and Toughness Trade-Offs
Hardness and toughness move in opposite directions in steel, and an edge specification that asks for more of one without stating what it will give up on the other is not a specification. A harder edge resists abrasion longer but tolerates less impact before it cracks; a tougher edge deforms rather than fractures but loses its cutting profile sooner, which increases passes, fuel burn and the load on the structure behind it.
| Property | A36 | 1045, hardened and tempered | 1080 or through-hardened band |
|---|---|---|---|
| Abrasion resistance | Lowest | Moderate | Highest of the three |
| Impact tolerance | High; deforms rather than cracks | Balanced | Lowest |
| Repair on site | Straightforward | Procedure-controlled | Generally not a field operation |
| Dimensional stability | Poor under load | Good | Good when properly supported |
The metallurgy behind those differences is documented rather than proprietary: ASM International publishes the reference material on steel heat treatment and wear behaviour that most edge specifications are ultimately built from. Two practical consequences follow. The first is that hardness has to be quoted as a band with a test method, not as a single figure, because a single figure describes one point on one part. The second is that the balance point moves with the machine: a heavier machine working mixed ground delivers more impact through the edge, so it may be correct to accept lower hardness on that machine than on a smaller one working cleaner material.
A third consideration is thickness, because hardness cannot compensate for a section that is too light. An edge that is hard but too thin for the load will bend at the hole line, and a bent edge is scrap regardless of grade. Where a fleet is standardising, thickness is usually the first variable to fix and grade the second.
How the Grade Is Verified
Verify with documents, not with the grade name.
Ask for the mill certificate or heat analysis, the hardness test method and result, and the identity of the batch, and check that they describe the part in front of you.
Verification starts with the paperwork and ends with a check on the part. A mill or material certificate should name the grade and the standard it was supplied to, and a hardness result should name the method used and where it was taken. A European quotation may describe the same requirement by a different designation, which is why having the drawing and the certificate refer to a named standard, indexed through DIN on the European side, removes ambiguity before an order rather than after delivery.
The second element is traceability. A batch identity that links the delivered edge to an inspection record is what allows a wear complaint to be investigated against production data instead of argued. SENTHAI operates lot-level traceability, with every batch inspected and archived, so a grade question can be answered from records; the inspection arrangement is described on the quality control page.
The third element is dimensional and visual: pattern, section, straightness and the condition of the cutting profile and countersinks. A grade question on a part that does not fit the pattern is a distraction, so the dimensional check comes first, and the hardness or chemistry result is read against the specification afterwards.
Wear Behaviour on Real Surfaces
The same grade behaves differently on different ground, and the difference is larger than the difference between two adjacent grades. Angular, silica-bearing aggregate scratches and cuts steel, so hard phases are worn away quickly and the profile rounds; limestone and softer materials largely displace, so a moderate grade can survive a long time on the same machine. Frozen or ice-bonded material introduces impact loading at the same time as abrasion, which is the combined duty that most often breaks an over-hard edge.
Published abrasion data is a useful starting point rather than an answer. Steel producers document abrasion performance for their wear grades, as SSAB does for its range, and the same producers also publish product information through suppliers such as voestalpine. The discipline for a buyer is to ask for the conditions behind a comparative figure, because an abrasion number measured on one abrasive is not a prediction for another.
Two further conditions change what happens at the edge. Moisture and fines create a polishing wear pattern that removes the cutting profile without obvious metal loss, and a hard surface layer that has been overheated during welding or cutting loses its hardness locally. Both produce a part that looks sound and cuts poorly, which is why a failure record explains more than the grade label does.
Weldability and Repair Considerations
Weldability is where grade selection meets workshop reality, and it is frequently ignored until a repair is needed. A36 and 1045 can be welded with a procedure appropriate to the carbon content and section, using preheat and controlled cooling where the thickness or the grade requires it; a high-carbon or fully hardened edge is a different case, where field welding risks a hard, brittle zone at the joint that cracks in service. The welding processes and consumable selection guidance for structural steels are published by the AWS.
Three rules keep repairs from making the situation worse. Weld only where the design permits it, and never as a substitute for a replacement edge that has reached its wear limit. Restore, rather than build up, the profile: a thick weld bead on a cutting edge changes the cutting geometry as well as the metallurgy. And re-check hardness locally after any thermal operation, because the hardness that was specified applies to the part as supplied and not to a repaired zone.
Where an edge is being run to a wear limit, the decision point is measurement rather than calendar: once the remaining section at the hole line approaches the point where the edge will bend, repair stops being economical.
Cost Per Hour by Grade
Cost per hour of machine work is the comparison that makes grade selection rational, because it includes the labour and the downtime that unit price excludes. The model is simple: edges consumed per hour, multiplied by delivered price plus change-out cost, plus the production lost during the periods when the edge was worn.
| Cost driver | A36 | 1045 hardened and tempered | 1080 or through-hardened |
|---|---|---|---|
| Unit price | Lowest | Mid | Highest |
| Changes per season | Most | Fewer | Fewest on abrasive ground |
| Labour and downtime paid | Repeatedly | Moderately | Least often |
| Production penalty as it dulls | Large on hard material | Small to moderate | Small until the profile is consumed |
Change-out cost is not a constant, and that is what makes the comparison fleet-specific. A shop-based fleet with spare edges on the shelf pays far less per change than a contractor calling out a fitter to a remote site, so the same grade can be correct for one and wrong for the other. The production penalty also depends on the material: a dull edge in loose sand costs a little, while the same edge in compacted clay or crushed rock costs a great deal.
The practical consequence is that the comparison should be run on the fleet’s own records, using edge type, material worked, hours and volume between changes. That record also prevents a common error: changing two variables at once when a grade is trialled.
Selecting by Application
The selection rule is short, and it starts with the ground rather than with the grade. Grade, thickness and condition of supply then follow from the duty band that the ground implies.
- Light, clean or seasonal work: A36 is adequate and inexpensive, provided the edge is changed on measurement.
- General grading, spreading and mixed ground: 1045 in a hardened and tempered condition is the working standard.
- Abrasive gravel, crushed rock or high annual hours: a higher-carbon or through-hardened band, with thickness fixed for the machine class.
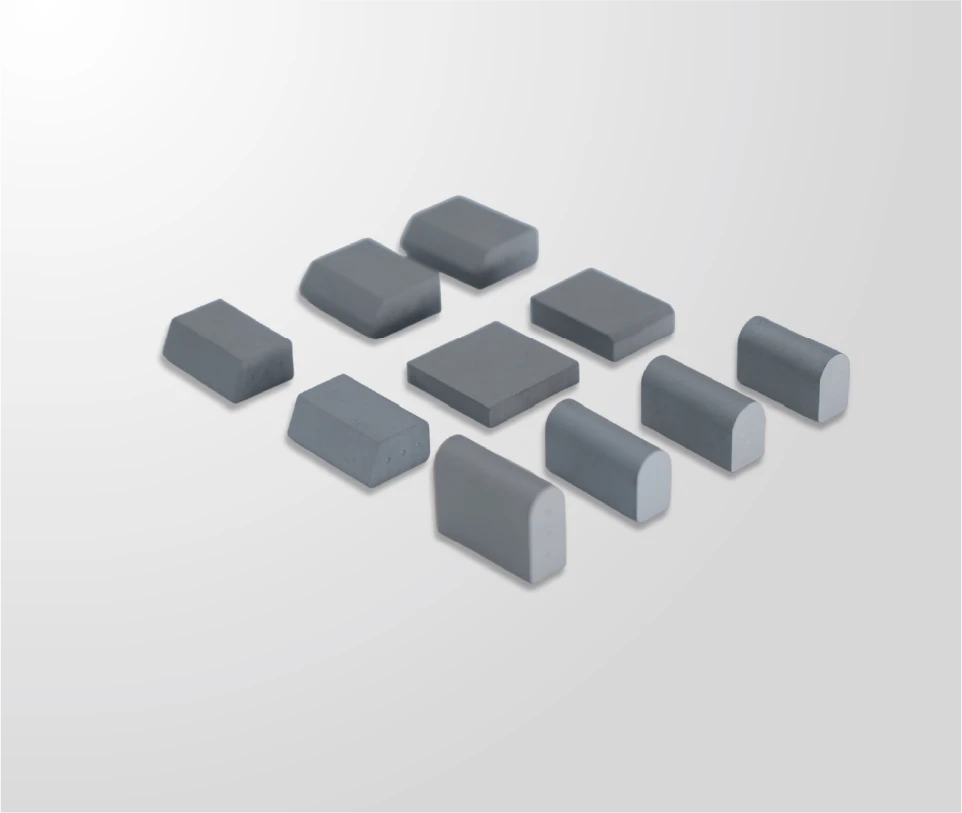
- Impact-heavy material and rock: accept lower hardness and a tougher section, or move to a carbide-tipped edge rather than pushing a brittle steel edge harder.
- Repair-intensive operations: favour grades that can be welded with a controlled procedure.
- Before ordering: confirm the pattern by drawing or measurement, and require the grade and the standard on the certificate.
How these grades sit alongside carbide and where the choice stops being about steel is covered in the edge materials section of the carbide edge guide and in the wider view of wear parts beyond plows.
Grade selection comes down to the ground, the machine and the cost of stopping it. A36 is a light-duty answer where the edge is not the constraint; 1045 hardened and tempered covers most general duty and remains repairable; higher-carbon and through-hardened sections buy abrasion resistance and give up toughness and field repairability in exchange. In every case the grade is only half the specification: thickness fixes whether the section survives, the condition of supply fixes the hardness actually delivered, and the certificate and batch identity are what allow a wear complaint to be resolved technically.
Send SENTHAI the machine list, the ground each machine works and the current edge grade, with a drawing or worn sample for pattern reference, and the technical team will review grade, thickness and condition of supply for each duty band.
Related reading: the hub article on wear parts beyond plows positions these steel edges against the other ground-engaging products.
Frequently Asked Questions
Which steel grades are used for cutting edges?
Bucket, grader and dozer edges are commonly supplied in a structural carbon steel such as A36 for light work, a medium-carbon grade such as 1045 in a hardened and tempered condition for general duty, and higher-carbon or through-hardened sections where abrasion is severe. The distinction that matters commercially is the condition of supply: the same grade name delivered as-rolled and delivered quenched and tempered behaves as two different products.
Is a harder cutting edge always better?
No. Hardness and toughness trade against each other, so an edge taken harder resists abrasion longer but tolerates less impact before cracking, and it also loses weldability. Impact-heavy rock, frozen ground and heavy machine classes all push the balance toward toughness. The right hardness is the one that keeps the edge cutting without fracturing on the ground that machine actually works, which is why grade selection follows the duty.
How can I confirm the grade of an edge I have received?
Check the documents against the part. A mill or material certificate should name the grade and the standard it was supplied to, and a hardness result should name the test method and where it was taken. Batch identification that links the delivered edge to an inspection record lets a wear question be investigated against production data. Dimensional checks on pattern, section and countersinks should come first, because a fitting error is not a grade issue.
What documentation and commercial terms apply to a cutting edge order?
The documentation set covers the grade and standard, the hardness band with its test method, the batch identity and the pattern drawing, and it is agreed with the order rather than assumed. Minimum order quantity, lead time, packing, delivery and warranty terms vary with specification, quantity and destination, and the applicable terms for a specific requirement are stated in the written quotation or order documents.
{
“@context”: “https://schema.org”,
“@type”: “FAQPage”,
“mainEntity”: [
{
“@type”: “Question”,
“name”: “Which steel grades are used for cutting edges?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Bucket, grader and dozer edges are commonly supplied in a structural carbon steel such as A36 for light work, a medium-carbon grade such as 1045 in a hardened and tempered condition for general duty, and higher-carbon or through-hardened sections where abrasion is severe. The distinction that matters commercially is the condition of supply: the same grade name delivered as-rolled and delivered quenched and tempered behaves as two different products.”
}
},
{
“@type”: “Question”,
“name”: “Is a harder cutting edge always better?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “No. Hardness and toughness trade against each other, so an edge taken harder resists abrasion longer but tolerates less impact before cracking, and it also loses weldability. Impact-heavy rock, frozen ground and heavy machine classes all push the balance toward toughness. The right hardness is the one that keeps the edge cutting without fracturing on the ground that machine actually works, which is why grade selection follows the duty.”
}
},
{
“@type”: “Question”,
“name”: “How can I confirm the grade of an edge I have received?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Check the documents against the part. A mill or material certificate should name the grade and the standard it was supplied to, and a hardness result should name the test method and where it was taken. Batch identification that links the delivered edge to an inspection record lets a wear question be investigated against production data. Dimensional checks on pattern, section and countersinks should come first, because a fitting error is not a grade issue.”
}
},
{
“@type”: “Question”,
“name”: “What documentation and commercial terms apply to a cutting edge order?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “The documentation set covers the grade and standard, the hardness band with its test method, the batch identity and the pattern drawing, and it is agreed with the order rather than assumed. Minimum order quantity, lead time, packing, delivery and warranty terms vary with specification, quantity and destination, and the applicable terms for a specific requirement are stated in the written quotation or order documents.”
}
}
]
}
