
Loader Bucket Cutting Edge Types: Bolt-On, Weld-On and Segmented
A loader bucket cutting edge is replaced twice before anyone asks why the lip is cracking. The decision that repeats itself every season is not which edge costs least per piece, but which of…

A loader bucket cutting edge is replaced twice before anyone asks why the lip is cracking. The decision that repeats itself every season is not which edge costs least per piece, but which of the three mounting families — bolt-on, weld-on or segmented — suits the bucket, the machine class and the material handled. Each family changes wear life, change-out time, lip load and the workshop labour it absorbs, and once a bucket has been built around one of them the others are not a straight swap.
What Each Design Is For
Bolt-on swaps fastest; weld-on wears longest.
Bolt-on edges suit buckets re-edged without a welding set, weld-on edges trade serviceability for an uninterrupted cutting line, and segmented sets let a wide bucket be renewed piece by piece.
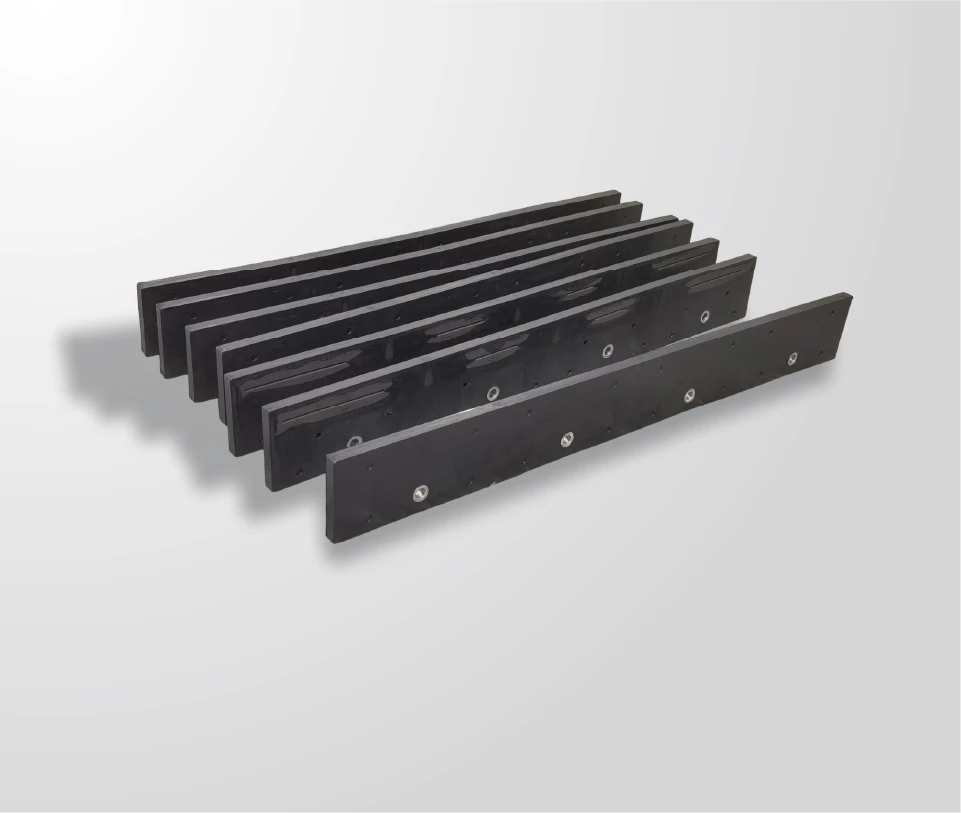
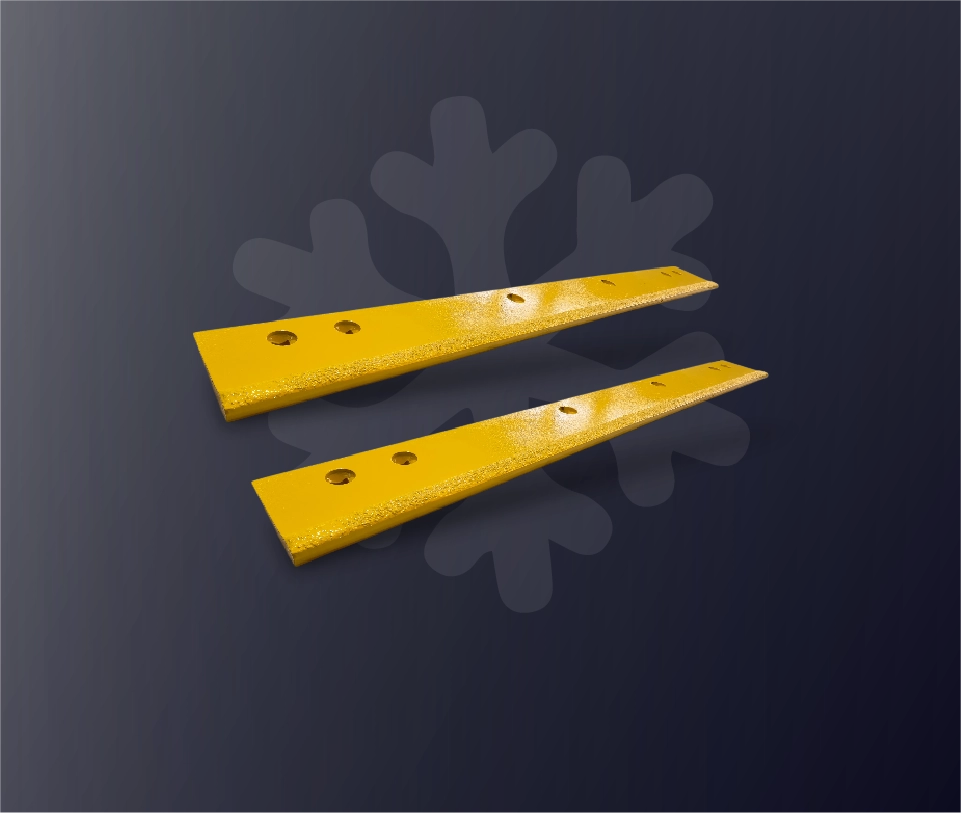
A bolt-on edge is a separate consumable fixed through countersunk plow bolts into the bucket lip. The lip keeps its structural role and the edge is designed to be consumed, which is why this family dominates fleets that must return a machine to work the same morning. The cost is the fastener interface: the countersink must seat, the bolts must hold torque, and the edge must sit flat instead of bridging a worn spot.
A weld-on edge is joined directly to the lip or into a pocket prepared for it. There are no fasteners to lose and no bolt holes to act as crack starters, so the cutting line stays continuous and can run closer to the material. Replacement is a hot work job, which suits a bucket welded once and run long shifts in one material. A segmented edge breaks that line into shorter pieces across a wide bucket, spreading wear and tolerating a lip that is no longer flat. Interface conventions are published through SAE and AEM.
Wear Life and Load Effects
Wear life is set by how the edge meets material, not by hardness alone. A bucket filling from a loose stockpile wears its edge evenly; the same bucket digging a face or back-dragging presents a loaded cutting contact in which the tip and underside take most of the loss. That difference explains why two machines on one site consume edges at completely different rates.
Mounting family changes the geometry. A bolted edge sits proud by the thickness of its fixings and leaves a joint for fines to enter. A welded edge is continuous with the lip, so there is no joint to rock on. A segmented edge divides the load between separate faces, which reduces what any single section carries and changes how the bucket fills.
Load effects matter as much as wear. A welded edge stiffens the lip and passes shock straight into the bucket structure, so rock work benefits from reinforcement behind the edge rather than a heavier edge alone. A bolted edge absorbs some shock but lets the edge move under load once torque is lost, and movement at a joint wears holes until the pattern no longer holds.
| Point | Bolt-on | Weld-on | Segmented |
|---|---|---|---|
| Cutting line | Continuous, sits on top of the lip | Continuous and flush with the lip | Broken into separate faces |
| Consumable unit | One edge plus fastener set | One welded edge | Short sections, renewed individually |
| Wear pattern | Even, joint receives fines | Even, lip wear hidden behind the weld | Uneven between sections, easy to monitor |
| Main risk | Loose or sheared fasteners | Heat input and lip distortion | Mis-matched segment heights |
Change-Out Time and Downtime
Change-out time is where a specification that looks expensive per piece becomes the cheaper decision. A bolted edge can be changed in the field with hand tools when the pattern and fasteners are right, and the same job becomes a workshop visit when they are not. Rounded countersinks, seized bolts and stretched holes turn an hour of work into cutting, drilling and re-tapping the lip.
A welded edge is a scheduled job. It needs the bucket positioned for access, the old edge cut clear, the lip dressed and the new edge aligned and welded with heat input controlled so the lip does not distort. That belongs in a planned window between shifts, and a fleet that runs a welded edge without such a window will eventually run it until the lip is damaged.
Segmented sets sit between the two. Segments can be replaced one at a time by a crew that would rather spend twenty minutes on a machine than take it out of service, and shorter pieces are easier to handle where lifting aids are limited. Whichever family is chosen, the comparison should be run against the cost of the machine standing still. Handling and guarding expectations are set out in 29 CFR 1910.
Material and Hardness Choices
Three material routes sit behind a loader bucket edge: a through-hardened steel edge, a wear-resistant steel edge with higher alloy content, and an edge that carries tungsten carbide as its working surface.
Hardened steel edges are the baseline for general purpose buckets. They hold a profile longer than a plain carbon section and can be straightened once or twice in a press. Wear-resistant grades go further: producers such as SSAB publish abrasion data for wear steels rather than one headline figure, and the methods used to quote hardness are published by ASTM. Hardness quoted without a method is not a specification.
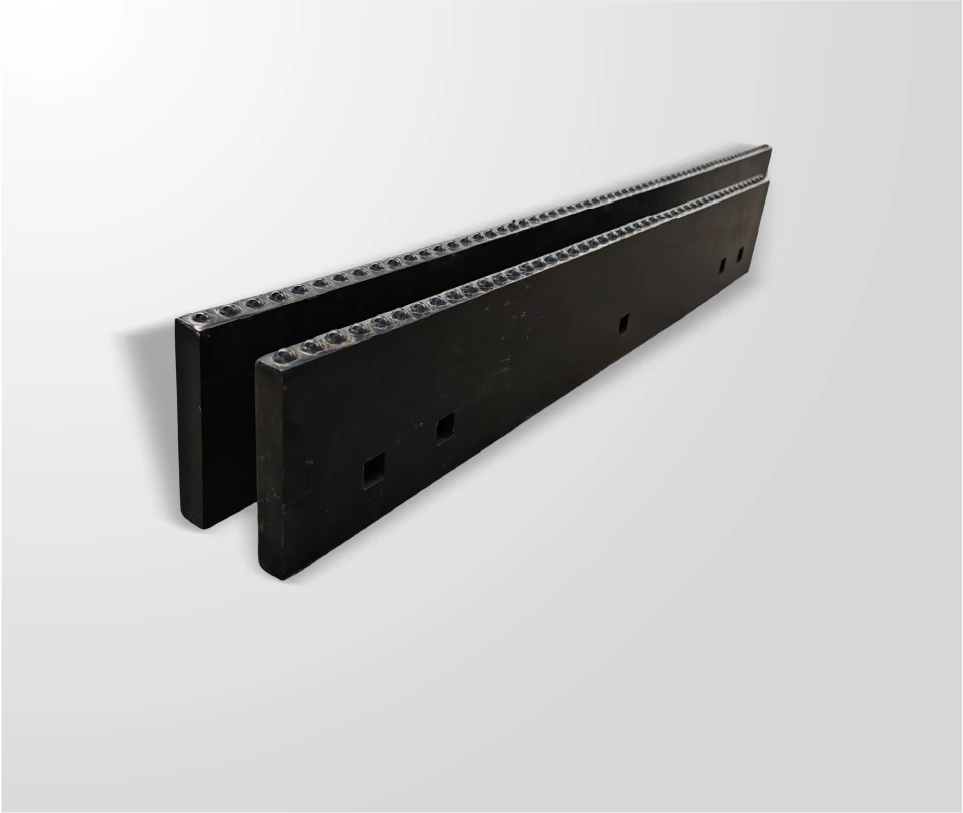
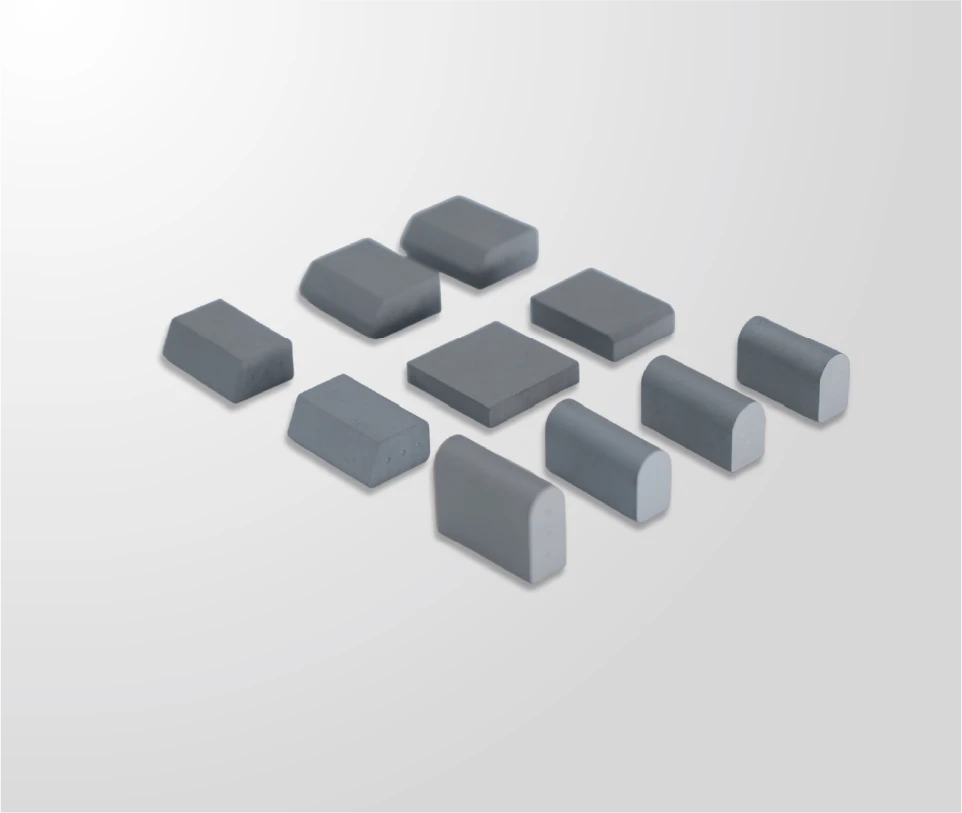
A carbide-edged bucket puts cemented tungsten carbide at the wear surface, brazed into machined pockets rather than welded on. Carbide resists abrasion far beyond any steel, so the limiting features become the pocket, the braze joint and the body behind them. Materials references from ASM International set out how hardness and toughness are traded in a wear application.
Hardness alone is a poor selector. An edge too hard for the shock it receives chips and spalls, and an insert too hard for the joint behind it lifts out. Abrasive, low-impact work gains most from a harder working surface; mixed rock with brittle edges finds the opposite. The balance point is decided per application, then confirmed by drawing.
Fitment Across Bucket Families
Fitment is where a correct specification becomes a rejected delivery, and it is the one variable a buyer can eliminate with a drawing and a tape measure. Four measurements travel with every bucket edge.
- Hole pattern. Hole diameter, spacing along the edge, and the distance from hole centre to the cutting face. A pattern that is close is not a pattern that fits.
- Section shape. Flat, beveled and curved edges are not interchangeable, and a curved edge on a straight lip leaves a gap that fills with fines.
- Thickness and lip height. A heavier edge sits further below the lip and changes the digging angle and rear clearance.
- Countersink and fastener. Plow bolt heads must seat flush in a matching countersink; a mismatched angle leaves the head proud and loosens the joint.
Fleets with mixed machine populations rarely hold one drawing per model. Measuring the pattern on the machine, recording the lip height and hole count, and validating that against a fitment drawing is faster than identifying a model year. It is also the method SENTHAI works to: bolt patterns are validated against a drawing or a physical sample before release, with machined insert pockets held to plus or minus 0.02 mm.
Cost Per Operating Hour
Unit price answers a purchasing question, not a fleet question. The number that decides a specification is cost per operating hour: the price of the edge or segment set divided by the hours it survived, plus the labour and lost production attached to each change.
Change-out frequency multiplies everything attached to it. An edge replaced twice as often also doubles fastener consumption, workshop hours and the risk of lip damage each time the joint is disturbed. On a machine running two shifts, lost production from an unplanned change can exceed the price of several edges. Aggregate industry practice around that trade-off is collected by the NSSGA.
| Input | Source | Effect on the comparison |
|---|---|---|
| Hours on the machine | Hour meter at fit and at change | Supplies the denominator for every edge fitted |
| Material handled | Site log or load tickets | Explains wear differences between machines |
| Labour per change | Workshop time booked to the machine | Multiplied by changes per year |
| Fastener consumption | Stores issues against unit number | Reveals a pattern or torque problem early |
| Lip condition | Inspection notes at each change | Shows whether the edge protects the bucket |
Two cautions belong with the arithmetic. Hours are not equal across sites, so a comparison built on a stockpile machine will not transfer to a face machine. And an edge that survives longer while damaging the lip is not cheaper, because the lip is the structural part of the bucket and takes far longer to repair than to protect.

Choosing by Machine and Material
The selection rule that survives contact with a real fleet is short, and it starts from material and downtime rather than from part numbers.
- Loose stockpiles, sand and gravel, single-shift use: a hardened steel bolt-on edge replaced on measurement.
- Face digging in abrasive rock or slag: a carbide-edged or wear-resistant edge, with the lip reinforced and the joint checked at every change.
- Wide buckets with limited lifting aids: segmented sets, so each section can be handled safely.
- Distributor stock and mixed fleets: standardise on the two or three hole patterns covering most machines, and hold one abrasive-duty option.
- Before any order: confirm hole pattern, countersink, thickness and section shape by measurement or drawing.
Where a bucket has already been welded on or modified, the same three questions still apply: what does the machine handle, what does an hour of downtime cost, and can the pattern be confirmed without guesswork. Answering them from drawings and a physical sample is what turns an edge into a repeatable purchase rather than a trial.
The mounting family is a service decision before it is a wear decision. Bolt-on edges keep machines in service and put the risk in the fastener joint; weld-on edges give an uninterrupted cutting line and move the risk into heat input and lip condition; segmented sets trade uniformity for safe handling and piece-by-piece renewal on wide buckets. The working surface is the second decision and it follows the material: sustained abrasive loading justifies a harder edge, while shock loading punishes one that is too brittle. Because hole pattern, section shape and thickness decide whether any of it fits, fitment confirmation belongs in the same document as the grade.
Send SENTHAI the bucket drawings or a measured hole pattern, the material the machine handles and the change-out hours you are currently seeing, and the technical team will review mounting family, hardness and toughness balance and fitment tolerance for each bucket group.
Related reading: wear parts beyond plows.
Frequently Asked Questions
How do I know whether a bolt-on or weld-on bucket edge suits my machine?
Start from service, not price. If the machine must return to work the same day and the lip is sound, a bolt-on edge keeps that option open and the fastener joint is manageable. If the bucket runs long shifts in one abrasive material and the fleet can plan a welding window, a weld-on edge gives a continuous cutting line with no joint to maintain. Mixed fleets usually end up running both.
What thickness of loader bucket cutting edge should I order?
Thickness has to be read together with the bucket lip, the machine class and the material. A heavier edge sits further below the lip and changes the digging angle, so it is not a free upgrade. The reliable method is to measure the existing edge and lip height, state the material handled and let the supplier confirm the section against a drawing rather than transferring a thickness from another machine.
Can a segmented edge be fitted to a bucket that currently runs a one-piece edge?
It can, provided the lip is sound, the hole pattern and countersink are confirmed, and the segment heights are uniform when assembled. Segmented sets are chosen where safe handling of one long section is difficult or where the lip is no longer flat. The change does alter how the bucket loads, so it is worth recording wear on the first set before standardising the fleet on it.
What are the commercial terms for ordering bucket edges and hardware?
SENTHAI prices every inquiry from the drawings, the quantity and the material specified, so nothing is published as a standing figure. The applicable terms, including quantity break points, packing and delivery arrangements, are stated in the written quotation or order documents. Send the drawings and the machine list first and the technical team will come back with the fitment review and the quotation together.
{
“@context”: “https://schema.org”,
“@type”: “FAQPage”,
“mainEntity”: [
{
“@type”: “Question”,
“name”: “How do I know whether a bolt-on or weld-on bucket edge suits my machine?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Start from service, not price. If the machine must return to work the same day and the lip is sound, a bolt-on edge keeps that option open and the fastener joint is manageable. If the bucket runs long shifts in one abrasive material and the fleet can plan a welding window, a weld-on edge gives a continuous cutting line with no joint to maintain. Mixed fleets usually end up running both.”
}
},
{
“@type”: “Question”,
“name”: “What thickness of loader bucket cutting edge should I order?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Thickness has to be read together with the bucket lip, the machine class and the material. A heavier edge sits further below the lip and changes the digging angle, so it is not a free upgrade. The reliable method is to measure the existing edge and lip height, state the material handled and let the supplier confirm the section against a drawing rather than transferring a thickness from another machine.”
}
},
{
“@type”: “Question”,
“name”: “Can a segmented edge be fitted to a bucket that currently runs a one-piece edge?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “It can, provided the lip is sound, the hole pattern and countersink are confirmed, and the segment heights are uniform when assembled. Segmented sets are chosen where safe handling of one long section is difficult or where the lip is no longer flat. The change does alter how the bucket loads, so it is worth recording wear on the first set before standardising the fleet on it.”
}
},
{
“@type”: “Question”,
“name”: “What are the commercial terms for ordering bucket edges and hardware?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “SENTHAI prices every inquiry from the drawings, the quantity and the material specified, so nothing is published as a standing figure. The applicable terms, including quantity break points, packing and delivery arrangements, are stated in the written quotation or order documents. Send the drawings and the machine list first and the technical team will come back with the fitment review and the quotation together.”
}
}
]
}

