
A Wear Parts Programme for Road Construction Contractors
Road construction wear parts are usually bought project by project, which is why they cost more than they should. Each project brings its own specification, its own supplier and its own lead time, and…

Road construction wear parts are usually bought project by project, which is why they cost more than they should. Each project brings its own specification, its own supplier and its own lead time, and the parts that arrive are judged only when they fail. A programme replaces that sequence with a documented set of products, agreed commercial terms and a consumption record, and it is the difference between a consumable budget that is planned and one that is discovered.
What a Contractor Actually Controls
A contractor cannot control the material it is asked to work, the weather that compresses the season or the specification an agency issues. It can control five things, and together they determine whether wear parts are a managed cost or an unmanaged one.
The first is the duty definition: what each machine actually does, on what surface, at what production rate. The second is the product specification: grade, section, geometry and fitment held constant across orders. The third is the fitment record, which converts a measurement exercise into a repeatable order. The fourth is the commercial structure: quantity tiers, lead times and delivery arrangements agreed in advance. The fifth is the failure record, which is what makes a quality claim resolvable and a specification improvable.
Those five are within reach of any contractor of moderate size, and they are the reason a programme is worth building. Fleets that manage them can compare products objectively; fleets that do not are comparing suppliers on price and parts on appearance.
Standardising Across Machine Types
Standardisation is not the same as forcing one product onto every machine. It means reducing the number of distinct specifications to the smallest set that covers the fleet’s actual duty range, and holding those specifications constant.
A workable approach starts with a duty map. List the machines, and against each one record the surfaces worked, the production rate expected and the wear parts consumed. That map usually shows a small number of duty bands: light surface work, general road construction and maintenance, and abrasive or high-impact work. Each band takes one specification per product category, and the difference between bands is meaningful — grade, section or profile — rather than cosmetic.
Two benefits follow. Buying consolidates into fewer, larger orders with better commercial terms. And maintenance becomes predictable, because a machine’s consumable is determined by its duty band rather than by whatever was on the shelf. Where a fleet runs equipment from several manufacturers, standardisation also means deliberately choosing patterns that fit the largest share of those machines and accepting a conversion cost on the remainder, or holding two patterns and managing them separately. Both work; drifting without a decision does not.
The Documentation Set for Each Product Line
A programme needs documentation, and the set is the same regardless of the product: a specification sheet, a fitment drawing or pattern record, an inspection and traceability arrangement, and a commercial annex holding the agreed terms.
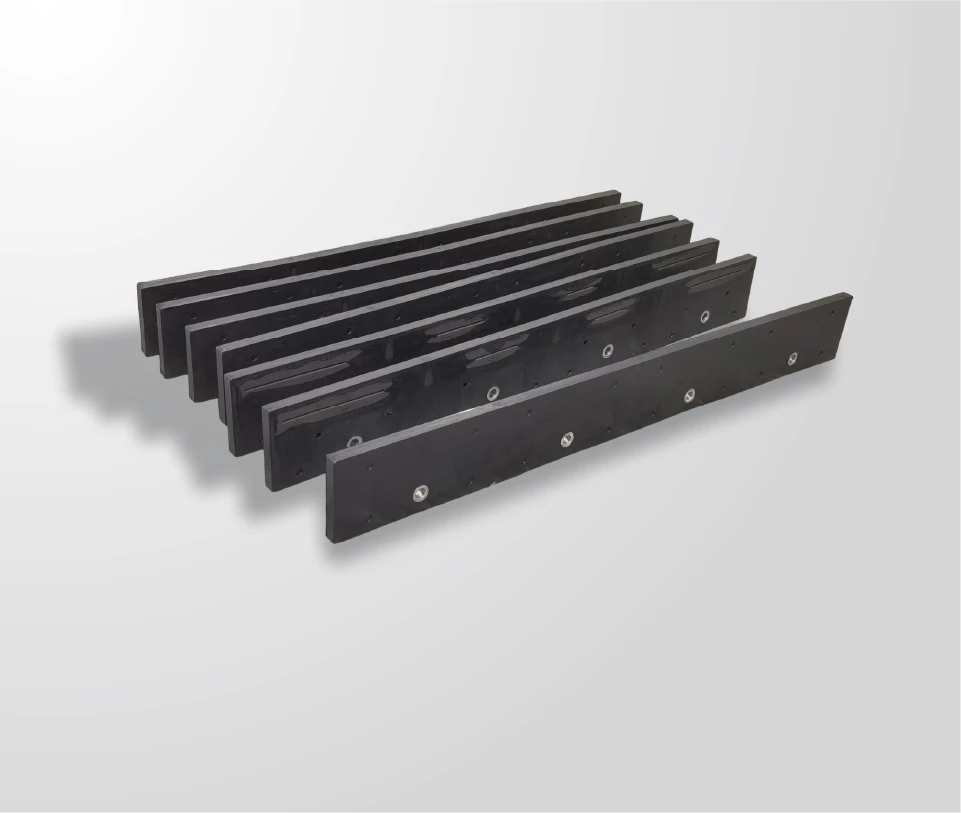
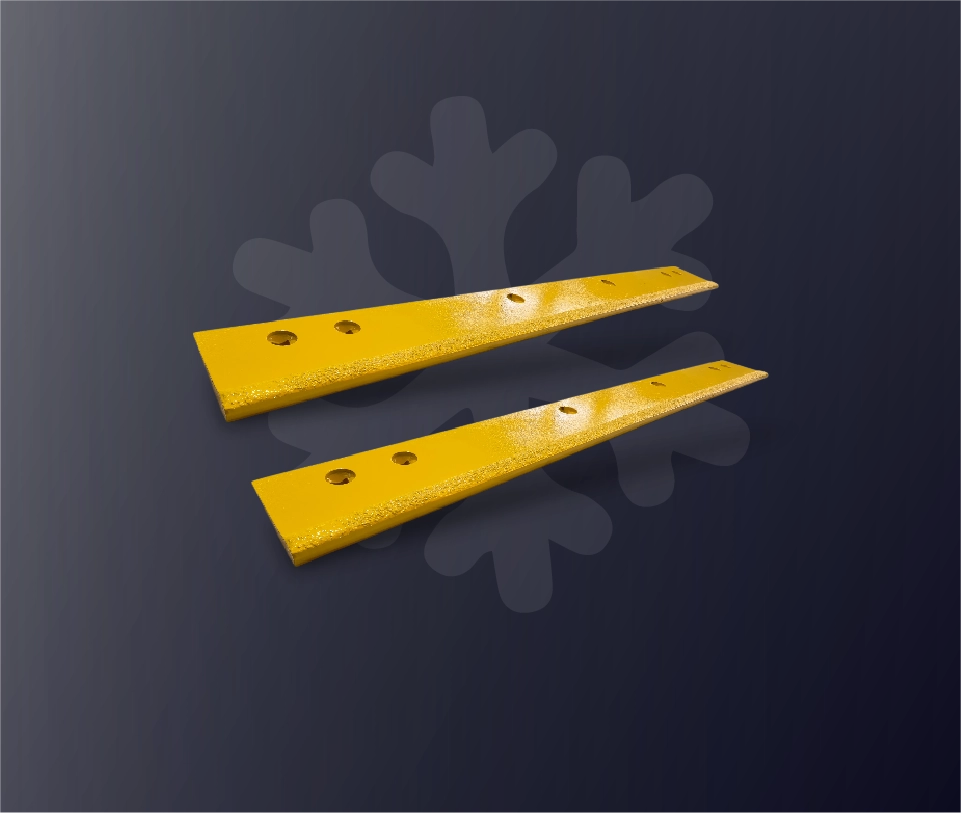
The specification sheet should name the attributes that decide performance rather than the attributes that are easy to list. For an edge, that is section, grade or hardness, profile, pattern and tolerance. For an insert, it is grade, grain size, profile and dimensions. For an assembly, it is the retention system and the interface dimensions. A specification that lists only length and quantity cannot support a comparison between suppliers.
Traceability deserves its own line in the documentation set because it is what makes a programme enforceable. SENTHAI operates lot-level traceability with every batch inspected and archived, so a failure can be tied to a production batch and investigated rather than negotiated. Where a contractor is working to an agency specification, the documentation the agency expects will typically reference published standards — the AASHTO publications programme, ASTM material and test standards, and the road programme guidance published by FHWA — and the contractor’s specification sheet should be written so it can be mapped onto those requirements without translation.
Price Structures and How They Are Built
Wear parts are quoted against a specification and a volume, and the structure of the quote determines what happens on the next order. Three elements are worth understanding because they explain why two similar quotations can behave very differently across a season.
The first is the quantity tier. Unit pricing varies with order size, and a tier structure that matches the fleet’s real annual consumption is worth negotiating explicitly rather than accepting as offered. The second is what happens to pricing on repeat orders: a price held for a season removes recurring negotiation, while a price that is re-quoted each time exposes the contractor to market movement on items that are consumed continuously. The third is what the price includes — delivery to site or to a yard, packaging to the contractor’s requirement, and documentation.
Because manufacturers publish neither prices nor a universal minimum order quantity, both must be obtained in writing for the specific specification and volume required. The same applies to warranty terms, which are set out in the order documents rather than by a general policy. Where the contractor buys through a distributor, the structure may include stocking arrangements, and those terms are negotiated with the distributor. Where a programme is intended to scale, export and delivery terms become relevant too: the Incoterms that govern delivery, risk and cost are published by the ICC, and using them precisely is what prevents a delivery dispute. Equipment-side conventions for the machines these parts fit are published by the AEM, and programme-level research on road maintenance practice is held by the Transportation Research Board.

Continuity, Lead Time and Site Delivery
Continuity is where a programme earns its keep. A consumable that is out of stock stops production, and the loss is not the price of the part but the cost of the idle plant and crew.
Managing continuity requires three decisions. Set a minimum holding based on measured consumption and lead time rather than on a rule of thumb. Agree lead times for repeat orders in advance and in writing, with a clear statement of what triggers a change. And decide where stock is held: at a yard, on site, or with the supplier as a stocking arrangement. Each has a cost, and the correct choice depends on how quickly a machine can be brought back into service when a consumable runs out.
Site delivery introduces its own requirements. Deliveries need to match the site’s access, unloading capability and storage, and packaging needs to protect the parts in the conditions they will be stored in. Where several machine groups are working in different locations, splitting deliveries by group rather than shipping a consolidated consignment prevents the classic error of a part arriving at the wrong site at the right time.
Acceptance and Rejection Criteria
A programme needs acceptance criteria that a storeman can apply without engineering judgement, because that is how a defect is caught before it reaches a machine.
| Product | Acceptance check | Why it matters |
|---|---|---|
| Cutting edges | Pattern, section, profile, tolerance against the drawing | A pattern error makes the edge unusable and the cost unrecoverable in season |
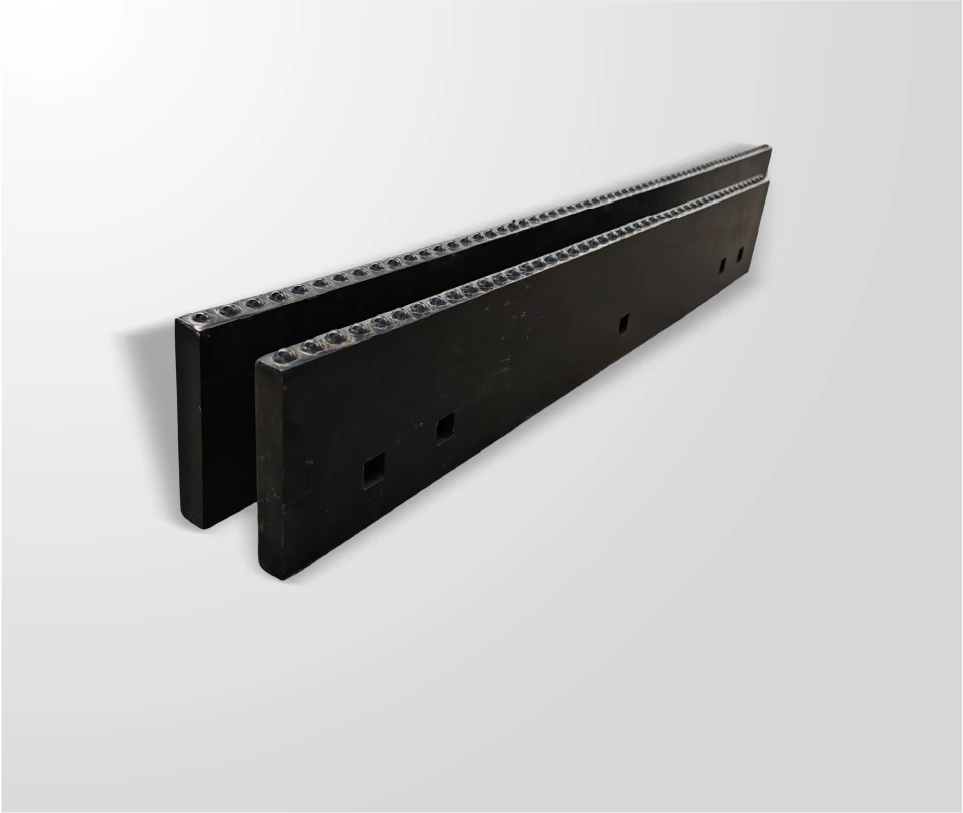
| Carbide-tipped edges | Insert condition, spacing and seating at the braze line | Poor seating becomes insert loss in service |
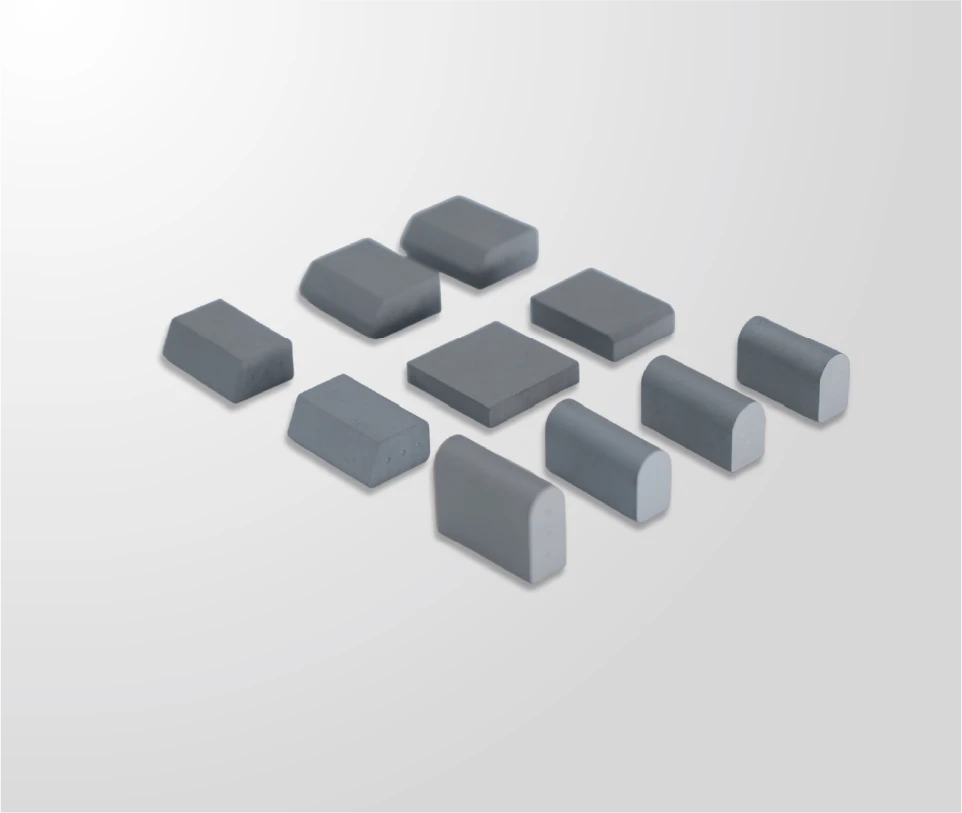
| Inserts and tips | Grade identification, dimensions, absence of cracks or voids | A wrong grade wears fast and produces a false conclusion about the supplier |
| Assemblies and kits | Component completeness against the kit specification | A missing component stops an installation mid-job |
| Any batch | Batch identification and documentation present | Without it, a failure cannot be attributed or claimed |
Rejection criteria should be equally explicit. The general rule is that a delivery failing a dimensional or pattern check is rejected rather than corrected on site, because field modifications remove the traceability that makes the programme work.
Managing Warranty and Failure Claims
Claims are resolved by evidence, and a programme is what produces it. The evidence set is consistent regardless of the product: the batch identification, the specification the part was bought against, the application and duty, the hours or production achieved, the failure mode with photographs, and the measurement or inspection record.
That set allows a supplier to diagnose rather than negotiate. An insert that has shed from a clean pocket is a joint question; an insert that has chipped is a duty or grade question; a pattern that does not fit is a drawing question. Each has a different resolution path, and separating them is what keeps a claim technical instead of commercial.
Where a claim does recur, the useful response is to review the specification rather than to renegotiate the price. A specification that produces repeat failures is describing the wrong product for the duty, and the fix belongs in the duty map and the specification sheet. Product-level performance on this basis is the reason documented quality control and traceability are part of the manufacturer’s offer rather than an optional service — the position is set out on the quality control page, and distributor-facing terms for stocking and private-label programmes are described in the wholesale programme.
A wear parts programme is five controls: a duty map, a small set of held specifications, fitment records, commercial terms agreed in writing, and an evidence-based failure record. Together they turn consumables from a project-by-project expense into a managed line item with a measurable cost per unit of production. Contractors who build that structure early spend less time sourcing parts mid-season and more time comparing products that actually suit the work, which is where the real saving sits.
Send SENTHAI your fleet list, the surfaces worked and current consumption, and the technical team will propose a specification set by duty band with the documentation, lead times and acceptance criteria to go with it.
Frequently Asked Questions
How many different wear part specifications should a contractor hold?
Fewer than most fleets carry. Map the machines to duty bands — light surface work, general road work and abrasive or high-impact work — and hold one specification per product category per band. Every additional specification multiplies ordering complexity and inventory without improving performance, unless it corresponds to a genuinely different duty.
What should be in a wear parts specification sheet?
The attributes that decide performance: section or thickness, grade or hardness, profile or geometry, fitment pattern with tolerance, and the retention system where relevant. Length and quantity belong on the order as well, but they do not distinguish one supplier’s product from another. A sheet that omits grade and tolerance cannot support an objective comparison.
How do I compare wear part suppliers objectively?
Compare against the same specification and require the same evidence from each: grade data, pattern tolerance, inspection arrangements and batch traceability. Then compare cost per unit of production rather than unit price, using your own consumption records. Where a supplier cannot provide the specification detail or the traceability, the comparison is not like for like regardless of price.
What evidence is needed to support a wear parts claim?
Batch identification, the specification the part was bought against, the application and duty conditions, the hours or production achieved, photographs of the failure mode, and any measurement records. With that set a supplier can diagnose a joint, grade or fitment problem rather than negotiate. Without it, a claim becomes an argument about durability that neither side can settle.
{
“@context”: “https://schema.org”,
“@type”: “FAQPage”,
“mainEntity”: [
{
“@type”: “Question”,
“name”: “How many different wear part specifications should a contractor hold?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Fewer than most fleets carry. Map the machines to duty bands — light surface work, general road work and abrasive or high-impact work — and hold one specification per product category per band. Every additional specification multiplies ordering complexity and inventory without improving performance, unless it corresponds to a genuinely different duty.”
}
},
{
“@type”: “Question”,
“name”: “What should be in a wear parts specification sheet?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “The attributes that decide performance: section or thickness, grade or hardness, profile or geometry, fitment pattern with tolerance, and the retention system where relevant. Length and quantity belong on the order as well, but they do not distinguish one supplier’s product from another. A sheet that omits grade and tolerance cannot support an objective comparison.”
}
},
{
“@type”: “Question”,
“name”: “How do I compare wear part suppliers objectively?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Compare against the same specification and require the same evidence from each: grade data, pattern tolerance, inspection arrangements and batch traceability. Then compare cost per unit of production rather than unit price, using your own consumption records. Where a supplier cannot provide the specification detail or the traceability, the comparison is not like for like regardless of price.”
}
},
{
“@type”: “Question”,
“name”: “What evidence is needed to support a wear parts claim?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Batch identification, the specification the part was bought against, the application and duty conditions, the hours or production achieved, photographs of the failure mode, and any measurement records. With that set a supplier can diagnose a joint, grade or fitment problem rather than negotiate. Without it, a claim becomes an argument about durability that neither side can settle.”
}
}
]
}
Related articles
 Asphalt Milling Teeth: Grade, Holder and Cost Per TonneGrader blades and road grading cutting edgesGrader Blade Thickness, Hole Pattern and Bolt GradesGrader blades and road grading cutting edges
 Carbide Grader Blades for High-Abrasion Road SurfacesGrader blades and road grading cutting edges
 Grader Blade Versus Cutting Edge: What Your Machine Actually NeedsGrader blades and road grading cutting edges