
Scraper Blade Cutting Edges: Bowl, Elevator and Router Bits
A scraper blade cutting edge is the part of a motor scraper that decides how much of each bowl load is paid for in metal. The bowl lip peels and lifts material that the…

A scraper blade cutting edge is the part of a motor scraper that decides how much of each bowl load is paid for in metal. The bowl lip peels and lifts material that the elevator or a pusher then drives into the bowl, so every hour in gravel, shot rock or compacted clay is an hour of abrasion on the edge, its fasteners and the bowl lip behind it. Ordering bowl edges, elevator edges and router bits as one generic item, or specifying from a model year rather than from a measurement, is what produces an edge that is correct on paper and unusable on the machine.
How a Scraper Loads and Why That Matters
A scraper loads through its edge, so the edge sets output.
A scraper cuts its own load through the bowl lip; the elevator or push tractor only moves what the edge has loosened, so edge condition sets cycle time before it sets part cost.
Both loading methods load the same parts. A self-loading scraper drives its own bowl lip through the cut, trading engine power for penetration; a push-loaded scraper takes assistance from a crawler tractor at the rear. Either way the cutting edge, the bowl lip and the side cutters carry the cutting load, so they decide whether the bowl fills in a reasonable distance or the pass is spent spinning.
The load path also explains why a scraper edge differs from an edge on a machine that only pushes material. The edge penetrates and then holds depth while the bowl fills, so profile and resistance to dulling matter as much as thickness. A rounded edge does not stop cutting; it stops filling, and the cost appears as extra passes and fuel per cubic metre.
Material state changes the duty more than distance does. Dry sand and loose gravel load easily and wear the edge gently; wet clay loads slowly and works the bowl sides; shot rock introduces impact that bends sections and breaks teeth out. Where scrapers work inside a mine or quarry, practice falls under mine safety rules rather than general industry rules, published in eCFR Title 30 and researched by NIOSH mining.
Bowl Edge Geometry and Material
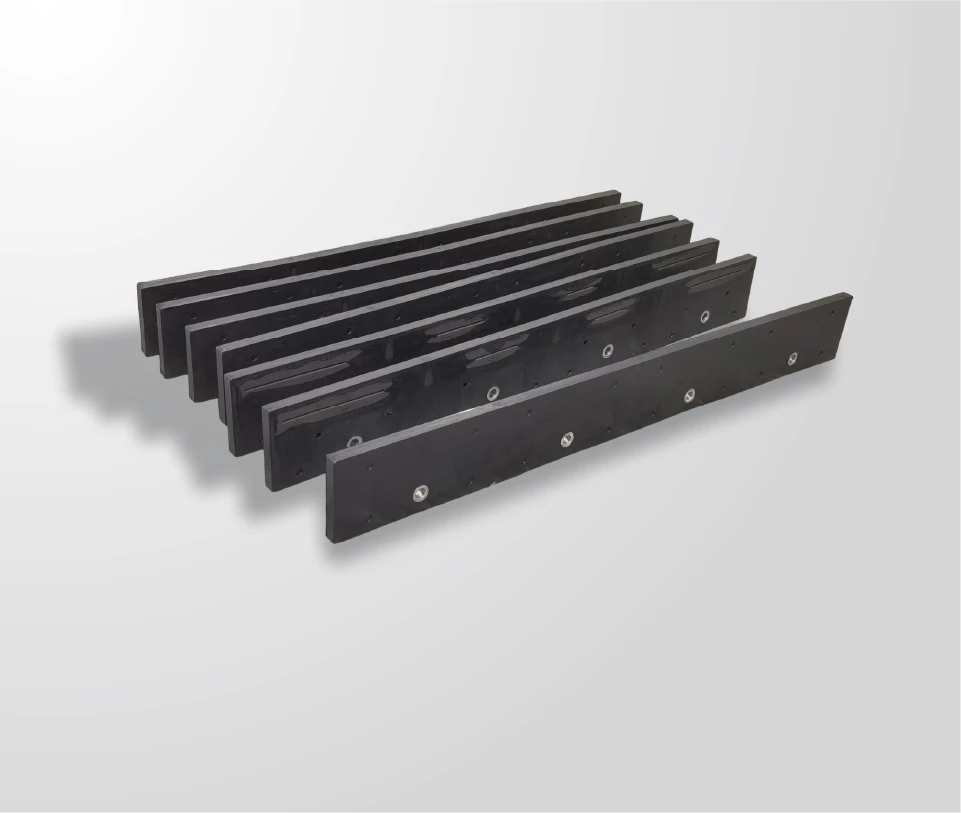
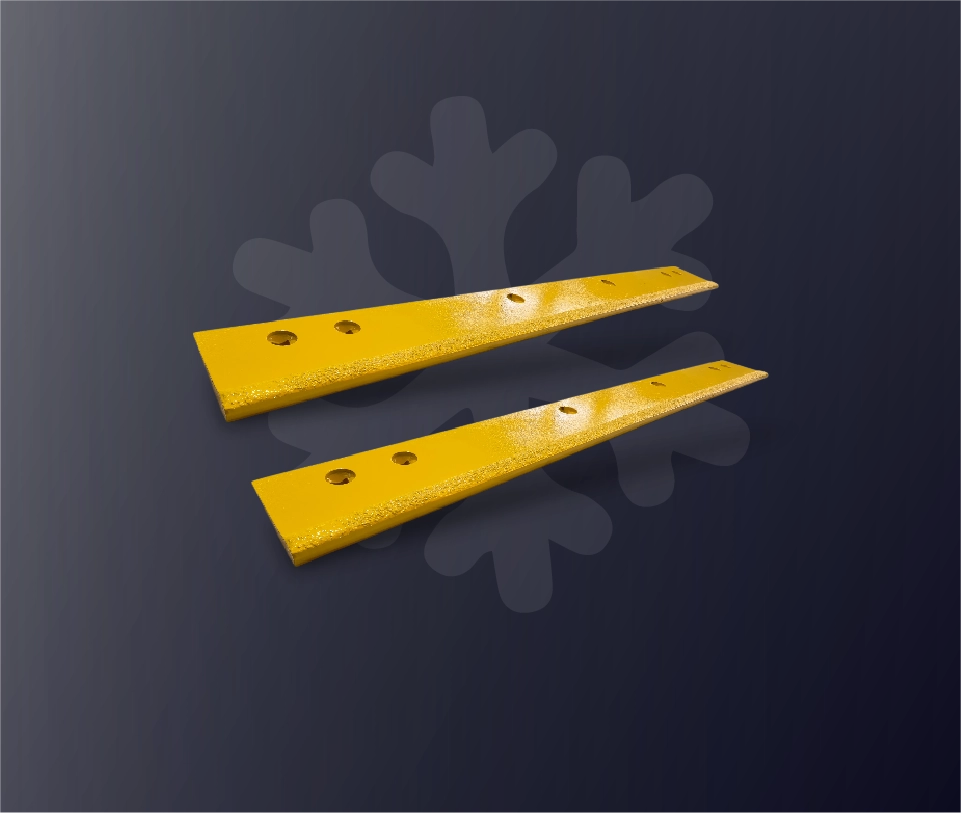
Most scraper bowl and elevator edges are bolt-on sections rather than one continuous blade, and section geometry sets the cutting action. A straight section penetrates predictably; a beveled section throws loosened material further and stalls less readily; a formed section follows the bowl arc. Thickness and hole pattern belong in the same geometry file, because an edge of the right profile and the wrong pattern is scrap.
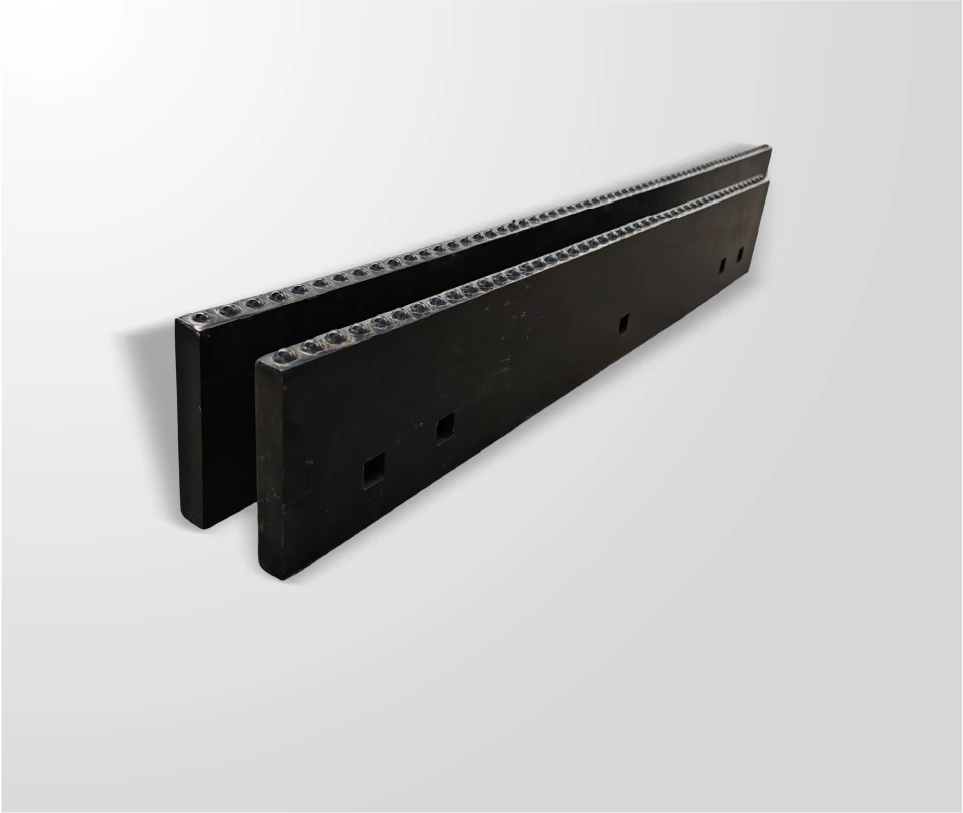
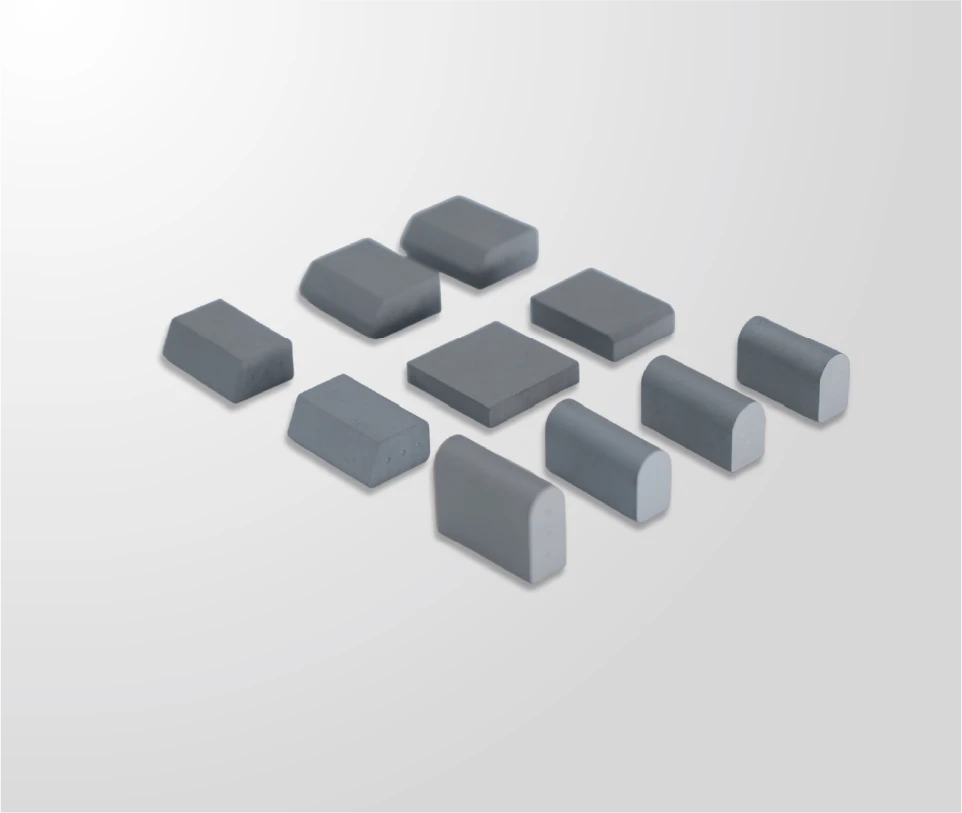
Material follows the duty. A through-hardened and tempered steel edge carries most general earthmoving work. A carbide-tipped edge, with tungsten carbide inserts seated in machined pockets along a steel body, is specified where the material is abrasive enough that edge changes interrupt the job. The assembly logic is covered in the hub article on wear parts beyond plows, and the wear behaviour of the two families is compared separately.
Three numbers travel together: thickness, hardness and profile. Thickness sets how much material exists to be worn away and how much bending load the section survives; hardness, quoted as a band rather than a single figure, sets how fast that material disappears; profile sets whether the edge keeps cutting as it wears. The test standards behind a hardness figure are published by ASTM, and ASM International publishes the wear and metallurgy reference behind abrasion-resistance claims, so a data sheet that names no test method is not yet a specification.
Router Bits, Side Cutters and Stub Teeth
Not every cutting function sits on the bowl lip, and the auxiliary cutters are the parts most often specified loosely. Router bits are replaceable teeth that break up material ahead of the lip so the edge can load it, and they are loaded in bending as well as abrasion. Side cutters are the vertical edges at the bowl sides that cut the walls of the pass. Stub teeth are the short replaceable teeth used where a cut has to be started in hard, compacted or frozen ground.
Because each part has a separate duty, each needs a separate line item. A generic description such as scraper teeth says nothing about the holder, the profile or the load, which is how two supplier quotations end up describing different products.
| Part | Duty | Dominant wear mode | Specify when |
|---|---|---|---|
| Bowl lip edge | Peels the cut across the bowl width | Sliding abrasion, rounding | Always; the primary cutting component |
| Elevator or floor edge | Trims the cut line behind the lip | Abrasion with impact | Elevating scrapers and hard loading |
| Router bits | Loosens material ahead of the lip | Bending and abrasion, tooth loss | Hard or cemented ground |
| Side cutters | Cuts the walls of the pass | Edge wear and face impact | Where the bowl sides run against the cut wall |
| Stub teeth | Initiates the cut in hard material | Tip wear and breakage | Frozen or bonded ground |
Insert and tooth material follows the same rule as the bowl edge. A cemented carbide grade is defined by hardness and toughness together, and grade data for wear parts is published by producers such as Hyperion Materials & Technologies. Where a tooth has to survive impact as well as abrasion, the hardest available grade is not automatically the right one.
Fitment and Tolerance Requirements
Fitment is where a technically correct edge becomes a rejected delivery. Scraper edges are bought against a bowl, a bolt pattern and a section, and the pattern is measured rather than guessed. Machine and attachment interface conventions are published through SAE, and European edge drawings and grade designations are indexed through DIN; mixing the two references on one machine is a common source of a pattern that is close but does not fit.
Five measurements belong on the order:
- Hole diameter and count, recorded per section rather than per machine.
- Hole spacing, centre to centre along the section including the end distances, because spacing error accumulates across a multi-section edge.
- Edge-to-hole distance, which sets both fitment and usable wear life.
- Section and profile: thickness, width and cutting profile, plus any bevel or curve required.
- Countersink angle, matched to the fastener so the head seats flush.
Where no drawing exists, measure the machine or send a worn edge as a physical reference. SENTHAI validates bolt patterns against the drawing or a physical sample before production, and holds machined insert pockets on carbide-tipped edges to a dimensional tolerance of plus or minus 0.02 mm, because that tolerance is what allows fitting without hand work. The same measurement discipline is described in the guide to specifying an edge by measurement.

Quality Evidence to Request With the Quote
An edge specification is only as strong as the evidence offered with it, and the request is short enough to put in writing before an order is placed. Ask for the grade and hardness basis on a steel edge, or the grade, grain size and hardness on a carbide-tipped edge, together with the inspection arrangement for the batch, the dimensional report for the pattern, and the joining method where an assembly is involved.
Traceability is the second half of that request. Lot-level identification, with every batch inspected and archived, is what allows a failure in service to be investigated against a production record rather than argued commercially, and a claim that an edge wore out early cannot be resolved without it.
The third element is a physical reference. Where the specification is new, or a machine group is converting to a harder edge, a first-article or sample submission before volume production removes most of the risk from the order. Sampling arrangements, documentation formats and their cost are not published as standard terms; they are stated in the written quotation or order documents for the specification and quantity required.
Failure Modes Specific to Scrapers
A scraper edge rarely fails in one obvious way, which is why failures are reported as the edge being gone and the underlying cause is never captured. Four modes cover most of what a fleet will see, and each points to a different fix.
| What is seen | Likely cause | Useful response |
|---|---|---|
| Edge rounds off and stops filling the bowl | Hardness class below the ground condition | Move up in grade or section before changing technique |
| Holes elongate and fasteners drop | Pattern or countersink mismatch, or re-used fasteners | Re-measure the pattern; replace fasteners with the edge |
| Section bends between holes or at the ends | Impact on too light a section, or rock under the lip | Increase section or add end protection |
| Insert or tooth loss on tips and router bits | Grade chosen for hardness where toughness was needed | Review grade selection and seating evidence |
The bowl structure is the expensive column. An edge left on the machine until it no longer cuts transfers its work to the bowl lip, the side cutters and the bowl floor, and repairing structure costs multiples of the part that was run too long. On carbide-tipped edges the first symptom is usually insert loss rather than edge rounding, which points at grade selection or seating.
Cost Per Cubic Metre Moved
Unit price is the least useful number in scraper edge procurement because it excludes what the purchase actually costs: the labour to change the edge, the production lost while the machine stands, and the fuel and cycle-time penalty of cutting with a dull profile. Cost per cubic metre moved is the comparison that survives those effects, and it is built from numbers a fleet already records.
The model is edges consumed per thousand cubic metres, multiplied by delivered price plus change-out cost, plus the production penalty of the periods when the edge was worn. A softer section that costs less and is changed three times in an interval where a hardened section is changed once also pays labour, fasteners and downtime three times. Change-out cost is not constant, because a fleet changing edges in its own workshop has a far lower marginal cost than a contractor paying call-out rates at a remote site.
The production penalty is material-specific: a dull edge in loose sand costs little, while the same edge in hard clay costs a great deal. Aggregate and quarry operators have a further reference in industry bodies such as the National Stone, Sand & Gravel Association, whose material-handling context is close to the duty scrapers face. The record is worth more than the model, because fleets that log edge type, material, hours and cubic metres between changes compare carbide-tipped and through-hardened edges on their own numbers rather than on a supplier claim.
Scraper edge specification comes down to four decisions this article has worked through: what the ground does to the edge, which sections and auxiliary cutters are genuinely separate parts, what the pattern must be measured to, and what evidence supports the grade being quoted. Ground condition and change-out cost decide the material; the drawing decides whether the edge can be used at all; and the evidence set decides whether a failure can be resolved technically rather than commercially.
Send SENTHAI the bowl and elevator edge drawings, the bolt patterns and the materials your scrapers work in, and the technical team will review section, grade, cutter specification and fitment tolerances for each machine group.
Related reading: the hub article on wear parts for earthmoving and road maintenance equipment shows how these product lines fit together.
Frequently Asked Questions
What is a scraper blade cutting edge made from?
Most scraper bowl and elevator edges are a formed, through-hardened and tempered steel section, bolted to the bowl lip with plow bolts. Where the ground is abrasive, a carbide-tipped edge is used instead, with tungsten carbide inserts seated in machined pockets along a steel body. Both are supplied to a documented grade with a hardness band, and the grade should be quoted together with the test method behind it rather than as a single figure.
How do I order a scraper bowl edge without a part number?
Measure the machine. Record hole diameter and count, centre-to-centre spacing including the end distances, the edge-to-hole distance, section thickness and profile, and the countersink angle. A worn edge sent as a physical sample works as an alternative reference. The pattern is then validated against that drawing or sample before production, which is what prevents a delivery that is close but does not fit.
Do router bits and bowl edges wear at the same rate?
No, and they should be specified separately. The bowl edge is loaded mostly in sliding abrasion as it peels the cut, while router bits are loaded in bending as well as abrasion because they break up ground ahead of the lip, so they tend to lose teeth rather than round off. Side cutters and stub teeth each have their own duty, so a single generic tooth line item cannot be quoted accurately.
Can a carbide-tipped scraper edge be repaired in the field?
Losing an insert or tooth in service is not a field repair on a scraper edge, because the replacement has to be seated and joined to the same tolerance as the original while the surrounding pockets are usually already worn. The practical route is to run the edge to a measured limit, replace it, and then review whether the grade or the section was wrong for the duty rather than attempting to rebuild it on site.
What are the minimum order quantity and lead time for scraper edges?
Neither is published as a universal figure, because both depend on the specification: section, grade, pattern, whether the edge is plain steel or carbide-tipped, and the quantity required. The applicable minimum order quantity, lead time, packing and delivery terms for a given requirement are stated in the written quotation or order documents issued against that specification.
{
“@context”: “https://schema.org”,
“@type”: “FAQPage”,
“mainEntity”: [
{
“@type”: “Question”,
“name”: “What is a scraper blade cutting edge made from?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Most scraper bowl and elevator edges are a formed, through-hardened and tempered steel section, bolted to the bowl lip with plow bolts. Where the ground is abrasive, a carbide-tipped edge is used instead, with tungsten carbide inserts seated in machined pockets along a steel body. Both are supplied to a documented grade with a hardness band, and the grade should be quoted together with the test method behind it rather than as a single figure.”
}
},
{
“@type”: “Question”,
“name”: “How do I order a scraper bowl edge without a part number?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Measure the machine. Record hole diameter and count, centre-to-centre spacing including the end distances, the edge-to-hole distance, section thickness and profile, and the countersink angle. A worn edge sent as a physical sample works as an alternative reference. The pattern is then validated against that drawing or sample before production, which is what prevents a delivery that is close but does not fit.”
}
},
{
“@type”: “Question”,
“name”: “Do router bits and bowl edges wear at the same rate?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “No, and they should be specified separately. The bowl edge is loaded mostly in sliding abrasion as it peels the cut, while router bits are loaded in bending as well as abrasion because they break up ground ahead of the lip, so they tend to lose teeth rather than round off. Side cutters and stub teeth each have their own duty, so a single generic tooth line item cannot be quoted accurately.”
}
},
{
“@type”: “Question”,
“name”: “Can a carbide-tipped scraper edge be repaired in the field?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Losing an insert or tooth in service is not a field repair on a scraper edge, because the replacement has to be seated and joined to the same tolerance as the original while the surrounding pockets are usually already worn. The practical route is to run the edge to a measured limit, replace it, and then review whether the grade or the section was wrong for the duty rather than attempting to rebuild it on site.”
}
},
{
“@type”: “Question”,
“name”: “What are the minimum order quantity and lead time for scraper edges?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Neither is published as a universal figure, because both depend on the specification: section, grade, pattern, whether the edge is plain steel or carbide-tipped, and the quantity required. The applicable minimum order quantity, lead time, packing and delivery terms for a given requirement are stated in the written quotation or order documents issued against that specification.”
}
}
]
}
Related articles
 Bucket Edge Wear Protection: Liners, Heel Plates and ShroudsLoader bucket edges, teeth and wear linersBolt-On Versus Weld-On Bucket Teeth: Change-Out EconomicsLoader bucket edges, teeth and wear liners
 Loader Bucket Cutting Edge Types: Bolt-On, Weld-On and SegmentedLoader bucket edges, teeth and wear liners
 A Wear Parts Programme for Road Construction ContractorsGrader blades and road grading cutting edges