




Crusher Wear Parts Supplier Evaluation: The Documentation Set
Two crusher wear parts suppliers can quote the same liner, the same profile and a similar price, and still leave a procurement officer with no way to tell which delivery will fit. What separates…

Two crusher wear parts suppliers can quote the same liner, the same profile and a similar price, and still leave a procurement officer with no way to tell which delivery will fit. What separates them is not the catalogue photograph but the documentation behind it: the drawing that fixes the interface, the grade data that defines the material, and the inspection record that shows what was actually checked. Evaluating a crusher wear parts supplier is therefore a paperwork exercise as much as a technical one, and it is worth running in a fixed order.
This page is for buyers who have to award, defend and live with the decision: plant and maintenance managers at aggregate and mining operations, contractors buying aftermarket parts, distributors adding a line, and OEMs placing a production order. It covers what the buyer actually controls, how to write a specification instead of naming a brand, which documents to demand before award, how pricing is built, how lead time and continuity are handled, where acceptance testing belongs, and how a wear-part dispute is resolved.
What the Buyer Actually Controls
Buyers control specification, documentation and acceptance.
A buyer cannot audit a supplier’s every internal step, but can define the specification, demand the records and set the acceptance gate that a delivery has to pass.
There is a natural instinct in wear-part procurement to try to control the supplier rather than the deliverable, by requesting factory photographs, process descriptions and assurances. Those are useful for context and less useful as controls, because none of them is checkable on the dock. What is checkable is the drawing revision, the grade stated with its hardness and grain size, the dimensional report and the inspection record for the batch in the crate.
Control therefore narrows to three levers. The first is the specification: a drawing or a physical sample that fixes the interface, and a material definition that states properties rather than a trade name. The second is the record: what the supplier measures, holds and can retrieve months later, since a plant that discovers a fitment problem in month eight needs information from month one. The third is acceptance: the points checked on receipt, by whom, against what, and what happens when one fails.
Everything else in this article follows from those three levers. A supplier with a documented process chain, lot-level traceability and a habit of archiving inspection results is easier to hold to a specification than one whose quality rests on assurances, but the buyer’s real protection is the specification and the acceptance gate, not the assurance.
Specification Versus Brand
A specification-led purchase describes the part by what it has to do and the interface it has to fit; a brand-led purchase describes it by who made it last time. Both work, and they fail in different ways, so the choice should be made deliberately rather than by default.
Brand-led buying is fast and predictable when the brand supplies the machine or the OEM part number is current, and it is expensive when the part is a commodity casting with a long lead time. Specification-led buying opens the supply base and asks more of the buyer, because someone has to write the drawing, define the material and accept responsibility for the acceptance criteria. The failure mode of a brand-led purchase is cost and dependency; the failure mode of a specification-led purchase is a loose specification that lets a marginal part through.
| Point of comparison | Brand or OEM part number | Specification-led purchase |
|---|---|---|
| Defined by | Manufacturer and part number | Drawing, material data and interface dimensions |
| Supplier base | Usually one route | Open to any maker that meets the specification |
| Buyer effort | Low at award | Higher before award, lower at every repeat |
| Main risk | Price and dependency | A specification too loose to exclude a poor part |
| Repeat order | Re-order the number | Re-order the revision, with the same acceptance points |
Documentation to Demand Before Award
The document set should be agreed before the order is placed, not collected afterwards, because a document that cannot be produced at award usually cannot be produced at delivery either. Ask for it as a package and treat missing items as a qualification issue rather than an administrative one.
- Interface definition. The drawing revision, or a controlled physical sample, that fixes hole pattern, spacing, thickness and profile. Fitment validation against that reference is a stated activity, not an inference from a photograph.
- Material definition. Carbide grade with hardness in HRA and grain size; steel body grade with hardness; the joint method where inserts are attached.
- Dimensional and inspection records. The measurements taken, the tolerance held on machined features such as insert pockets, and who performed the check.
- Batch identification. How the batch in the crate links to the production and inspection records behind it.
- Packing and preservation. How edges and machined faces are protected in transit, and how the batch is labelled.
Measurement discipline is what gives these documents weight. Reference material from NIST on measurement traceability, and the material and test standards published by ASTM, are the background that lets a buyer ask whether a reported figure was produced by a recognised method or by an internal habit.
Pricing Structure and What Drives It
Wear-part pricing is built from inputs rather than set by the part number, and understanding the structure is what allows a buyer to compare quotations that do not look alike.
The dominant inputs are the wear material and its volume, the machining content of the part, the batch quantity, the level of inspection agreed, packing, and the delivery terms. A carbide-tipped item carries the cost of the carbide and the joining step; a large cast or fabricated liner carries the cost of the section and the machining of the mounting pattern. Inspection level is a real cost line: a delivery checked dimensionally and recorded batch by batch is not the same product as one inspected by eye at the end of the line.
Delivery terms are where quotations most often diverge without the price looking different, because the point at which responsibility and cost transfer changes what the buyer actually pays. The international commercial terms that define those points are maintained by the International Chamber of Commerce, and a quotation that names the term is easier to compare than one that does not. Where two prices differ by a few percent and the terms are different, the comparison has not been made yet.
The practical rule is to compare on landed cost for a defined scope, with the inspection level and the documentation package stated in both quotations.
Lead Time, MOQ and Continuity
Continuity matters more than a single delivery in wear-part supply, and it is a question about tooling, patterns and process rather than about promises.
A first order and a repeat order are different events. The first includes setup: pattern or drawing review, insert pocket machining, first-article checks and packing development. Subsequent orders should be a repeat of a known revision, which is why the revision number and the inspection record matter at reorder time — they are what make the second delivery the same as the first. A buyer should ask how a repeat order is identified internally, because the answer shows whether the supplier works from a controlled revision or from memory.
Batch quantity and lead time are commercial variables, agreed per order, quoted against the specific drawing and quantity, and stated in the written quotation or order documents. Where a plant needs buffer stock, the questions worth asking are how long a batch stays identifiable as one production run, and whether a repeat can be scheduled against a known revision.
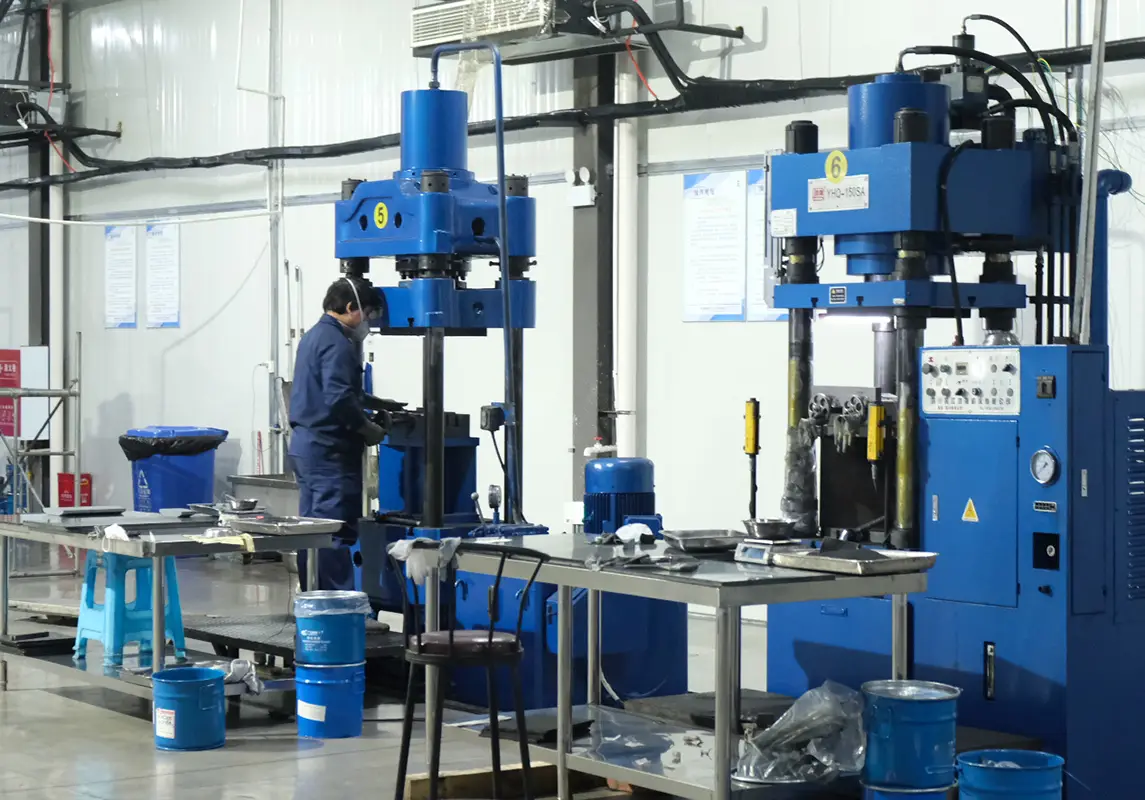
Quality Gates and Acceptance Testing
Acceptance testing turns a specification into a gate, and it should be written so that a delivery either passes or is documented as failing.
The practical gates are dimensional, material and assembly checks. Dimensional checks confirm that hole pattern, thickness and profile match the drawing revision, which is where a fitment problem is caught before a machine is stripped. Material checks confirm the grade and hardness claimed, and can be requested as documentation rather than testing where the supplier holds the records. Assembly checks are specific to carbide-tipped items: that the insert sits correctly in its pocket, that the joint is sound and that the retaining feature works.
What makes a gate work is that the criteria are written in the order before delivery, with the sampling basis and the record that will be kept. Federal procurement practice is a useful reference for how acceptance criteria and documentation requirements are structured in a formal order, and the contracting resources published by GSA and the supplier registration guidance at SAM.gov show the level of detail that holds up when a delivery is disputed. SENTHAI inspects and archives every batch, so acceptance criteria can be checked against records kept with the batch rather than reconstructed after the fact.
Risk, Warranty and Dispute Handling
Wear parts fail in service, and the useful question is not whether a failure will occur but whether the evidence needed to classify it will exist when it does.
A dispute is resolved by separating three outcomes: a part that did not meet the specification, a part that met the specification but was unsuitable for the application, and a part that failed because of how it was fitted or operated. Each has a different answer, and each is decided by evidence gathered in the first hours after the failure rather than by correspondence afterwards. Photographs of the failed item in position, the zone it came from, the hours and tonnage since installation, the condition of the retaining hardware, and the batch identification from the delivery are what make that classification possible.
The commercial terms that govern a claim — how long a claim window remains open, what the supplier will do, and how the part is returned or inspected — are stated in the written quotation or order documents, so they should be read before the first order rather than after the first failure. Procurement review bodies such as the US Government Accountability Office publish findings on how contested awards and claims are examined, which is a reminder that a claim is settled on records rather than on recollection.
For export orders, import and clearance documentation is worth a check before the first shipment; the requirements published by the International Trade Administration cover the practical side of cross-border supply.
The supplier decision described here rests on three things a buyer fully controls. Write the specification so the part is defined by interface and material data rather than by a brand, demand the documentation set before award, and set an acceptance gate with written criteria and a kept record. Pricing then becomes comparable on landed cost with a stated inspection level, continuity becomes a question about revisions and batch identity, and a failure becomes an evidence exercise rather than an argument. A supplier with documented grades and archived batch inspection makes that discipline easier to apply, but the discipline itself is what protects the plant.
Send SENTHAI the drawing or sample that defines the part, the feed conditions it works in and the acceptance points your plant wants checked, and the technical team will prepare the specification, documentation package and batch inspection record for review before award.
Related reading: the wider consumable picture is set out in wear parts beyond plows, and how batches are inspected and archived is described at our quality-control page.
Frequently Asked Questions
What documents should come with a crusher wear parts delivery?
The package should include the drawing revision or controlled sample that defines the interface, the carbide grade with hardness in HRA and grain size, the steel body grade and hardness, the dimensional inspection record, and the batch identification that links the crate to the production records. Packing and preservation instructions belong with it. Agreeing this list before award is what makes it enforceable at delivery, because a document that cannot be produced then usually cannot be produced later.
How do I compare two wear parts suppliers on quality?
Compare them on the specification they will accept, the records they will provide and the acceptance gate they will work to, then on landed cost for a defined scope. Unit price alone cannot carry the comparison, because inspection level, documentation and delivery terms change what the buyer receives. A supplier that can state the grade, the tolerance on machined features and how a batch is identified is offering something a supplier working from a catalogue photograph cannot.
Can a crusher wear part be specified without naming an OEM brand?
Yes, and for a commodity casting or a machined insert set it is usually the better route. The specification is built from the drawing or a controlled physical sample, the interface dimensions, and the material properties required for the duty. That definition can be met by any maker able to hold the tolerance, which opens the supply base while keeping the plant protected. The risk to manage is a specification too loose to exclude a marginal part.
What are the ordering terms, batch quantity and lead time for wear parts?
These are commercial variables rather than fixed published figures. Quantity, lead time, packing, delivery terms and inspection scope are agreed per order against the specific drawing and are stated in the written quotation or order documents. The quotation is the right place to read the claim window and any return or inspection arrangements, and it should be read before the first order rather than after a failure in service.
How is a wear part failure investigated and settled?
By separating three cases: a part that did not meet specification, a part that met specification but was unsuitable for the application, and a part that failed because of fitment or operation. The evidence needed is gathered in the first hours after the failure and includes photographs of the item in position, the zone it came from, hours and tonnage since installation, hardware condition and the batch identification. The claim window and remedy are stated in the written quotation or order documents.
{
“@context”: “https://schema.org”,
“@type”: “FAQPage”,
“mainEntity”: [
{
“@type”: “Question”,
“name”: “What documents should come with a crusher wear parts delivery?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “The package should include the drawing revision or controlled sample that defines the interface, the carbide grade with hardness in HRA and grain size, the steel body grade and hardness, the dimensional inspection record, and the batch identification that links the crate to the production records. Packing and preservation instructions belong with it. Agreeing this list before award is what makes it enforceable at delivery, because a document that cannot be produced then usually cannot be produced later.”
}
},
{
“@type”: “Question”,
“name”: “How do I compare two wear parts suppliers on quality?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Compare them on the specification they will accept, the records they will provide and the acceptance gate they will work to, then on landed cost for a defined scope. Unit price alone cannot carry the comparison, because inspection level, documentation and delivery terms change what the buyer receives. A supplier that can state the grade, the tolerance on machined features and how a batch is identified is offering something a supplier working from a catalogue photograph cannot.”
}
},
{
“@type”: “Question”,
“name”: “Can a crusher wear part be specified without naming an OEM brand?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “Yes, and for a commodity casting or a machined insert set it is usually the better route. The specification is built from the drawing or a controlled physical sample, the interface dimensions, and the material properties required for the duty. That definition can be met by any maker able to hold the tolerance, which opens the supply base while keeping the plant protected. The risk to manage is a specification too loose to exclude a marginal part.”
}
},
{
“@type”: “Question”,
“name”: “What are the ordering terms, batch quantity and lead time for wear parts?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “These are commercial variables rather than fixed published figures. Quantity, lead time, packing, delivery terms and inspection scope are agreed per order against the specific drawing and are stated in the written quotation or order documents. The quotation is the right place to read the claim window and any return or inspection arrangements, and it should be read before the first order rather than after a failure in service.”
}
},
{
“@type”: “Question”,
“name”: “How is a wear part failure investigated and settled?”,
“acceptedAnswer”: {
“@type”: “Answer”,
“text”: “By separating three cases: a part that did not meet specification, a part that met specification but was unsuitable for the application, and a part that failed because of fitment or operation. The evidence needed is gathered in the first hours after the failure and includes photographs of the item in position, the zone it came from, hours and tonnage since installation, hardware condition and the batch identification. The claim window and remedy are stated in the written quotation or order documents.”
}
}
]
}

