
Inserts for Automated Brazing Lines: Robotic Assembly and Fit
An automated brazing line changes the rules for carbide inserts. A human operator can compensate for a slightly oversized insert or a tight slot; a robotic pick-and-place system cannot. When the line is automated,…
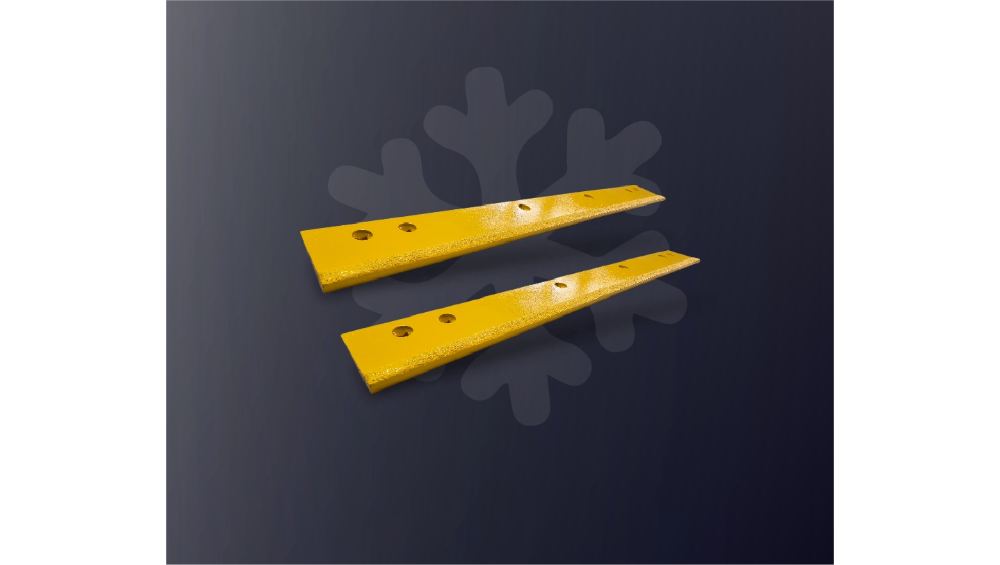
An automated brazing line changes the rules for carbide inserts. A human operator can compensate for a slightly oversized insert or a tight slot; a robotic pick-and-place system cannot. When the line is automated, insert consistency becomes a production input, and a batch of inserts that is “close enough” by hand becomes a line-stopping problem by robot.
This article explains what automated insert assembly demands: how robotic lines handle inserts, the fit requirements that prevent jams, the consistency that keeps the line running, and what a manufacturer should verify with its insert supplier before committing to automation.
Automation raises the consistency bar
The business case for automated brazing is productivity: faster cycles, repeatable joints, and fewer labor hours per blade. The price of that productivity is tolerance. A robot indexes to a programmed position and a brazing cell applies heat on a fixed cycle, so the insert has to arrive where the program expects it, every time.
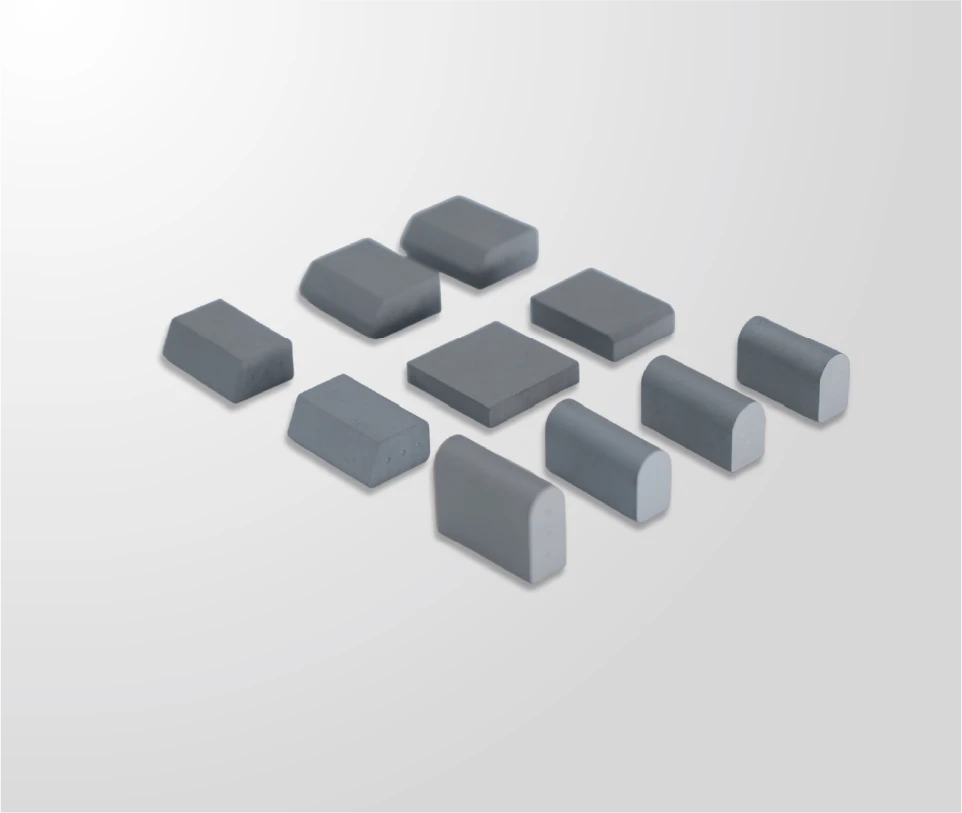
That is why manufacturers moving to automation discover that insert quality is not just a material question. It is a dimensional and consistency question. SENTHAI, which supplies carbide inserts for snow plow blade production, states that it can hold dimensional tolerances within ±0.02 mm and describes this precision as ideal for manufacturers using high-speed robotic pick-and-place or automated induction brazing systems. The statement points directly at the requirement: the insert must fit the milled slot within a tolerance the robot can absorb.
For an OEM, the practical consequence is that insert sourcing and line automation have to be designed together. The insert specification, the slot machining tolerance, and the robot’s pickup tolerance form one system, and changing any one of them changes the others. The same discipline applies to the finished product: the carbide snow plow blade page shows how insert fit feeds into the assembled blade, so the line’s quality targets should be defined at the component level first.
How do robotic lines handle inserts?
A typical automated insert line follows a fixed sequence: inserts are fed from a magazine or tray, picked by a robot or pick-and-place unit, positioned into the milled slot on the steel carrier, and passed to an induction brazing cell where heat and alloy form the joint.
Every step assumes a consistent part. The feeder needs inserts that stack and separate cleanly without burrs. The robot gripper needs a part whose dimensions stay inside the pickup window. The slot insertion needs a fit that is neither too loose, which allows the insert to shift during handling, nor too tight, which jams the cell. The brazing cell needs the insert seated at the same position on every cycle so the joint forms in the same place.
The failure modes are characteristic of automation: jams, mis-seats, and off-position brazing. All three trace back to variation that a human line could absorb and a robotic line cannot.
Fit requirements that prevent jams
Jam prevention starts with the dimensional agreement between the insert and the slot. The two drawings have to be checked together, and the tolerance stack has to fit inside the robot’s handling window.
The practical requirements:
| Requirement | What it prevents |
|---|---|
| Insert dimensions held consistently | Feed and seating variation across the batch |
| Edge condition free of burrs and chips | Feeder and gripper catches |
| Consistent surface preparation | Uneven wetting in the brazing process |
| Slot machining held to the drawing | Fit mismatch at the tolerance extremes |
SENTHAI describes its inserts as manufactured from 100% virgin micro-grain tungsten carbide with controlled compression molding and vacuum sintering, and its stated ±0.02 mm tolerance is the kind of number an automation engineer needs to see in the specification rather than discover during commissioning.
Consistency that keeps the line running
Consistency is the difference between a line that runs and a line that stops. Batch-to-batch variation in insert dimensions, surface condition, or hardness changes how the parts feed, seat, and braze, and the first sign of trouble is often an unexplained jam or a run of weak joints.
The supplier’s process control is what protects the line. SENTHAI states that its quality control monitors the sintering environment and metallurgical properties, including grain size and hardness, to keep physical properties consistent from shipment to shipment. For an OEM, that translates into a supply agreement with defined batch documentation, so the line knows what to expect before the pallet is opened.
Consistency is also a maintenance metric, not just a purchasing one. When the line runs smoothly for weeks and then begins to jam or produce variable joints, the change is usually in the incoming material, not in the robot. A line log that records batch numbers alongside jam counts and brazing results makes that connection visible: the pattern of problems lines up with the batch, and the supplier conversation starts with data instead of impressions. Building that log is a small change to the line’s existing records, and it turns consistency from a vague requirement into a measurable contract.
Expert view — SENTHAI engineering team: “When a line starts jamming, the first question is not the robot, it is the batch. We see inserts that vary by fractions of a millimeter stop automated cells that ran fine on the previous lot. Consistency is the specification that automation cannot work without.”
What should you verify with your supplier?
Before committing inserts to an automated line, verify these items with the supplier:
- Dimensional tolerance and the measuring method used to confirm it;
- Batch consistency records across multiple shipments, not just one lot;
- Surface condition and preparation for brazing;
- Edge quality, including freedom from burrs and chips;
- Documentation that ships with each batch, so the line can trace any issue to a lot.
Run a pilot lot through the actual line before production volumes. Measure feed reliability, jam rate, seat position, and brazing results, and compare them against the acceptance criteria. A pilot lot is the only reliable way to confirm that the specification on paper is the part on the feeder.
Define the acceptance criteria before the pilot starts, not after. A simple scorecard works: a target jam rate per thousand parts, a maximum seat-position deviation, and a brazing quality check at a defined sampling rate. If the pilot lot meets the scorecard, the line has a verified baseline; if it does not, the data identifies whether the fix belongs to the insert supplier, the slot machining, or the robot program. Writing the criteria first keeps the pilot honest and gives procurement a pass-fail standard to hold against future shipments.
Keep your line moving
Automated brazing rewards the manufacturers who treat insert supply as part of the process design. Define the tolerance and documentation requirements before commissioning, verify them with a pilot lot, and keep the batch records attached to every delivery so the line can react to variation instead of guessing.
SENTHAI’s carbide inserts page describes the standard range, tolerances, and process controls relevant to automated assembly. For a specification confirmation and pilot terms, send the slot drawing and line requirements through the contact page and ask for the batch documentation that will support your line.
The same discipline should extend to the finished blade assemblies, not just the inserts: the line’s brazing results, sampling data, and batch numbers belong in the same record system that qualifies the incoming parts. When the whole chain, incoming insert to finished blade, shares one documentation standard, a problem anywhere in the process can be traced to its source instead of becoming a debate between departments.
Frequently Asked Questions
Why does automation change insert requirements? Robotic lines cannot compensate for variation the way human operators can. Inserts must fit the feeder, gripper, and slot consistently, so dimensional tolerance and batch consistency become production inputs.
What tolerance does SENTHAI state for its inserts? SENTHAI states it can hold dimensional tolerances within ±0.02 mm, which the company describes as suitable for robotic pick-and-place and automated induction brazing systems.
What causes jams on an automated insert line? Common causes are insert dimensions outside the handling window, burrs or edge defects, slot machining at the edge of tolerance, and batch-to-batch variation that changes the fit.
How do I validate inserts before production volumes? Run a pilot lot through the actual line and measure feed reliability, jam rate, seat position, and brazing results against defined acceptance criteria.
What documentation should an insert order include? Dimensional inspection results, batch consistency records, material and process documentation, and brazing surface preparation details, confirmed during quotation.
Does SENTHAI support automated assembly programs? SENTHAI describes its inserts and tolerances as suited to automated assembly, and its engineering team can confirm the specification and pilot terms for the line. Confirm details per order.
Can an insert batch vary and still pass a visual check? Yes, which is why automation programs need measured tolerances and batch records rather than visual acceptance. The pilot lot is the verification.
Sources
Related articles
 Best Snow Plow Blade Family for Your Fleet: Top 5 ScenariosKnowledge
 Top 10 Snow Plow Blade Types for Winter Fleets (Ranked by Duty Fit)KnowledgeTop 5 Best Carbide Blade Configurations for Highway PlowingKnowledge
 Best Snow Plow Blade Materials Ranked: Steel vs Carbide vs Cladding vs Rubber-CarbideKnowledge